
UFIBER® Radial Ceramic Fiber Disc Precision Deburring, Grinding & Polishing
Ultra-thin 0.8 mm ceramic-fiber radial abrasive disc for controlled deburring, grinding, edge finishing and polishing. Designed for grooves, ribs, side walls, slots and other narrow or difficult-to-access features.
- 0.8 mm Ultra-Thin
- Radial Cutting Action
- 6 Grit Grades
- CNC / Robot Ready
- E-Pack Compatible
- Electric Drive Only

FINISHING
What is the UFIBER® Radial Ceramic Fiber Disc?
An ultra-thin 0.8 mm ceramic-fiber abrasive disc for precision deburring, grinding, edge finishing and polishing. Its outer circumference provides controlled radial cutting, while the thin profile reaches grooves, ribs, side walls, slots and other narrow or difficult-to-access features.
Five diameters from Ø13 to Ø30 mm, six grits from #150 to #1000. Use it by hand on the UF9999 Portable E-Pack, or integrate it into CNC machines and robotic cells with a compatible electric spindle.
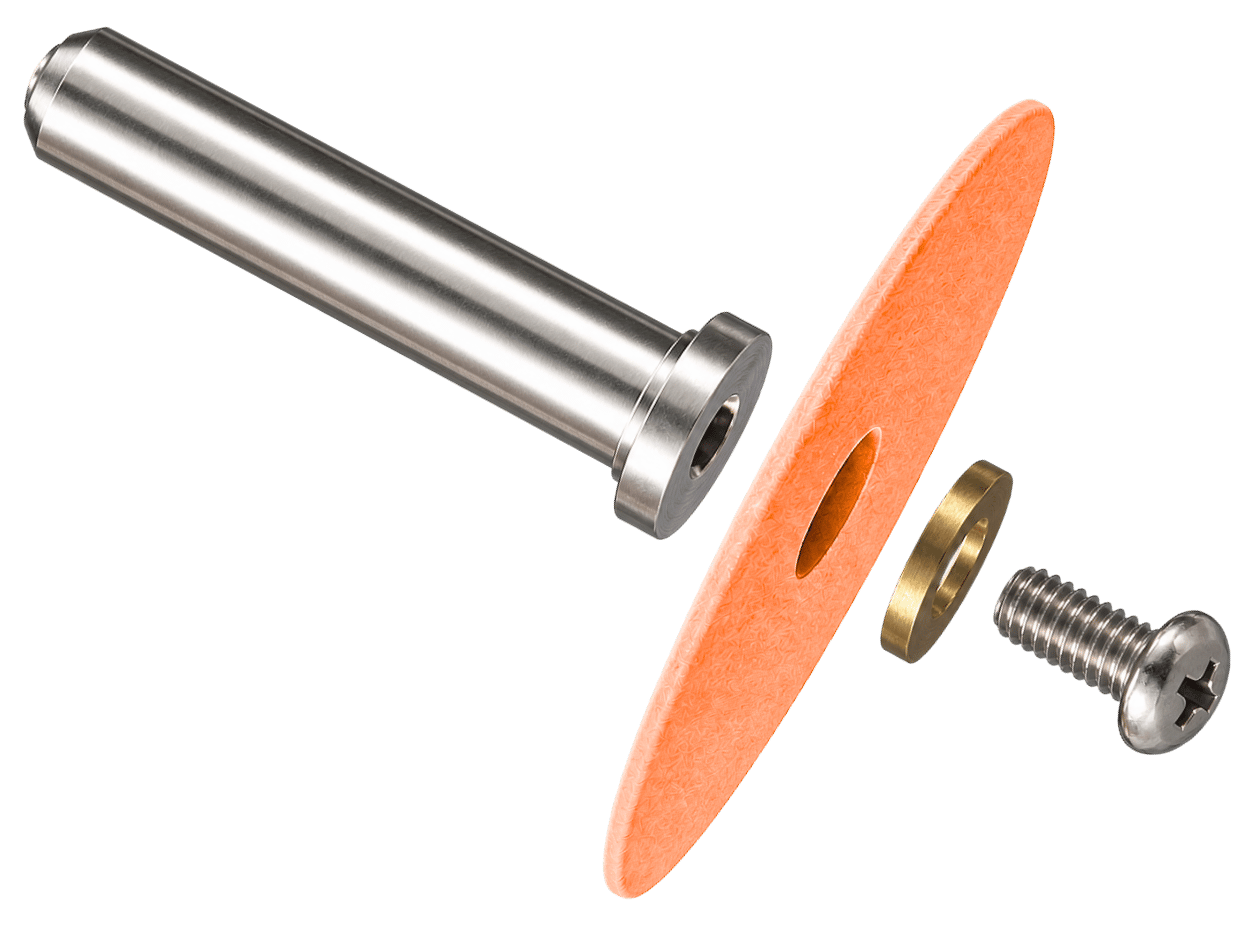
- Radial cutting actionControlled finishing with the outer edge of the disc.
- Ultra-thin 0.8 mmReaches narrow grooves, slots and confined profiles.
- Precision deburringControlled burr removal and edge refinement.
- Grinding & polishingFrom coarse removal to ultra-fine polishing.
- Portable operationRuns on the UFIBER Portable E-Pack UF9999.
- Automation readyCNC machines and robotic arms with an electric spindle.
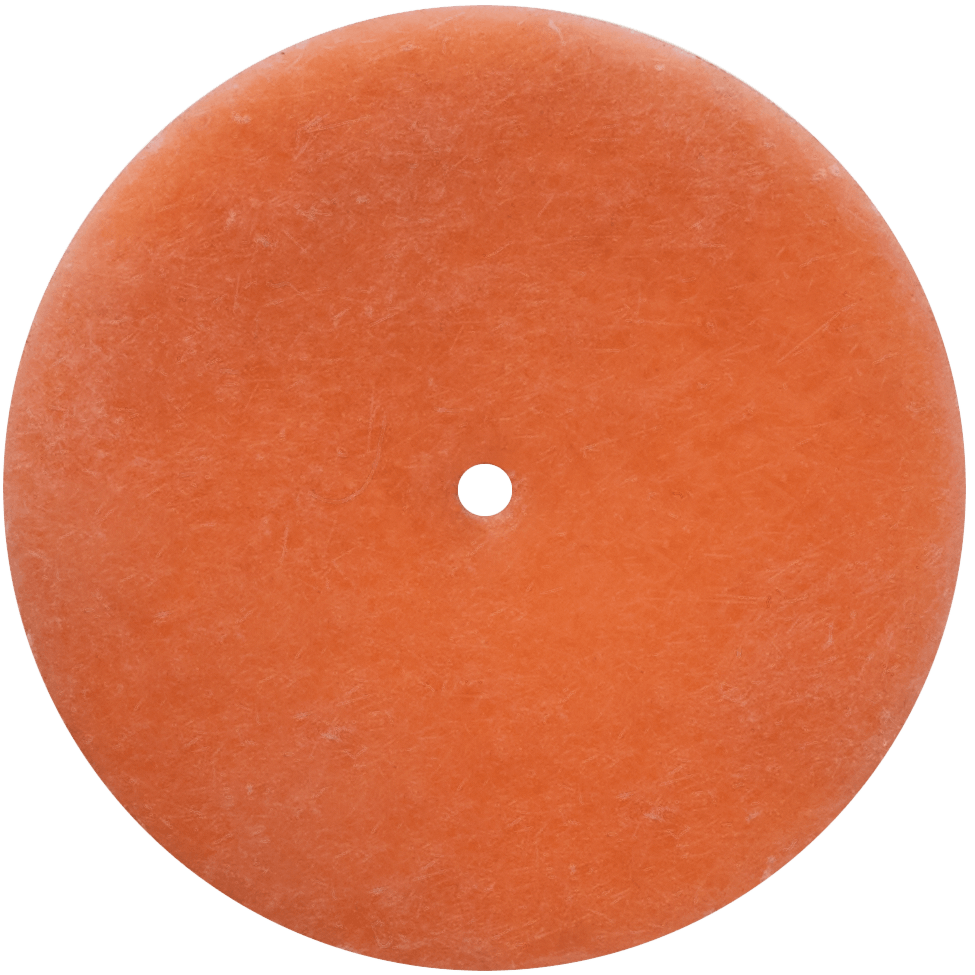
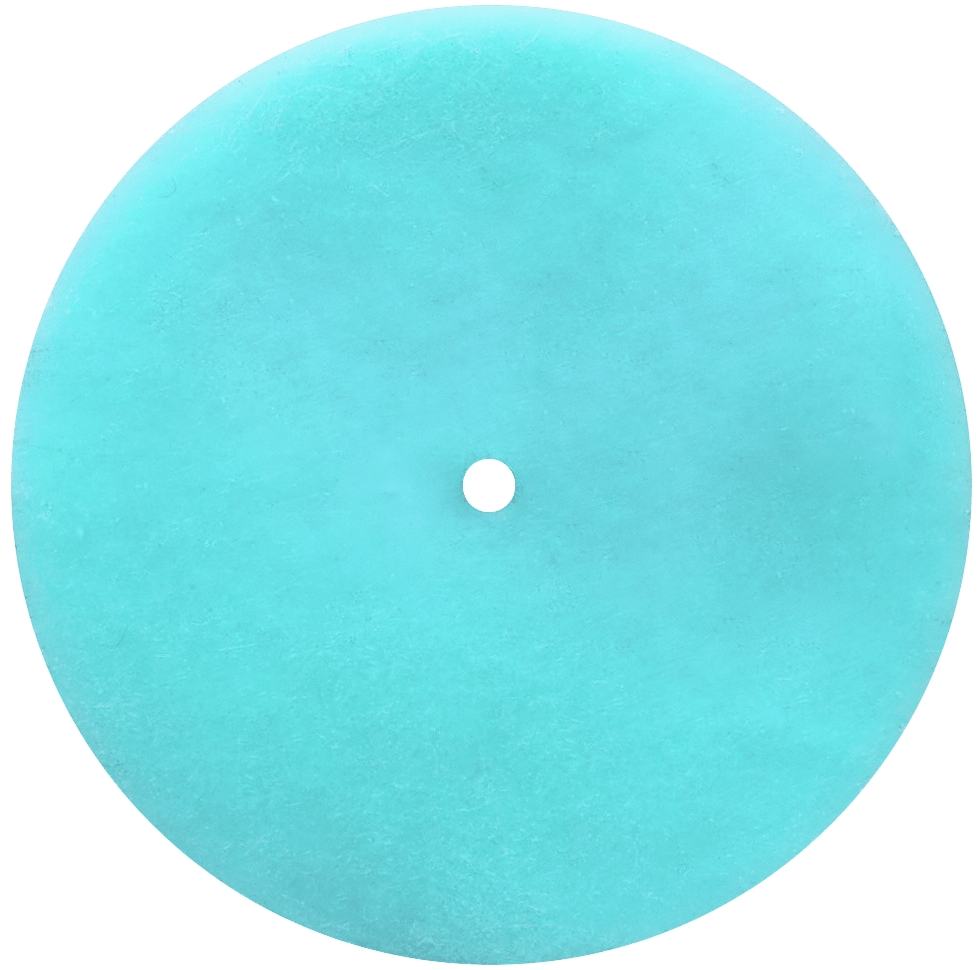
Grit & Color Guide
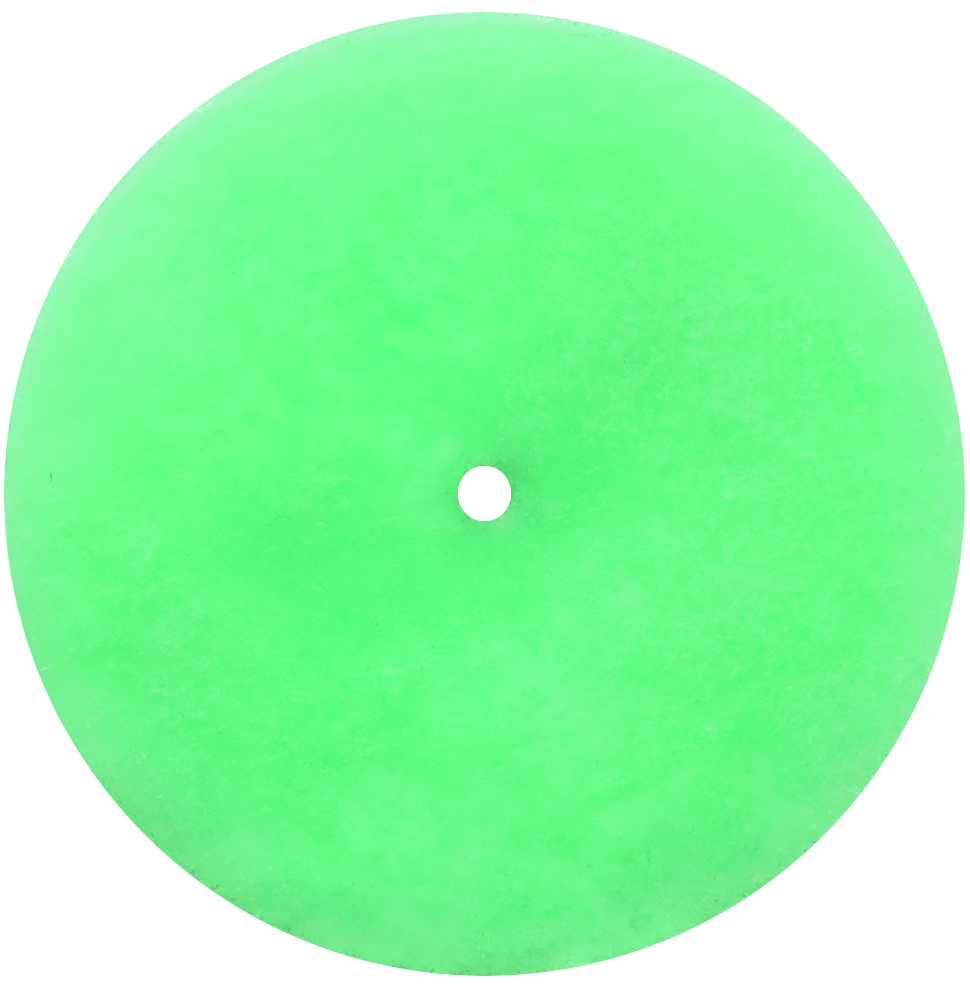
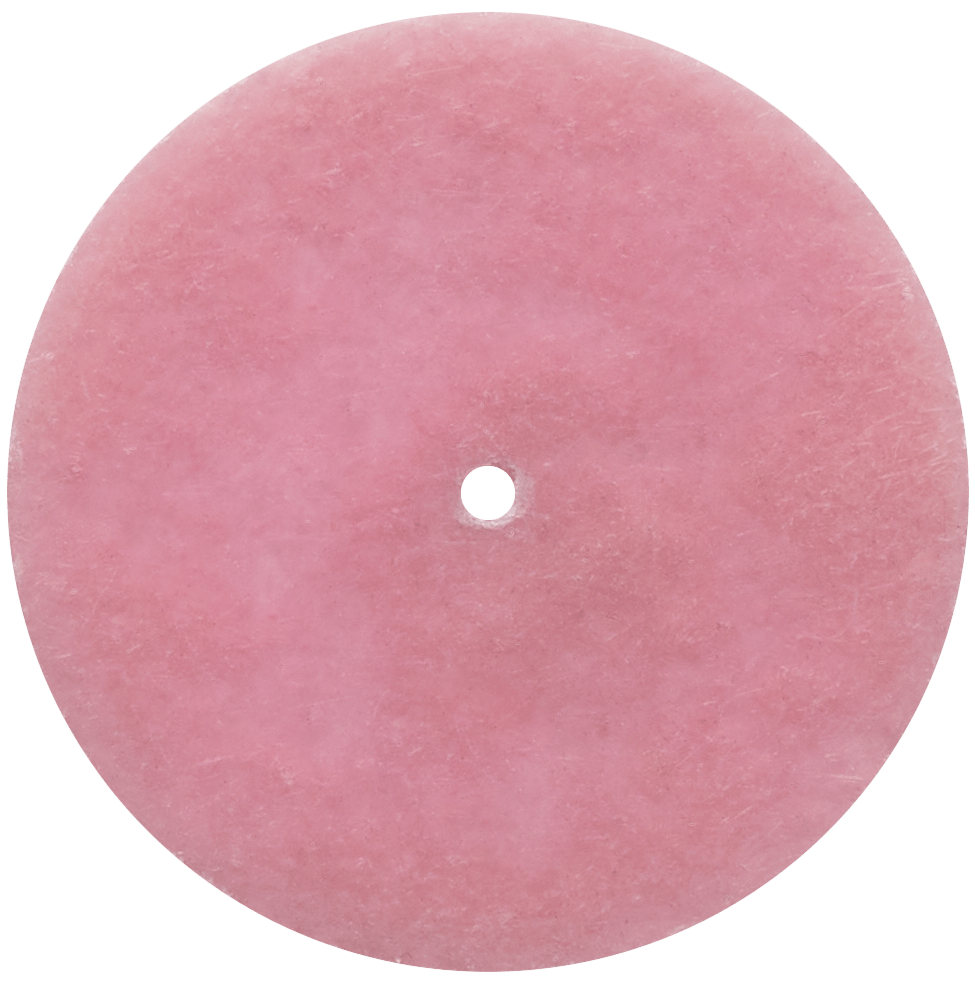
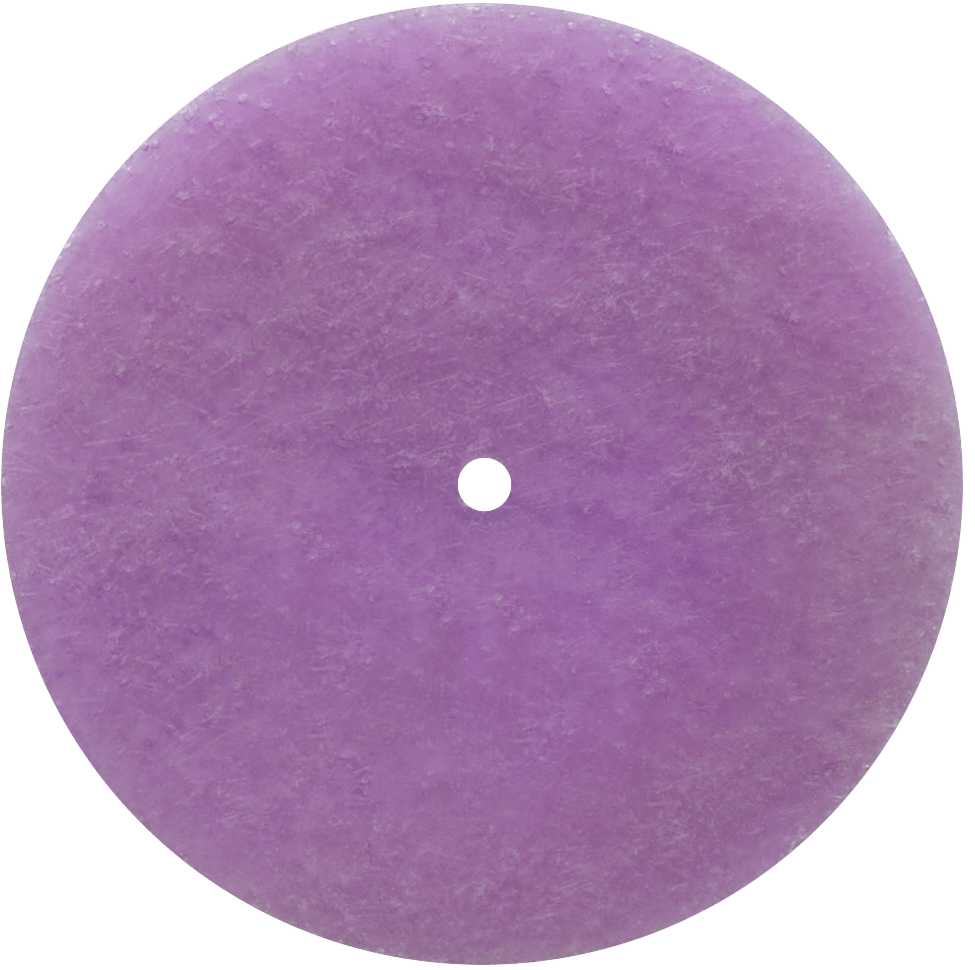
Six color-coded grits. Lower numbers are coarser for burr and stock removal; higher numbers are finer for finishing and polishing.
Technical Specifications
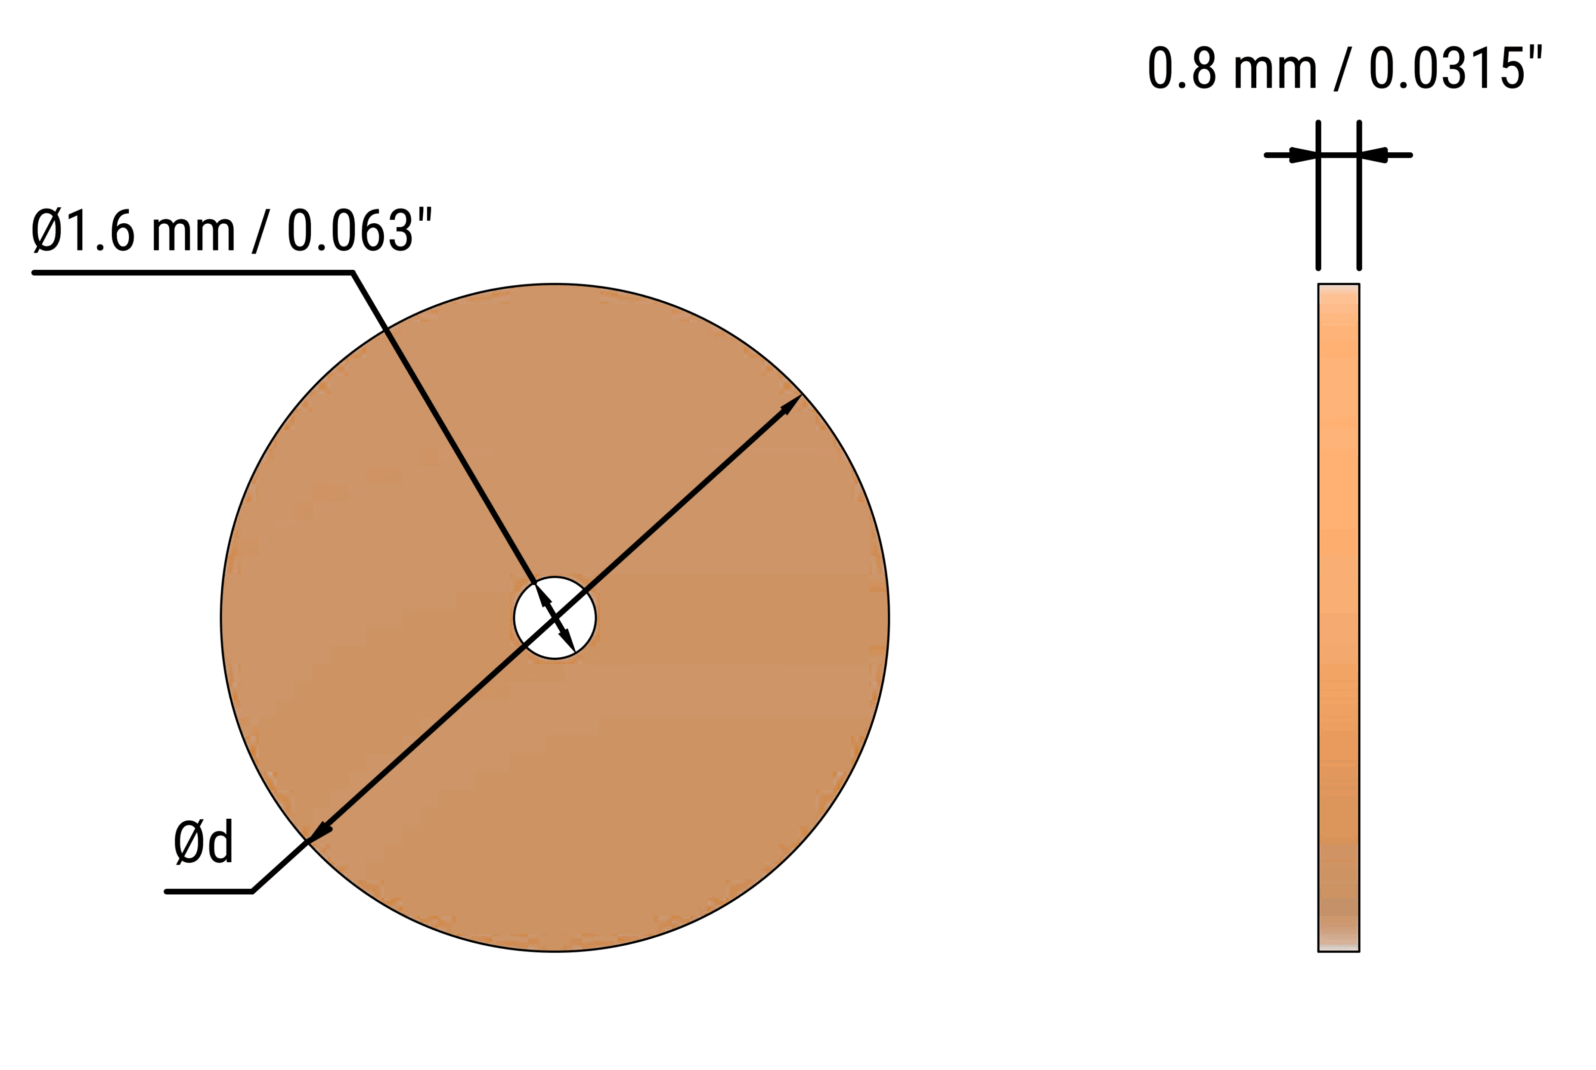
- Disc thickness
- 0.8 mm / 0.0315″
- Center hole
- Ø1.6 mm / 0.063″
- Diameters Ød
- Ø13 · 19 · 22 · 25 · 30 mm
- Grits
- #150 · #200 · #400 · #600 · #800 · #1000
- Maximum speed
- 9,000 RPM
- Recommended speed
- 6,000–8,000 RPM
- Drive
- Electric spindle or rotary tool · CNC · Robot · Portable E-Pack
- Not for
- Pneumatic (air) tools
Product Range
30 discs in five diameters and six grits — all 0.8 mm / 0.0315″ thick, max. 9,000 RPM. Description format UF-GD-[color]-D[Ø]-L008.
| SKU | Description | Grit | Ødmm / inch | Max. spindle speedmin⁻¹ (RPM) |
|---|---|---|---|---|
| UF7113 | UF-GD-G-D013-L008 | 150Green | Ø13mm / 0.512″ | 9,000RPM max. |
| UF7213 | UF-GD-P-D013-L008 | 200Pink | ||
| UF7313 | UF-GD-V-D013-L008 | 400Violet | ||
| UF7413 | UF-GD-O-D013-L008 | 600Orange | ||
| UF7513 | UF-GD-B-D013-L008 | 800Blue | ||
| UF7613 | UF-GD-W-D013-L008 | 1000White | ||
| UF7119 | UF-GD-G-D019-L008 | 150Green | Ø19mm / 0.748″ | 9,000RPM max. |
| UF7219 | UF-GD-P-D019-L008 | 200Pink | ||
| UF7319 | UF-GD-V-D019-L008 | 400Violet | ||
| UF7419 | UF-GD-O-D019-L008 | 600Orange | ||
| UF7519 | UF-GD-B-D019-L008 | 800Blue | ||
| UF7619 | UF-GD-W-D019-L008 | 1000White | ||
| UF7122 | UF-GD-G-D022-L008 | 150Green | Ø22mm / 0.866″ | 9,000RPM max. |
| UF7222 | UF-GD-P-D022-L008 | 200Pink | ||
| UF7322 | UF-GD-V-D022-L008 | 400Violet | ||
| UF7422 | UF-GD-O-D022-L008 | 600Orange | ||
| UF7522 | UF-GD-B-D022-L008 | 800Blue | ||
| UF7622 | UF-GD-W-D022-L008 | 1000White | ||
| UF7125 | UF-GD-G-D025-L008 | 150Green | Ø25mm / 0.984″ | 9,000RPM max. |
| UF7225 | UF-GD-P-D025-L008 | 200Pink | ||
| UF7325 | UF-GD-V-D025-L008 | 400Violet | ||
| UF7425 | UF-GD-O-D025-L008 | 600Orange | ||
| UF7525 | UF-GD-B-D025-L008 | 800Blue | ||
| UF7625 | UF-GD-W-D025-L008 | 1000White | ||
| UF7130 | UF-GD-G-D030-L008 | 150Green | Ø30mm / 1.181″ | 9,000RPM max. |
| UF7230 | UF-GD-P-D030-L008 | 200Pink | ||
| UF7330 | UF-GD-V-D030-L008 | 400Violet | ||
| UF7430 | UF-GD-O-D030-L008 | 600Orange | ||
| UF7530 | UF-GD-B-D030-L008 | 800Blue | ||
| UF7630 | UF-GD-W-D030-L008 | 1000White |
Quick SKU finder — grit × diameter
| Grit | Ø13 mm0.512″ | Ø19 mm0.748″ | Ø22 mm0.866″ | Ø25 mm0.984″ | Ø30 mm1.181″ |
|---|---|---|---|---|---|
| #150Green | UF7113 | UF7119 | UF7122 | UF7125 | UF7130 |
| #200Pink | UF7213 | UF7219 | UF7222 | UF7225 | UF7230 |
| #400Violet | UF7313 | UF7319 | UF7322 | UF7325 | UF7330 |
| #600Orange | UF7413 | UF7419 | UF7422 | UF7425 | UF7430 |
| #800Blue | UF7513 | UF7519 | UF7522 | UF7525 | UF7530 |
| #1000White | UF7613 | UF7619 | UF7622 | UF7625 | UF7630 |
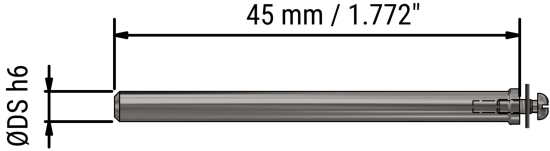
Disc Clamping Shanks
Every disc mounts on a clamping shank. Choose the shank diameter to fit your spindle collet or E-Pack handpiece.
| SKU | Description | ØDS h6 | Length |
|---|---|---|---|
| UF7023 | UF-DA-016-C023-L45 | Ø2.35 / 0.093″ | 45 / 1.772″ |
| UF7030 | UF-DA-016-C030-L45 | Ø3.0 / 0.118″ | 45 / 1.772″ |
Spare parts (both shanks): clamping screw M1.6 × 0.35 mm · washer O.D. Ø5.0 × I.D. Ø1.61 × H 0.48 mm (O.D. Ø0.197″ × I.D. Ø0.063″ × H 0.019″).
Machining Recommendations
Starting parameters for CNC and robotic deburring, grinding, finishing and polishing. Use the lower value first and optimize on the actual component.
| Workpiece material | Deburring / grinding | Finishing / polishing | Coolant | ||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|
| ISO | Material group | Condition | Vcm/min | Feedmm/min | Engagementmm | UFIBER grit | Vcm/min | Feedmm/min | Engagementmm | UFIBER grit | Recommendedmethod |
| P | Non-Alloyed & Alloy Steels | Annealed | 150–250 | 200–500 | 0.05–0.15 | #150#200#400 | 100–180 | 200–450 | 0.02–0.08 | #600#800#1000 | Air / Wet |
| Quenched & Tempered | 100–180 | 150–400 | 0.04–0.12 | #150#200#400 | 80–150 | 150–350 | 0.02–0.06 | #600#800#1000 | Wet preferred | ||
| M | Stainless Steel | Austenitic | 100–180 | 150–400 | 0.04–0.12 | #200#400 | 80–150 | 150–350 | 0.02–0.06 | #600#800#1000 | Wet recommended |
| Ferritic / Martensitic | 100–180 | 150–400 | 0.04–0.12 | #200#400 | 80–150 | 150–350 | 0.02–0.06 | #600#800#1000 | Wet recommended | ||
| K | Grey Cast Iron | — | 180–300 | 250–600 | 0.05–0.15 | #150#200#400 | 120–200 | 200–500 | 0.02–0.08 | #600#800 | Air preferred |
| Nodular Cast Iron | — | 150–250 | 200–500 | 0.05–0.15 | #150#200#400 | 100–180 | 200–450 | 0.02–0.08 | #600#800 | Air preferred | |
| N | Aluminum Wrought Alloys | Non-Hardenable | 250–400 | 300–800 | 0.03–0.10 | #400#600 | 180–300 | 300–700 | 0.01–0.05 | #800#1000 | Wet / MQL |
| Aluminum Alloys | Hardenable | 200–350 | 250–700 | 0.03–0.10 | #400#600 | 150–250 | 250–600 | 0.01–0.05 | #800#1000 | Wet / MQL | |
| Copper Alloys | Brass / Bronze | 200–350 | 250–700 | 0.03–0.10 | #400#600 | 150–250 | 250–600 | 0.01–0.05 | #800#1000 | Wet / MQL | |
| S | Heat-Resistant Alloys | Annealed | 60–120 | 100–300 | 0.03–0.10 | #150#200#400 | 50–100 | 100–250 | 0.01–0.05 | #600#800#1000 | Wet recommended |
| Hardened | 50–100 | 100–250 | 0.03–0.08 | #150#200#400 | 40–80 | 100–200 | 0.01–0.04 | #600#800#1000 | Wet recommended | ||
| Titanium Alloys | — | 60–120 | 100–300 | 0.03–0.10 | #150#200#400 | 50–100 | 100–250 | 0.01–0.05 | #600#800#1000 | Wet recommended | |
| H | Hardened Steel | 45–55 HRC | 50–120 | 100–300 | 0.03–0.10 | #150#200#400 | 50–100 | 100–250 | 0.01–0.05 | #600#800#1000 | Wet preferred |
| >55 HRC | 40–100 | 100–250 | 0.02–0.08 | #150#200#400 | 40–80 | 100–200 | 0.01–0.04 | #600#800#1000 | Wet preferred | ||
Spindle Speed Calculator
Calculate the spindle speed for your cutting speed and disc diameter. The result is checked against the 9,000 RPM disc limit.
Vc = cutting speed in m/min · D = diameter in mm
Vc = cutting speed in SFM · D = diameter in inches
Enter the cutting speed and disc diameter.
Typical Applications
Use the disc where a conventional rotary abrasive is too wide, or where precise, controlled contact is required.
Radial deburring & edge finishing
Burr removal and controlled edge refinement in narrow, hard-to-reach features.
Narrow grooves & slots
The 0.8 mm profile reaches rib bottoms, slots and narrow grooves.
Rib bottoms & side walls
Precision radial finishing of rib bottoms, side walls and confined geometries.
Internal & external profiles
Controlled deburring, grinding and polishing along profiles.
Local grinding & polishing
From removing machining marks to fine surface polishing.
CNC & robotic finishing
Repeatable automated finishing with an electric spindle or robotic end-effector.
How to select your disc
- DiameterØ13–Ø30 mm, by access, contact area and tool clearance. Smaller discs reach tighter spaces; larger discs give more contact and lower RPM for the same Vc.
- GritStart coarse (#150–#400) for burrs and machining marks, then finish with #600–#1000.
- Shank & driveUF7023 (Ø2.35 mm) or UF7030 (Ø3 mm) on an electric spindle, robot end-effector or the Portable E-Pack — at or below 9,000 RPM.
3D Models
STEP models of the ceramic discs on the 3 mm / 0.118″ clamping shank, for CAM and robot cell programming.
Safe Use of the Radial Ceramic Fiber Disc
Read these instructions before use. Abrasive grinding and polishing dust can damage CNC machine components, and disc breakage or fragments may cause serious personal injury. Always follow the machine, spindle, toolholder and workplace safety instructions.
Use appropriate machine guarding or a closed machine enclosure. Always wear suitable eye and face protection, and inspect the disc and mounting components before every use.
1. Before use
- Inspect the ceramic fiber disc, adapter, clamping screw and washer before every use.
- Do not use cracked, chipped, loose, deformed or otherwise damaged components.
- Confirm the disc is securely mounted and runs true before contacting the workpiece.
- Never exceed the lowest rated speed of the disc, holder, adapter, spindle or machine.
- Maximum permitted disc speed is 9,000 RPM.
2. During operation
- Keep machine guards or the machine enclosure closed whenever possible.
- Verify smooth rotation before contacting the workpiece.
- Use light, controlled contact. Do not force, jam or excessively side-load the disc.
- Keep hands, hair, jewelry and loose clothing away from rotating components.
- Stop the spindle completely before touching, adjusting or replacing the disc.
3. Abrasive dust & CNC protection
- Grinding and polishing generate abrasive powder that may enter CNC guideways, bearings, seals and other precision components.
- Abrasive dust may cause accelerated wear or damage to machine components.
- Use effective local dust extraction or a dust collector, especially during dry processing.
- Keep the machine enclosure, spindle area, tool changer, guideways and surrounding equipment clean.
- Do not let grinding powder or abrasive dust accumulate inside the machine.
- Do not use compressed air in a way that drives abrasive dust deeper into machine components.
4. PPE & disc dressing
- Wear safety glasses with side protection.
- Use a face shield and respiratory protection when required by the process, dust level or workplace risk assessment.
- Wear suitable protective clothing and follow your workplace PPE requirements.
- Dress or reshape the disc only with a suitable diamond dressing tool and controlled contact.
- After dressing, inspect the disc again and verify secure mounting and true running before restarting.
Stop the machine if the disc is damaged, runs out of true, vibrates, overheats or produces unusual noise. Replace damaged components before restarting.
These instructions supplement, and do not replace, the machine manufacturer's instructions, spindle and toolholder instructions and applicable workplace safety requirements. NOGA MT · UFIBER® Radial Ceramic Fiber Disc.
Frequently Asked Questions
What is the UFIBER® Radial Ceramic Fiber Disc?
Which disc diameters are available?
Which grit sizes are available?
What is the maximum speed?
Which rotary tool should I use?
Can the disc be used on CNC machines and robots?
How is the disc mounted?
Can the disc be dressed or reshaped?
More UFIBER® Tools
Need help selecting the right disc?
Send us the workpiece material, burr condition, required finish, available access and machine details — including the CNC spindle or robot end-effector.