
UFIBER® End Brush
Precision ceramic-fiber tools for controlled deburring, edge finishing and polishing of localized surfaces, chamfers, corners and recessed features. Available in Flat End and 45° configurations for CNC, robotic and controlled manual operation.
- Localized Deburring
- Flat End
- 45° End
- Chamfer Finishing
- CNC / Robot Ready

FINISHING
End-Type Brush – UFIBER® Technical Specifications & Application Guide
UFIBER® End Brushes are precision ceramic-fiber tools designed for controlled deburring, edge finishing and polishing of localized surfaces, edges, chamfers, corners and recessed features.
Available in Flat End and 45° End configurations for CNC machines, machining centers, robotic systems and controlled hand-held rotary operation.
Compatible models
It can be used in the following environments.
Features
Controlled Cutting Action
Ceramic fibers continuously expose cutting edges, providing controlled deburring and finishing with consistent contact.
CNC & Robotic Ready
Suitable for automated deburring and polishing on CNC machines, machining centers and robotic systems.
Flat & 45° Configurations
Choose a Flat End Brush for axial contact or a 45° End Brush for chamfers, corners, recesses and difficult-to-access geometries.
Ø5 mm Compact Brush
The compact Ø5 mm brush provides controlled access to localized surfaces and features where larger Surface Brushes may not be suitable.
Up to 12,000 RPM
Designed for operation at spindle speeds up to 12,000 RPM when correctly mounted and operated within the recommended machining conditions.
Adjustable Brush Tip
The ceramic-fiber tip can be shaped when required using a suitable diamond dressing tool to adapt the contact geometry to the application.
End-Type Brush Product Range


| Series | Brush Type | Description | Brush Diameter | Available Grits | Maximum Speed |
|---|---|---|---|---|---|
| UF4...50 | Flat End | UF-EB-...-D5-L20 | Ø5 mm 0.197" | #150 – #6000 | 12,000 RPM |
| UF6...50 | 45° End | UF-EB45-...-D5-L20 | Ø5 mm 0.197" | #150 – #6000 | 12,000 RPM |
Flat End vs. 45° End Brush
Flat End Type
Designed for controlled axial contact on localized flat surfaces, edges and small planar areas.
Best for: Flat-surface deburring • Outer-edge finishing • Spot polishing • Localized planar surfaces • Axial contact
45° End Type
Designed for selective contact with chamfers, angled surfaces, corners and recessed geometries.
Best for: Chamfer deburring • Angled surfaces • Corners and recesses • Selective edge finishing • Difficult-to-access locations
Grit Selection by Burr Condition & Material
| Grit | Code | Relative Action | Typical Application |
|---|---|---|---|
| #150 | G | Very aggressive | Heavy burrs and hardened materials |
| #200 | P | Aggressive | Hardened steels and difficult burrs |
| #400 | V | Medium-coarse | Steel, stainless steel and heat-resistant alloys |
| #600 | O | General deburring | General-purpose metal deburring |
| #800 | B | Fine deburring | Fine burr removal and pre-finishing |
| #1000 | W | Fine finishing | Controlled surface finishing |
| #1200 | R | Fine polishing | Final finishing and non-ferrous materials |
| #2000 | M | Very fine | Aluminum, plastics and delicate surfaces |
| #3000 | Z | Ultra-fine | Composites and high-finish applications |
| #6000 | A | Micro-finish | Final polishing of composites and plastics |
How to Use the UFIBER® End Brush
1. Select the Contact Geometry
Use the Flat End Brush for axial surface contact and the 45° End Brush for chamfers, corners or recessed features.
2. Start with Light Engagement
Begin with minimum brush engagement. Increase contact only when additional cutting action is required.
3. Maintain Controlled Movement
Move continuously over the machining area and avoid holding the rotating brush at one point for an extended period.
UFIBER® END BRUSH — MACHINING RECOMMENDATIONS
Search by material, condition, grade, DIN number, grit or recommended method, or filter directly by ISO material group.
| Starting parameters for CNC deburring and polishing • Metric and imperial units • Use the lower value first and optimize on the actual component | |||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| WORKPIECE MATERIAL | DEBURRING | POLISHING | COOLANT | ||||||||||
| ISO | Material Group | Material Details | Condition | Grade AISI / SAE / ASTM + DIN |
RPM | Feed mm/min • in/min |
Engagement mm • inch |
UFIBER Deburring Grit | RPM | Feed mm/min • in/min |
Engagement mm • inch |
UFIBER Polishing Grit | Recommended Method |
| P | Non-alloy steel and cast steel, free cutting steel | <0.25% C | Annealed | 10201.0044 | 10,800–12,000 | 1200–2000 47.2–78.7 |
0.3–0.5 0.012–0.020" |
#400 (V) / #600 (O) #800 (B) for fine burrs |
10,500–12,000 | 700–1400 27.6–55.1 |
0.1–0.2 0.004–0.008" |
#800 (B) → #1200 (R) | Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | ≥0.25% C | Annealed | 10351.0501 | 7,300–12,000 | 1200–2000 47.2–78.7 |
0.3–0.5 0.012–0.020" |
#400 (V) / #600 (O) | 10,500–12,000 | 700–1400 27.6–55.1 |
0.1–0.2 0.004–0.008" |
#800 (B) → #1200 (R) | Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | <0.55% C | Quenched and tempered | 10451.1201 | 6,400–12,000 | 1000–1700 39.4–66.9 |
0.25–0.45 0.010–0.018" |
#150 / #200 / #400 | 8,900–12,000 | 600–1100 23.6–43.3 |
0.08–0.18 0.003–0.007" |
#400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | ≥0.55% C | Annealed | 10551.0535 | 6,000–12,000 | 1000–1700 | 0.25–0.45 | #150 / #200 / #400 | 9,500–12,000 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | ≥0.55% C | Quenched and tempered | 10601.1221 | 5,100–12,000 | 1000–1700 | 0.25–0.45 | #150 / #200 / #400 | 7,600–12,000 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Annealed | G926001.5028 | 6,000–12,000 | 1000–1800 | 0.25–0.5 | #400 / #600 | 10,500–12,000 | 600–1200 | 0.08–0.2 | #800 → #1200 | Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Quenched and tempered | 41301.7218 | 5,100–12,000 | 1000–1800 | 0.25–0.5 | #150 / #200 / #400 | 8,300–12,000 | 600–1200 | 0.08–0.2 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Quenched and tempered | 41421.2332 | 5,100–12,000 | 1000–1800 | 0.25–0.5 | #150 / #200 / #400 | 8,300–12,000 | 600–1200 | 0.08–0.2 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Quenched and tempered | 50451.7006 | 5,100–12,000 | 1000–1800 | 0.25–0.5 | #150 / #200 / #400 | 8,300–12,000 | 600–1200 | 0.08–0.2 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | High alloyed steel, cast steel and tool steel | — | Annealed | H131.2344 | 3,800–9,500 | 700–1400 | 0.2–0.4 | #150 / #200 / #400 | 12,000 max. | 400–800 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| P | High alloyed steel, cast steel and tool steel | — | Quenched and tempered | M331.3249 | 3,200–7,600 | 700–1400 | 0.2–0.4 | #150 / #200 / #400 | 12,000 max. | 400–800 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| P | Stainless steel and cast steel | Ferritic / martensitic | — | 4201.4021 | 3,800–8,900 | 800–1500 | 0.2–0.4 | #150 / #200 / #400 | 9,500–12,000 | 600–1200 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| P | Stainless steel and cast steel | Martensitic | — | —— | 3,200–7,600 | 800–1500 | 0.2–0.4 | #150 / #200 / #400 | 7,600–12,000 | 600–1200 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| M | Stainless steel | Austenitic, duplex | — | 304L1.4306 | 3,200–7,600 | 800–1500 | 0.2–0.4 | #400 / #600 #800 fine burrs |
9,500–12,000 | 600–1200 | 0.05–0.2 | #800 → #1200 | Wet recommended |
| K | Gray cast iron (GG) | Ferritic / pearlitic | — | Class 250.6015 | 3,800–10,800 | 900–1600 | 0.25–0.45 | #200 / #400 #600 fine burrs |
7,600–12,000 | 600–1100 | 0.08–0.18 | #600 → #1000 | Air preferred |
| K | Gray cast iron (GG) | Pearlitic / martensitic | — | Grade H2036037 | 3,200–8,900 | 900–1600 | 0.25–0.45 | #150 / #200 / #400 | 6,400–11,500 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air preferred |
| K | Nodular cast iron (GGG) | Ferritic | — | 60-40-180.7043 | 3,800–9,500 | 1100–1900 | 0.3–0.5 | #400 / #600 | 7,000–12,000 | 700–1300 | 0.1–0.2 | #800 → #1200 | Air preferred |
| K | Nodular cast iron (GGG) | Pearlitic | — | F335000.705 | 3,200–8,300 | 900–1600 | 0.25–0.45 | #150 / #200 / #400 | 5,700–10,800 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air preferred |
| K | Malleable cast iron | Ferritic | — | A470.8135 | 3,800–9,500 | 1100–1900 | 0.3–0.5 | #400 / #600 | 7,000–12,000 | 700–1300 | 0.1–0.2 | #800 → #1200 | Air preferred |
| K | Malleable cast iron | Pearlitic | — | A220 Class0.8155 | 3,200–8,300 | 900–1600 | 0.25–0.45 | #150 / #200 / #400 | 5,700–10,800 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air preferred |
| N | Aluminum-wrought alloys | — | Not hardenable | 50053.3315 | 11,500–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 10,500–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-wrought alloys | — | Hardenable | 70753.4365 | 10,200–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 9,500–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-cast alloys | ≤12% Si | Not hardenable | 5183.3292 | 9,900–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 8,900–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-cast alloys | ≤12% Si | Hardenable | 5153.3241 | 9,200–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 8,300–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-cast alloys | >12% Si | High temperature | 390— | 8,300–12,000 | 800–1600 | 0.2–0.4 | #600 / #800 | 6,400–12,000 | 700–1400 | 0.05–0.15 | #1000 → #1200 | Wet / MQL |
| N | Copper alloys | >1% Pb | Free cutting | C360002.0375 | 8,300–12,000 | 1000–1800 | 0.2–0.4 | #800 / #1200 | 7,600–12,000 | 800–1600 | 0.05–0.2 | #1200 → #2000 | Air / Wet |
| N | Copper alloys | — | Brass | C220002.023 | 8,900–12,000 | 1000–1800 | 0.2–0.4 | #800 / #1200 | 8,900–12,000 | 800–1600 | 0.05–0.2 | #1200 → #2000 | Air / Wet |
| N | Copper alloys | — | Electrolytic copper | C630002.0966 | 7,000–12,000 | 1000–1800 | 0.2–0.4 | #800 / #1200 | 6,400–12,000 | 800–1600 | 0.05–0.2 | #1200 → #2000 | Air / Wet |
| N | Non metallic | Duroplastics, fiber plastics | — | Bakelite— | 5,100–12,000 | 800–1600 | 0.1–0.3 | #2000 / #3000 | 5,100–10,200 | 600–1400 | 0.05–0.15 | #3000 → #6000 | Dry air + extraction |
| N | Non metallic | Hard rubber | — | Ebonite— | 3,800–11,500 | 800–1600 | 0.1–0.3 | #2000 / #3000 | 3,800–7,600 | 600–1400 | 0.05–0.15 | #3000 → #6000 | Dry air + extraction |
| S | High temperature alloys | Fe based | Annealed | 3301.4864 | 2,500–6,000 | 600–1200 | 0.1–0.3 | #150 / #200 / #400 | 5,100–10,200 | 500–1000 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Fe based | Hardened | S5901.4977 | 2,200–5,100 | 600–1200 | 0.1–0.3 | #150 / #200 / #400 | 3,800–7,600 | 500–1000 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Ni or Co based | Annealed | Incoloy 8252.4858 | 1,900–4,500 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 2,200–4,100 | 350–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Ni or Co based | Hardened | Inconel 7182.4668 | 1,600–3,500 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 1,900–3,500 | 350–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Ni or Co based | Cast | Nimocast K242.4674 | 1,600–3,800 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 1,900–3,800 | 350–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | Titanium alloys | — | Pure | Titanium G.13.7024 | 2,200–5,100 | 500–1000 | 0.1–0.3 | #150 / #200 / #400 | 2,200–4,500 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | Titanium alloys | — | Alpha+beta alloys, hardened | Titanium G.53.7165 | 1,900–4,100 | 500–1000 | 0.1–0.3 | #150 / #200 / #400 | 1,900–3,800 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| H | Hardened steel | — | Hardened | HARDOX 500— | 2,200–5,100 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 12,000 max. | 300–700 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| H | Hardened steel | — | Hardened | HARDOX Extreme— | 1,900–3,800 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 9,500–12,000 | 300–700 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| H | Chilled cast iron | — | Cast | A532 IIIA 25% Cr0.965 | 2,500–5,100 | 500–1000 | 0.15–0.3 | #150 / #200 / #400 | 6,400–11,500 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| H | Hardened cast iron | — | Hardened | A532 IID 20% CrMo0.9645 | 2,200–4,500 | 500–1000 | 0.15–0.3 | #150 / #200 / #400 | 5,100–9,500 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
Controlling Deburring & Polishing Performance
Increase Deburring Action
Coarser grit → More engagement → Lower feed → Additional controlled pass
Reduce Aggressiveness
Finer grit → Lighter engagement → Higher feed → Fewer passes
Improve Surface Finish
Finer grit sequence → Light contact → Stable feed → Finishing passes
Improve Brush Life
Reduce pressure → Correct alignment → Avoid side load → Minimum required engagement
End Brush Installation & Usage
01. Shank Grip
Grip the brush shank by at least 20 mm to ensure secure clamping.
02. Chuck Matching
Use a chuck or collet that correctly matches the brush shank diameter.
03. Minimize Runout
Keep spindle and tool runout as low as practical for stable brush contact.
04. Initial Engagement
Start with minimum contact and increase engagement gradually only when required.
05. Secure Workholding
Ensure the brush and workpiece are securely clamped before CNC operation.
06. Validate the Process
Confirm the parameters on the actual component before production use.
Manual & CNC Operating Speed Guidelines
Manual Operation
1,000 → 3,000 RPM
Start at approximately 1,000 RPM. Once stable control is established, increase gradually up to 3,000 RPM.
Automated Operation
Up to 12,000 RPM
Follow the RPM values specified in the machining recommendation table. Never exceed 12,000 RPM.
Correct Brush Contact
Use light axial contact for localized deburring, edge finishing and polishing.
For the 45° End Type, keep engagement light and use the formed tip to reach chamfers, corners and recesses.
Do not force the ceramic fibers strongly sideways against an edge. Excessive bending can reduce stability and accelerate wear.
End Brush Troubleshooting
| Problem | Recommended Adjustment |
|---|---|
| Burr remains | Use a coarser grit → slightly increase engagement → reduce feed → add another controlled pass. |
| Excessive edge rounding | Increase feed → reduce brush engagement → select a finer grit → reduce RPM if necessary. |
| Brush marks | Use a finer grit → reduce engagement → maintain stable movement → add a light finishing pass. |
| Excessive brush wear | Reduce engagement → check alignment → minimize side loading → verify runout and clamping. |
| Poor surface finish | Use a progressive grit sequence → reduce final engagement → maintain stable feed → check brush cleanliness. |
| Vibration / unstable contact | Stop operation → check chuck, runout, brush condition and workholding before restarting. |
Brush Wear & Maintenance
Brush Wear Changes Cutting Behavior
As the ceramic fibers wear and become shorter, stiffness and contact behavior may change. Re-check the process when the brush has visibly shortened.
Compensate Gradually
If the process becomes too aggressive, reduce engagement, increase feed, reduce RPM if required, or select a finer grit.
Keep the Brush Clean
Remove accumulated machining debris, dust and coolant residue. Contamination can reduce cutting consistency and surface-finish quality.
Inspect Before Production
Check the brush tip, shank, clamping condition and runout before use. Replace a damaged or unstable brush before production machining.
End Brush Safety Precautions & Instructions
Operation Safety
• Do not exceed the specified maximum spindle speed.
• Do not use pneumatic-powered hand tools.
• Stop immediately if abnormal vibration occurs.
• Avoid prolonged machining at one fixed point.
• Ensure secure tool and workpiece clamping.
Operator & Work Area Safety
• Wear suitable eye protection.
• Use respiratory protection where required.
• Use suitable dust and particle extraction.
• Keep flammable materials away from the machining area.
• Do not touch hot surfaces immediately after machining.
Technical Downloads & 3D Models
End Brush – UFIBER® Technical Specifications & Application Guide
UFIBER® End Brushes are precision ceramic-fiber tools designed for controlled deburring, edge finishing and polishing of localized surfaces, edges, chamfers, corners and recessed features.
Available in Flat End and 45° End configurations for CNC machines, machining centers, robotic systems and controlled hand-held rotary operation.
Compatible models
It can be used in the following environments.
Features
Controlled Cutting Action
Ceramic fibers continuously expose cutting edges, providing controlled deburring and finishing with consistent contact.
CNC & Robotic Ready
Suitable for automated deburring and polishing on CNC machines, machining centers and robotic systems.
Flat & 45° Configurations
Choose a Flat End Brush for axial contact or a 45° End Brush for chamfers, corners, recesses and difficult-to-access geometries.
Ø5 mm Compact Brush
The compact Ø5 mm brush provides controlled access to localized surfaces and features where larger Surface Brushes may not be suitable.
Up to 12,000 RPM
Designed for operation at spindle speeds up to 12,000 RPM when correctly mounted and operated within the recommended machining conditions.
Adjustable Brush Tip
The ceramic-fiber tip can be shaped when required using a suitable diamond dressing tool to adapt the contact geometry to the application.
End Brush Product Range
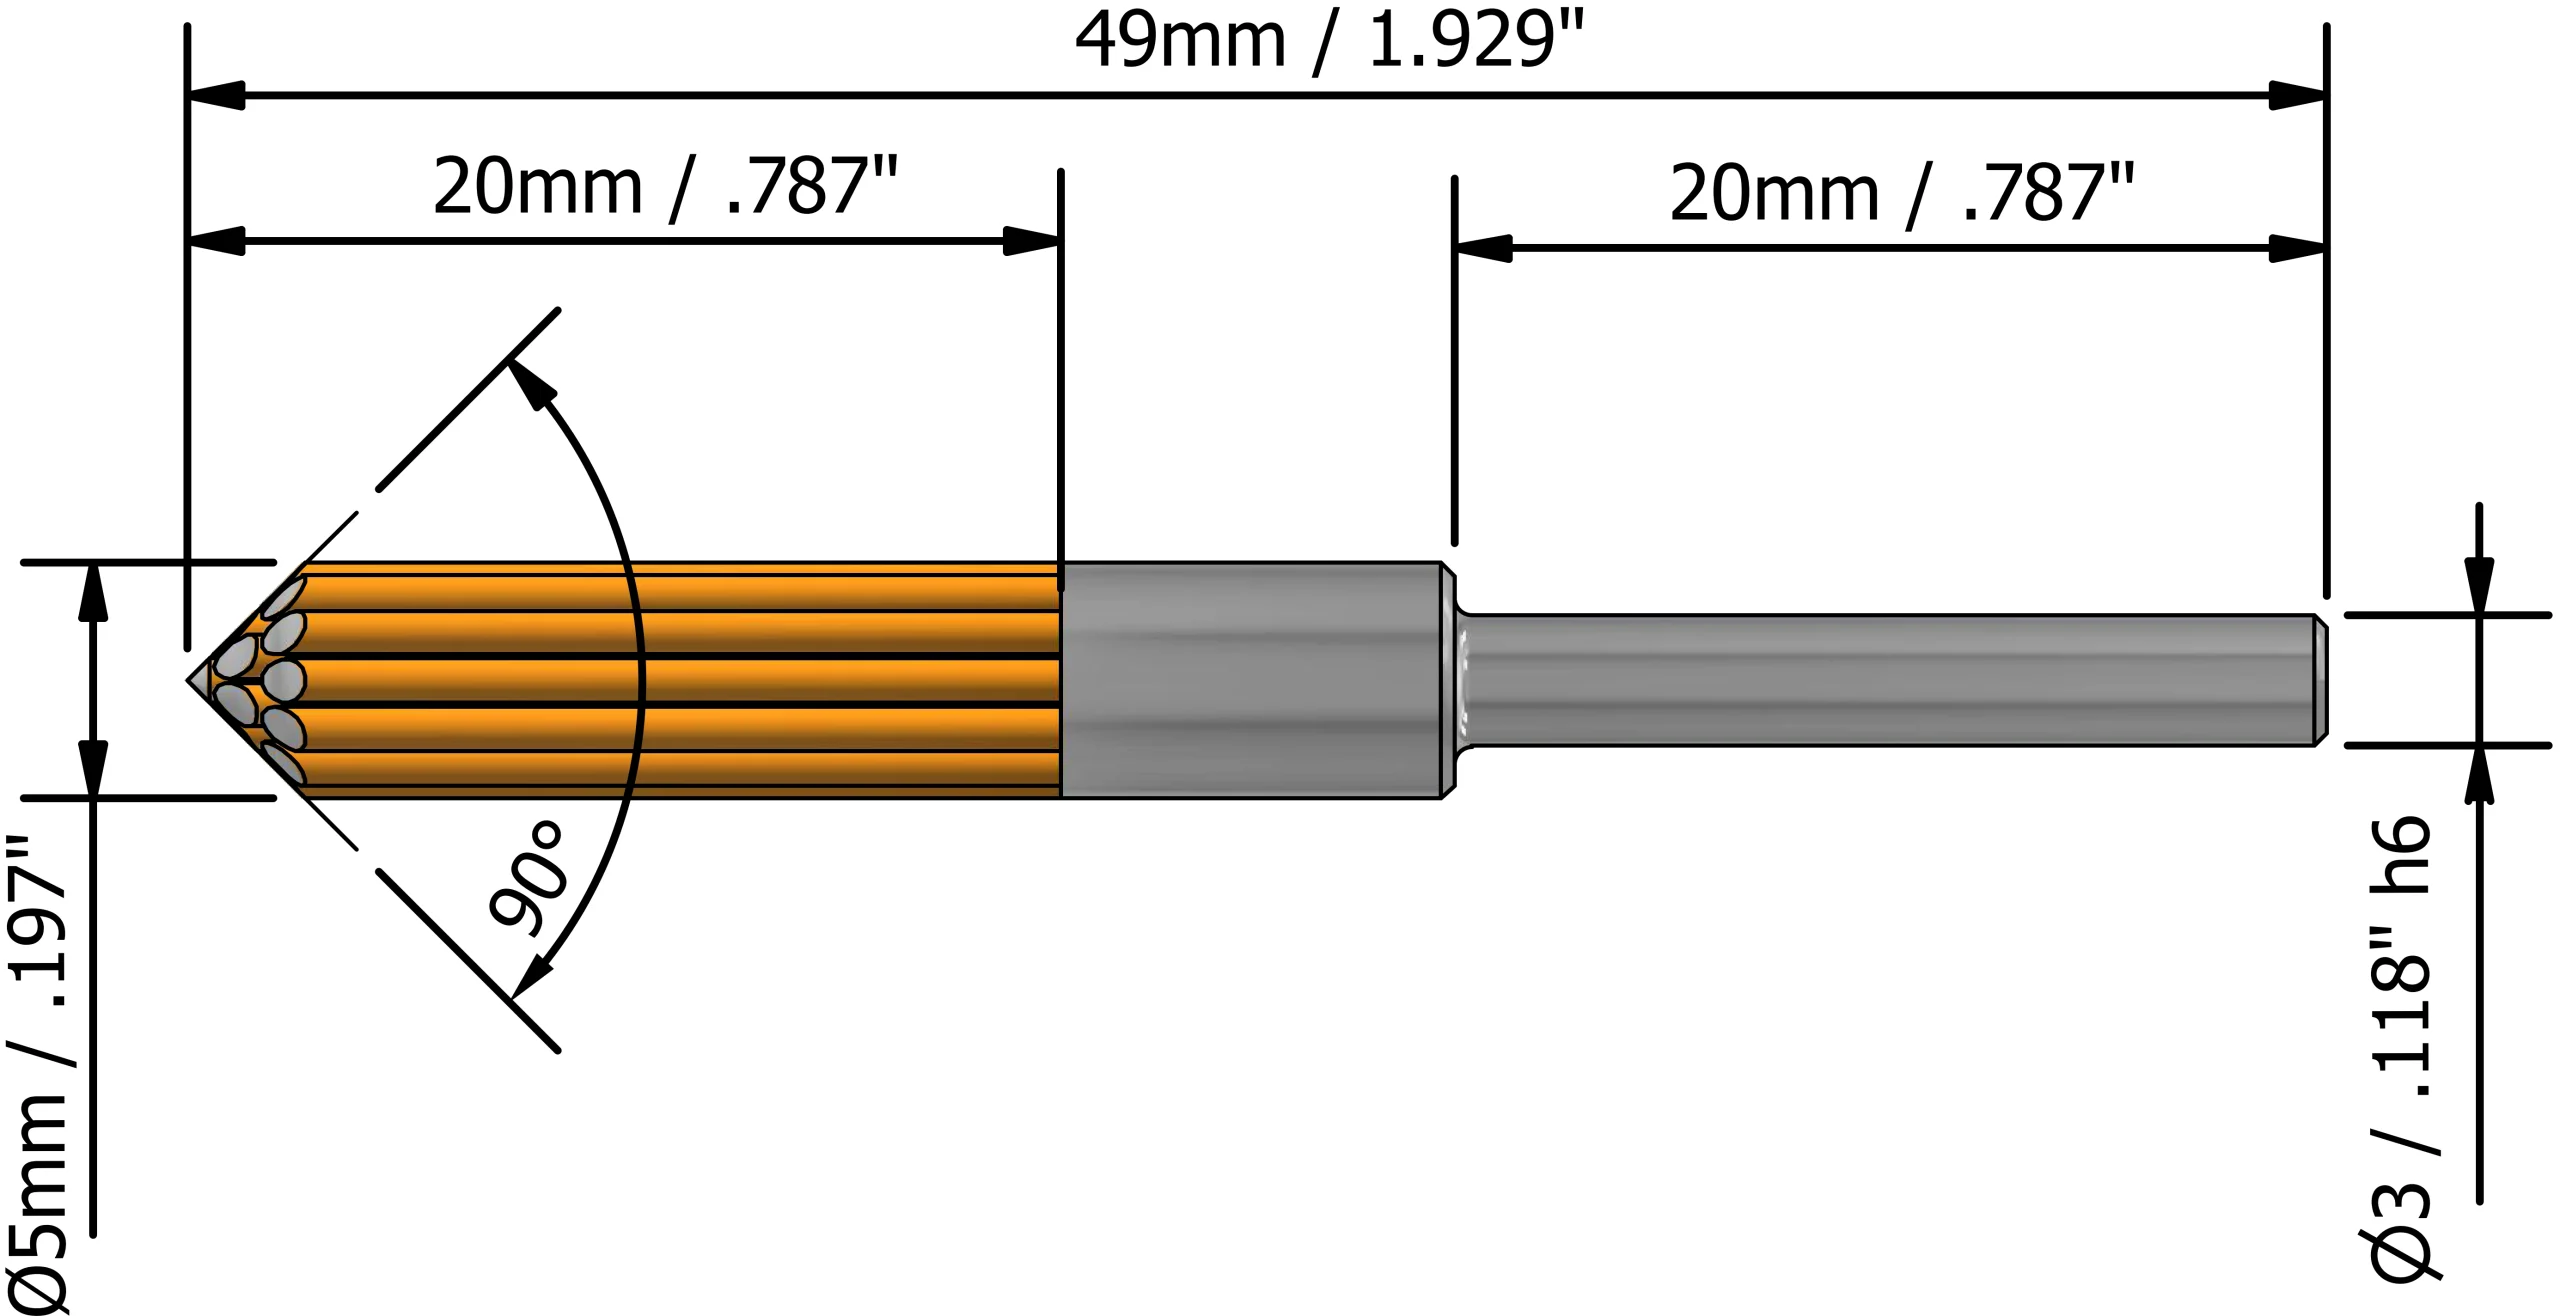
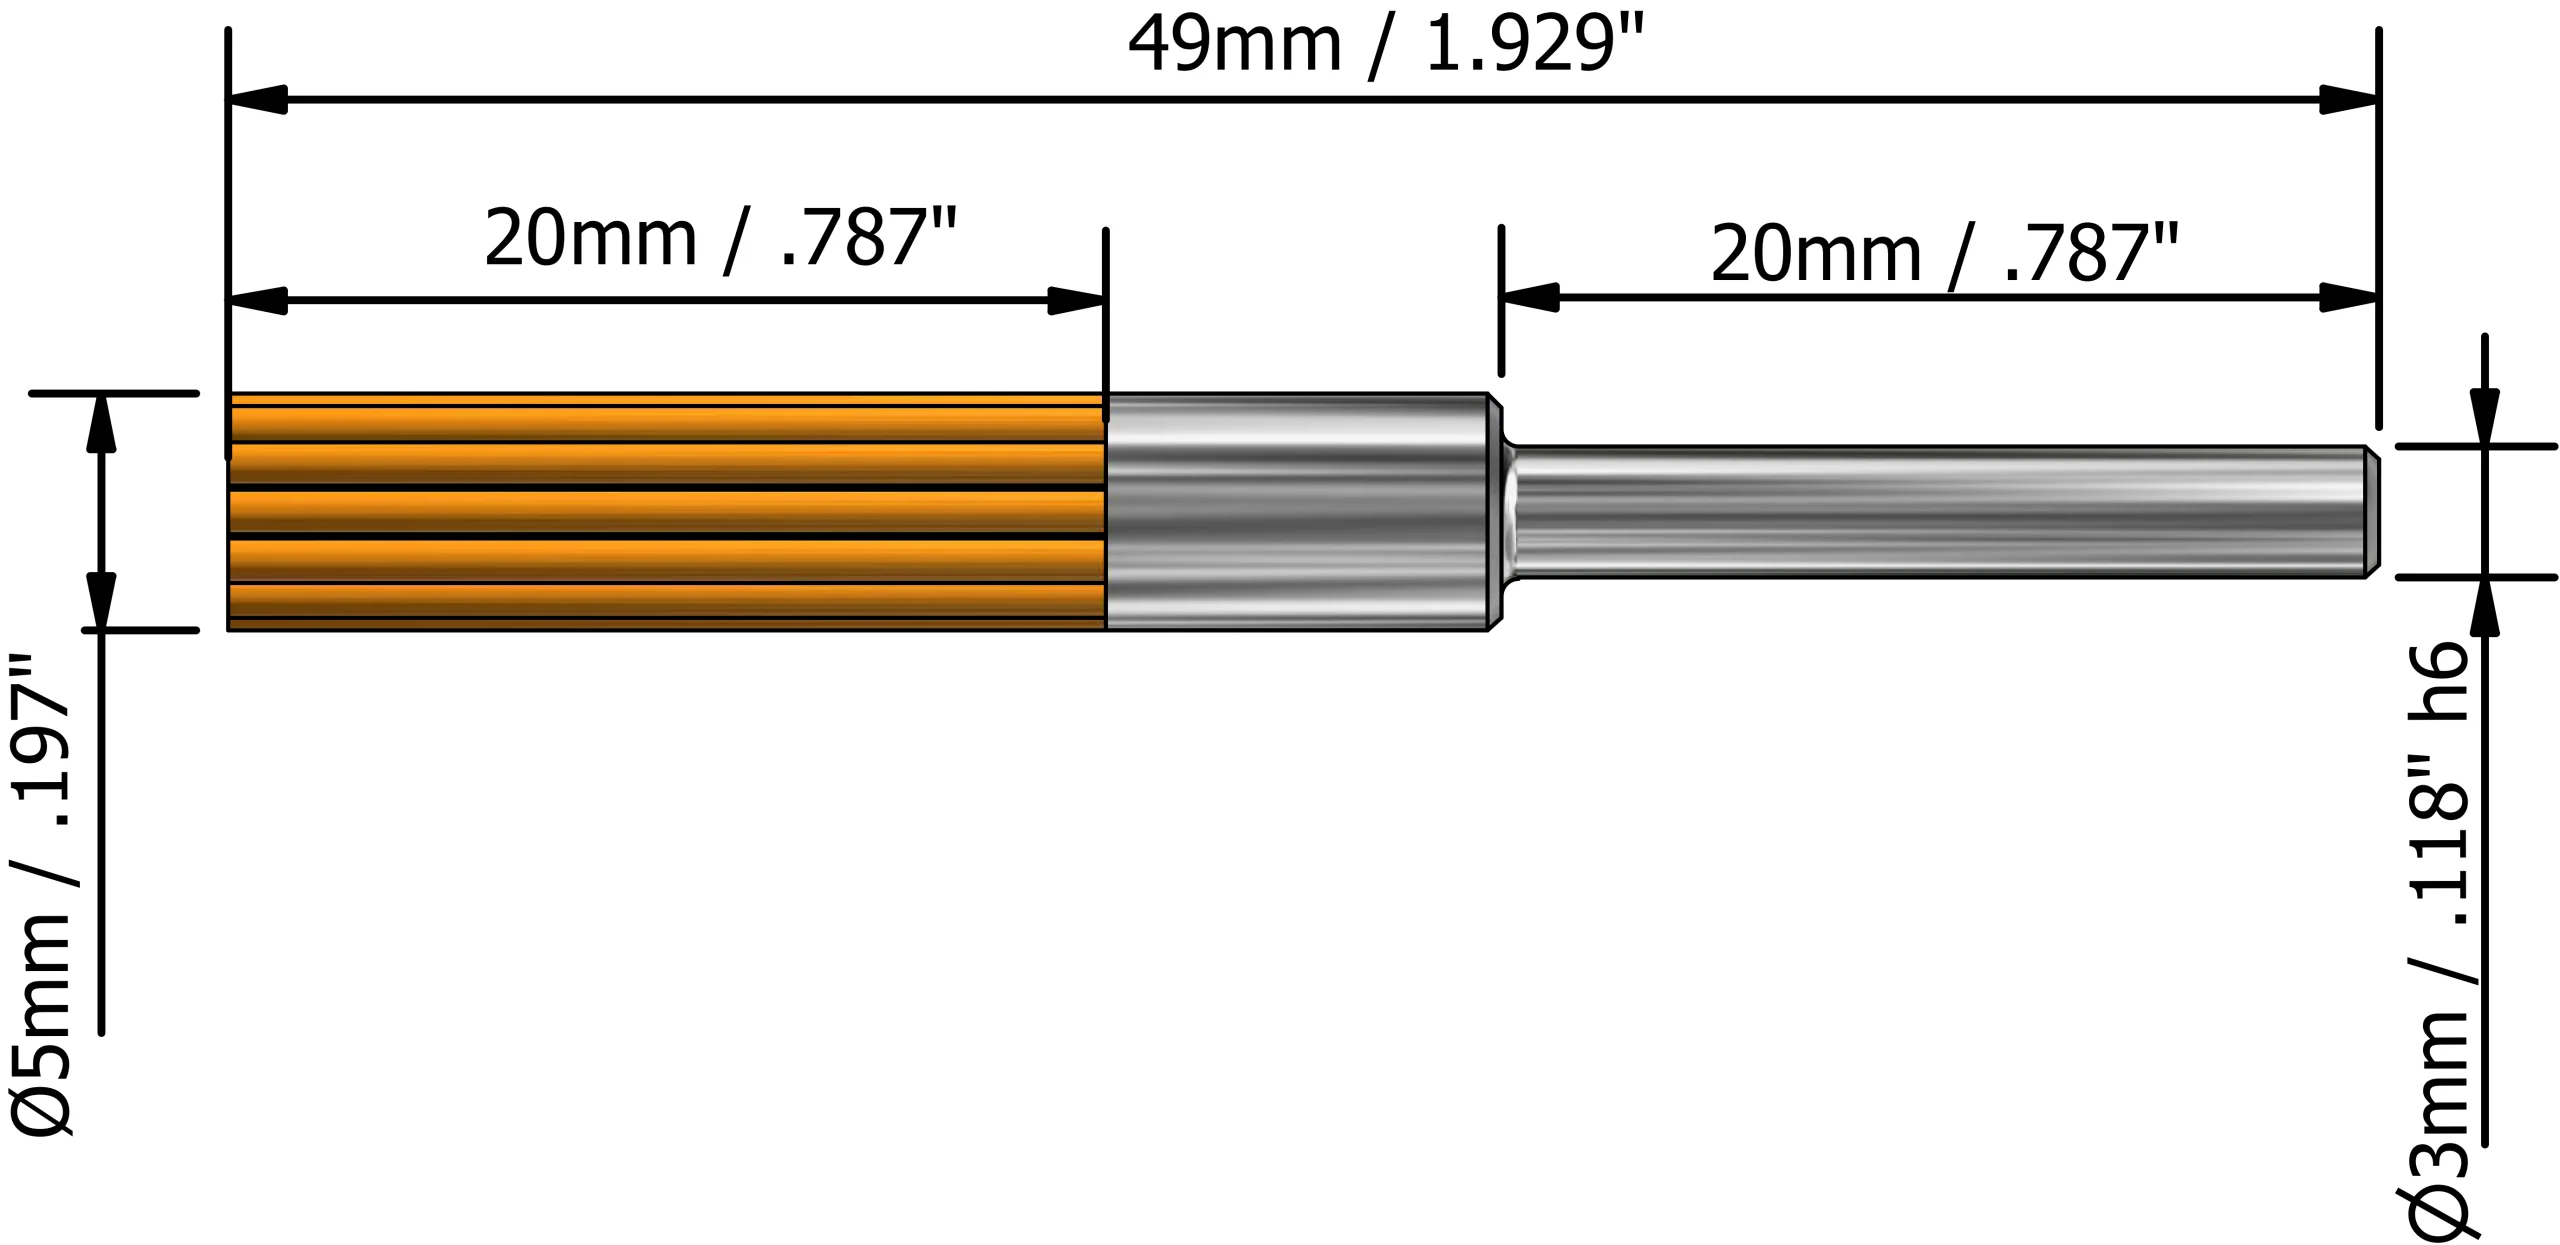
| Series | Brush Type | Description | Brush Diameter | Available Grits | Maximum Speed |
|---|---|---|---|---|---|
| UF4...50 | Flat End | UF-EB-...-D5-L20 | Ø5 mm 0.197" | #150 – #6000 | 12,000 RPM |
| UF6...50 | 45° End | UF-EB45-...-D5-L20 | Ø5 mm 0.197" | #150 – #6000 | 12,000 RPM |
Flat End vs. 45° End Brush
Flat End Type
Designed for controlled axial contact on localized flat surfaces, edges and small planar areas.
Best for: Flat-surface deburring • Outer-edge finishing • Spot polishing • Localized planar surfaces • Axial contact
45° End Type
Designed for selective contact with chamfers, angled surfaces, corners and recessed geometries.
Best for: Chamfer deburring • Angled surfaces • Corners and recesses • Selective edge finishing • Difficult-to-access locations
Grit Selection by Burr Condition & Material
| Grit | Code | Relative Action | Typical Application |
|---|---|---|---|
| #150 | G | Very aggressive | Heavy burrs and hardened materials |
| #200 | P | Aggressive | Hardened steels and difficult burrs |
| #400 | V | Medium-coarse | Steel, stainless steel and heat-resistant alloys |
| #600 | O | General deburring | General-purpose metal deburring |
| #800 | B | Fine deburring | Fine burr removal and pre-finishing |
| #1000 | W | Fine finishing | Controlled surface finishing |
| #1200 | R | Fine polishing | Final finishing and non-ferrous materials |
| #2000 | M | Very fine | Aluminum, plastics and delicate surfaces |
| #3000 | Z | Ultra-fine | Composites and high-finish applications |
| #6000 | A | Micro-finish | Final polishing of composites and plastics |
How to Use the UFIBER® End Brush
1. Select the Contact Geometry
Use the Flat End Brush for axial surface contact and the 45° End Brush for chamfers, corners or recessed features.
2. Start with Light Engagement
Begin with minimum brush engagement. Increase contact only when additional cutting action is required.
3. Maintain Controlled Movement
Move continuously over the machining area and avoid holding the rotating brush at one point for an extended period.
UFIBER® END BRUSH — MACHINING RECOMMENDATIONS
Search by material, condition, grade, DIN number, grit or recommended method, or filter directly by ISO material group.
| Starting parameters for CNC deburring and polishing • Metric and imperial units • Use the lower value first and optimize on the actual component | |||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| WORKPIECE MATERIAL | DEBURRING | POLISHING | COOLANT | ||||||||||
| ISO | Material Group | Material Details | Condition | Grade AISI / SAE / ASTM + DIN |
RPM | Feed mm/min • in/min |
Engagement mm • inch |
UFIBER Deburring Grit | RPM | Feed mm/min • in/min |
Engagement mm • inch |
UFIBER Polishing Grit | Recommended Method |
| P | Non-alloy steel and cast steel, free cutting steel | <0.25% C | Annealed | 10201.0044 | 10,800–12,000 | 1200–2000 47.2–78.7 |
0.3–0.5 0.012–0.020" |
#400 (V) / #600 (O) #800 (B) for fine burrs |
10,500–12,000 | 700–1400 27.6–55.1 |
0.1–0.2 0.004–0.008" |
#800 (B) → #1200 (R) | Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | ≥0.25% C | Annealed | 10351.0501 | 7,300–12,000 | 1200–2000 47.2–78.7 |
0.3–0.5 0.012–0.020" |
#400 (V) / #600 (O) | 10,500–12,000 | 700–1400 27.6–55.1 |
0.1–0.2 0.004–0.008" |
#800 (B) → #1200 (R) | Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | <0.55% C | Quenched and tempered | 10451.1201 | 6,400–12,000 | 1000–1700 39.4–66.9 |
0.25–0.45 0.010–0.018" |
#150 / #200 / #400 | 8,900–12,000 | 600–1100 23.6–43.3 |
0.08–0.18 0.003–0.007" |
#400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | ≥0.55% C | Annealed | 10551.0535 | 6,000–12,000 | 1000–1700 | 0.25–0.45 | #150 / #200 / #400 | 9,500–12,000 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Non-alloy steel and cast steel, free cutting steel | ≥0.55% C | Quenched and tempered | 10601.1221 | 5,100–12,000 | 1000–1700 | 0.25–0.45 | #150 / #200 / #400 | 7,600–12,000 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Annealed | G926001.5028 | 6,000–12,000 | 1000–1800 | 0.25–0.5 | #400 / #600 | 10,500–12,000 | 600–1200 | 0.08–0.2 | #800 → #1200 | Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Quenched and tempered | 41301.7218 | 5,100–12,000 | 1000–1800 | 0.25–0.5 | #150 / #200 / #400 | 8,300–12,000 | 600–1200 | 0.08–0.2 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Quenched and tempered | 41421.2332 | 5,100–12,000 | 1000–1800 | 0.25–0.5 | #150 / #200 / #400 | 8,300–12,000 | 600–1200 | 0.08–0.2 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | Low alloy and cast steel (<5% alloying elements) | — | Quenched and tempered | 50451.7006 | 5,100–12,000 | 1000–1800 | 0.25–0.5 | #150 / #200 / #400 | 8,300–12,000 | 600–1200 | 0.08–0.2 | #400 → #800 #1000 / #1200 final |
Air / Wet |
| P | High alloyed steel, cast steel and tool steel | — | Annealed | H131.2344 | 3,800–9,500 | 700–1400 | 0.2–0.4 | #150 / #200 / #400 | 12,000 max. | 400–800 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| P | High alloyed steel, cast steel and tool steel | — | Quenched and tempered | M331.3249 | 3,200–7,600 | 700–1400 | 0.2–0.4 | #150 / #200 / #400 | 12,000 max. | 400–800 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| P | Stainless steel and cast steel | Ferritic / martensitic | — | 4201.4021 | 3,800–8,900 | 800–1500 | 0.2–0.4 | #150 / #200 / #400 | 9,500–12,000 | 600–1200 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| P | Stainless steel and cast steel | Martensitic | — | —— | 3,200–7,600 | 800–1500 | 0.2–0.4 | #150 / #200 / #400 | 7,600–12,000 | 600–1200 | 0.05–0.2 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| M | Stainless steel | Austenitic, duplex | — | 304L1.4306 | 3,200–7,600 | 800–1500 | 0.2–0.4 | #400 / #600 #800 fine burrs |
9,500–12,000 | 600–1200 | 0.05–0.2 | #800 → #1200 | Wet recommended |
| K | Gray cast iron (GG) | Ferritic / pearlitic | — | Class 250.6015 | 3,800–10,800 | 900–1600 | 0.25–0.45 | #200 / #400 #600 fine burrs |
7,600–12,000 | 600–1100 | 0.08–0.18 | #600 → #1000 | Air preferred |
| K | Gray cast iron (GG) | Pearlitic / martensitic | — | Grade H2036037 | 3,200–8,900 | 900–1600 | 0.25–0.45 | #150 / #200 / #400 | 6,400–11,500 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air preferred |
| K | Nodular cast iron (GGG) | Ferritic | — | 60-40-180.7043 | 3,800–9,500 | 1100–1900 | 0.3–0.5 | #400 / #600 | 7,000–12,000 | 700–1300 | 0.1–0.2 | #800 → #1200 | Air preferred |
| K | Nodular cast iron (GGG) | Pearlitic | — | F335000.705 | 3,200–8,300 | 900–1600 | 0.25–0.45 | #150 / #200 / #400 | 5,700–10,800 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air preferred |
| K | Malleable cast iron | Ferritic | — | A470.8135 | 3,800–9,500 | 1100–1900 | 0.3–0.5 | #400 / #600 | 7,000–12,000 | 700–1300 | 0.1–0.2 | #800 → #1200 | Air preferred |
| K | Malleable cast iron | Pearlitic | — | A220 Class0.8155 | 3,200–8,300 | 900–1600 | 0.25–0.45 | #150 / #200 / #400 | 5,700–10,800 | 600–1100 | 0.08–0.18 | #400 → #800 #1000 / #1200 final |
Air preferred |
| N | Aluminum-wrought alloys | — | Not hardenable | 50053.3315 | 11,500–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 10,500–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-wrought alloys | — | Hardenable | 70753.4365 | 10,200–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 9,500–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-cast alloys | ≤12% Si | Not hardenable | 5183.3292 | 9,900–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 8,900–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-cast alloys | ≤12% Si | Hardenable | 5153.3241 | 9,200–12,000 | 1200–2000 | 0.2–0.5 | #800 / #1200 | 8,300–12,000 | 1000–1800 | 0.05–0.2 | #1200 → #2000 | Wet / MQL |
| N | Aluminum-cast alloys | >12% Si | High temperature | 390— | 8,300–12,000 | 800–1600 | 0.2–0.4 | #600 / #800 | 6,400–12,000 | 700–1400 | 0.05–0.15 | #1000 → #1200 | Wet / MQL |
| N | Copper alloys | >1% Pb | Free cutting | C360002.0375 | 8,300–12,000 | 1000–1800 | 0.2–0.4 | #800 / #1200 | 7,600–12,000 | 800–1600 | 0.05–0.2 | #1200 → #2000 | Air / Wet |
| N | Copper alloys | — | Brass | C220002.023 | 8,900–12,000 | 1000–1800 | 0.2–0.4 | #800 / #1200 | 8,900–12,000 | 800–1600 | 0.05–0.2 | #1200 → #2000 | Air / Wet |
| N | Copper alloys | — | Electrolytic copper | C630002.0966 | 7,000–12,000 | 1000–1800 | 0.2–0.4 | #800 / #1200 | 6,400–12,000 | 800–1600 | 0.05–0.2 | #1200 → #2000 | Air / Wet |
| N | Non metallic | Duroplastics, fiber plastics | — | Bakelite— | 5,100–12,000 | 800–1600 | 0.1–0.3 | #2000 / #3000 | 5,100–10,200 | 600–1400 | 0.05–0.15 | #3000 → #6000 | Dry air + extraction |
| N | Non metallic | Hard rubber | — | Ebonite— | 3,800–11,500 | 800–1600 | 0.1–0.3 | #2000 / #3000 | 3,800–7,600 | 600–1400 | 0.05–0.15 | #3000 → #6000 | Dry air + extraction |
| S | High temperature alloys | Fe based | Annealed | 3301.4864 | 2,500–6,000 | 600–1200 | 0.1–0.3 | #150 / #200 / #400 | 5,100–10,200 | 500–1000 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Fe based | Hardened | S5901.4977 | 2,200–5,100 | 600–1200 | 0.1–0.3 | #150 / #200 / #400 | 3,800–7,600 | 500–1000 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Ni or Co based | Annealed | Incoloy 8252.4858 | 1,900–4,500 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 2,200–4,100 | 350–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Ni or Co based | Hardened | Inconel 7182.4668 | 1,600–3,500 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 1,900–3,500 | 350–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | High temperature alloys | Ni or Co based | Cast | Nimocast K242.4674 | 1,600–3,800 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 1,900–3,800 | 350–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | Titanium alloys | — | Pure | Titanium G.13.7024 | 2,200–5,100 | 500–1000 | 0.1–0.3 | #150 / #200 / #400 | 2,200–4,500 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| S | Titanium alloys | — | Alpha+beta alloys, hardened | Titanium G.53.7165 | 1,900–4,100 | 500–1000 | 0.1–0.3 | #150 / #200 / #400 | 1,900–3,800 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet recommended |
| H | Hardened steel | — | Hardened | HARDOX 500— | 2,200–5,100 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 12,000 max. | 300–700 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| H | Hardened steel | — | Hardened | HARDOX Extreme— | 1,900–3,800 | 400–900 | 0.1–0.3 | #150 / #200 / #400 | 9,500–12,000 | 300–700 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| H | Chilled cast iron | — | Cast | A532 IIIA 25% Cr0.965 | 2,500–5,100 | 500–1000 | 0.15–0.3 | #150 / #200 / #400 | 6,400–11,500 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
| H | Hardened cast iron | — | Hardened | A532 IID 20% CrMo0.9645 | 2,200–4,500 | 500–1000 | 0.15–0.3 | #150 / #200 / #400 | 5,100–9,500 | 400–800 | 0.05–0.15 | #400 → #800 #1000 / #1200 final |
Wet preferred |
Controlling Deburring & Polishing Performance
Increase Deburring Action
Coarser grit → More engagement → Lower feed → Additional controlled pass
Reduce Aggressiveness
Finer grit → Lighter engagement → Higher feed → Fewer passes
Improve Surface Finish
Finer grit sequence → Light contact → Stable feed → Finishing passes
Improve Brush Life
Reduce pressure → Correct alignment → Avoid side load → Minimum required engagement
End Brush Installation & Usage
01. Shank Grip
Grip the brush shank by at least 20 mm to ensure secure clamping.
02. Chuck Matching
Use a chuck or collet that correctly matches the brush shank diameter.
03. Minimize Runout
Keep spindle and tool runout as low as practical for stable brush contact.
04. Initial Engagement
Start with minimum contact and increase engagement gradually only when required.
05. Secure Workholding
Ensure the brush and workpiece are securely clamped before CNC operation.
06. Validate the Process
Confirm the parameters on the actual component before production use.
Manual & CNC Operating Speed Guidelines
Manual Operation
1,000 → 3,000 RPM
Start at approximately 1,000 RPM. Once stable control is established, increase gradually up to 3,000 RPM.
Automated Operation
Up to 12,000 RPM
Follow the RPM values specified in the machining recommendation table. Never exceed 12,000 RPM.
Correct Brush Contact
Use light axial contact for localized deburring, edge finishing and polishing.
For the 45° End Type, keep engagement light and use the formed tip to reach chamfers, corners and recesses.
Do not force the ceramic fibers strongly sideways against an edge. Excessive bending can reduce stability and accelerate wear.
End Brush Troubleshooting
| Problem | Recommended Adjustment |
|---|---|
| Burr remains | Use a coarser grit → slightly increase engagement → reduce feed → add another controlled pass. |
| Excessive edge rounding | Increase feed → reduce brush engagement → select a finer grit → reduce RPM if necessary. |
| Brush marks | Use a finer grit → reduce engagement → maintain stable movement → add a light finishing pass. |
| Excessive brush wear | Reduce engagement → check alignment → minimize side loading → verify runout and clamping. |
| Poor surface finish | Use a progressive grit sequence → reduce final engagement → maintain stable feed → check brush cleanliness. |
| Vibration / unstable contact | Stop operation → check chuck, runout, brush condition and workholding before restarting. |
Brush Wear & Maintenance
Brush Wear Changes Cutting Behavior
As the ceramic fibers wear and become shorter, stiffness and contact behavior may change. Re-check the process when the brush has visibly shortened.
Compensate Gradually
If the process becomes too aggressive, reduce engagement, increase feed, reduce RPM if required, or select a finer grit.
Keep the Brush Clean
Remove accumulated machining debris, dust and coolant residue. Contamination can reduce cutting consistency and surface-finish quality.
Inspect Before Production
Check the brush tip, shank, clamping condition and runout before use. Replace a damaged or unstable brush before production machining.
End Brush Safety Precautions & Instructions
Operation Safety
• Do not exceed the specified maximum spindle speed.
• Do not use pneumatic-powered hand tools.
• Stop immediately if abnormal vibration occurs.
• Avoid prolonged machining at one fixed point.
• Ensure secure tool and workpiece clamping.
Operator & Work Area Safety
• Wear suitable eye protection.
• Use respiratory protection where required.
• Use suitable dust and particle extraction.
• Keep flammable materials away from the machining area.
• Do not touch hot surfaces immediately after machining.