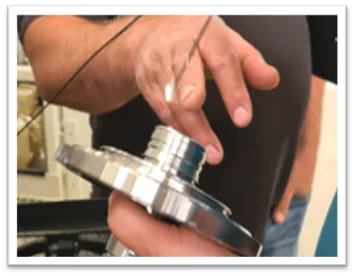
Transmission Shaft Deburring in the Automotive Industry.
Automate front and rear burr removal on transmission shaft pilot holes with UBURR™ internal deburring tools. In a head-to-head trial in AISI 4340 steel, UBURR HSS blades completed 210 holes at Ø2.5 mm and 1,300 holes at Ø3.0 mm, compared with 100 and 500 holes for a competitor's HSS blade. Tool life and surface finish were verified with an endoscope.
See the comparison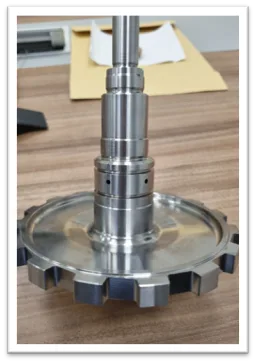 UB2500 · UB3000
- Pilot holes
- Ø2.5 / 3.0 mm
- Spindle speed
- 2,000 RPM
- Table feed
- 500 mm/min
- Tool life vs. competitor
- 2.6× max
A head-to-head tool-life test.
The task
Run comparison tests against a competitor for removing burrs from the front and rear of machined drill holes in an automotive transmission shaft.
- Part
- Transmission shaft
- Material
- AISI 4340 (W.Nr. 1.6928)
- Pilot holes
- Ø2.5 & Ø3.0 mm (0.098" & 0.118")
- Pilot hole length
- H1 = 35 mm (1.38")
- Production volume
- 45,000 bores/month
The trial
Two UBURR tool-holder sets, each matched to one pilot-hole diameter, ran at 2,000 RPM and 500 mm/min with external emulsion. Blade life was compared with a competitor's HSS blade on the same holes. Tool life and surface finish were checked with an endoscope.
Application photo
SUPPLIED PHOTO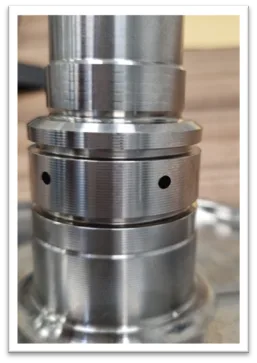
The tools behind
the result.
- Blade
- UB2022
- Blade code
- UB-TSB-2.5-PL-NCT
- Blade
- UB2032
- Blade code
- UBS-TSB-3.0-PL-NCT
| Parameter | Ø2.5 mm | Ø3.0 mm |
|---|---|---|
| Workpiece material | AISI 4340 | AISI 4340 |
| Pilot hole diameter | Ø2.5 mm (0.098") | Ø3.0 mm (0.118") |
| Pilot hole length | 35 mm (1.38") | 35 mm (1.38") |
| Spindle speed | 2,000 RPM | 2,000 RPM |
| Table feed | 500 mm/min (20 in/min) | 500 mm/min (20 in/min) |
| Cutting speed | 16 m/min (52 sfm) | 19 m/min (62 sfm) |
| Feed per tooth | 0.25 mm (0.01") | 0.25 mm (0.01") |
| Coolant | External emulsion | External emulsion |
These values describe this trial. Confirm the setup for your own application with NOGA MT.
Up to 2.6× the tool life.
| Parameter | NOGA UBURR | Competitor | Difference |
|---|---|---|---|
| Ø2.5 mm / 0.098" | 210 holes | 100 holes | 2.1× |
| Ø3.0 mm / 0.118" | 1,300 holes | 500 holes | 2.6× |
The customer was highly satisfied with the results, especially the longer tool life and the surface finish, both verified with an endoscope.
Result
AFTER UBURR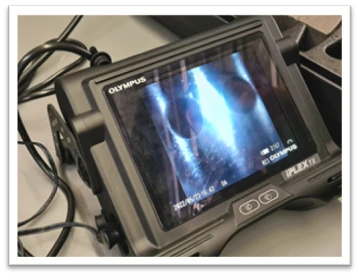
Result
AFTER UBURR