UBURR · CNC Application Case Study
Front & Rear Deburring of 60 HRC Tool Steel.
Put UBURR™ to the test on hardened material. In AISI H13 pallets hardened to 60 HRC, a UB1070 tool-holder with a T-coated UB2062 blade removed front and rear burrs from Ø7 mm holes at 700 RPM, leaving 0.2×45° chamfers with no significant wear after 50 holes.
See the trial result UB1070 · UB2062
- Hardness
- 60 HRC
- Spindle speed
- 700 RPM
- Table feed
- 140 mm/min
- Chamfer
- 0.2×45°
01 / The application
Deburring at 60 HRC.
The task
Test the UBURR tools on hardened material and eliminate burrs from the front and rear of machined drill holes.
Application details
- Industry
- General
- Material
- AISI H13 (W.Nr. 1.2344) pallets, 60 HRC
- Pilot hole
- Ø7 mm (0.276")
- Pilot hole length
- H1 = 25 mm (0.984")
- Machine
- DMG Mori Seiki AKIRA Mi745
02 / Tool & parameters
The tool behind
The tool behind
the result.
UBURR tool-holder
UB1070
UB-d070-C08-H53-L115
- Pilot hole
- Ø7 mm
- Blade
- UB2062
UBURR blade · T-type coating
UB2062
UB-TSB-5-PL-NCT
- Coating
- Type T
| Workpiece material | AISI H13, 60 HRC |
|---|---|
| Pilot hole diameter | Ø7.0 mm (0.276") |
| Pilot hole length | 25 mm (0.984") |
| Machine | DMG Mori Seiki AKIRA Mi745 |
| Spindle speed | 700 RPM |
| Table feed | 140 mm/min (5.5 in/min) |
| Cutting speed | 15 m/min (49 sfm) |
| Feed per tooth | 0.2 mm (0.008") |
| Coolant | External air |
| Reported result | 0.2×45° chamfers, no significant wear after 50 holes |
These values describe this trial. Confirm the setup for your own application with NOGA MT.
03 / Before & after
No significant wear after 50 holes
Hardened steel, clean edges.
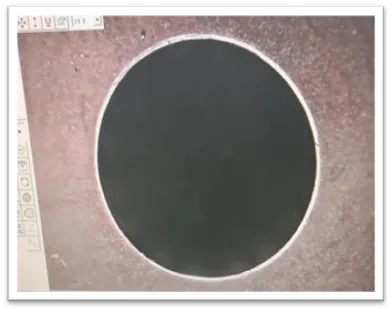
Before UBURR
DRILLED HOLE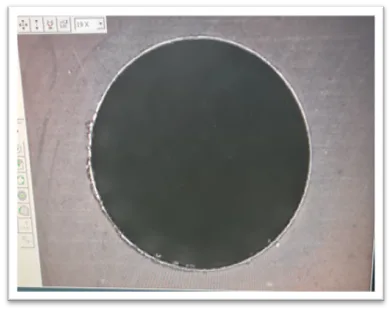
After UBURR
RESULT