
UBURR · CNC Application Case Study
Dual-Sided Thread Deburring in 38 HRC Hardened Steel.
Remove front and rear burrs from machined threads in one automated pass. In AISI 4340 tool steel hardened to 38 HRC, a UBURR™ UB1085 tool-holder with a UB2060 blade deburred Ø8.5 mm threaded holes at 800 RPM, leaving clean 0.2×45° chamfers with no significant blade wear after 50 holes.
See the trial result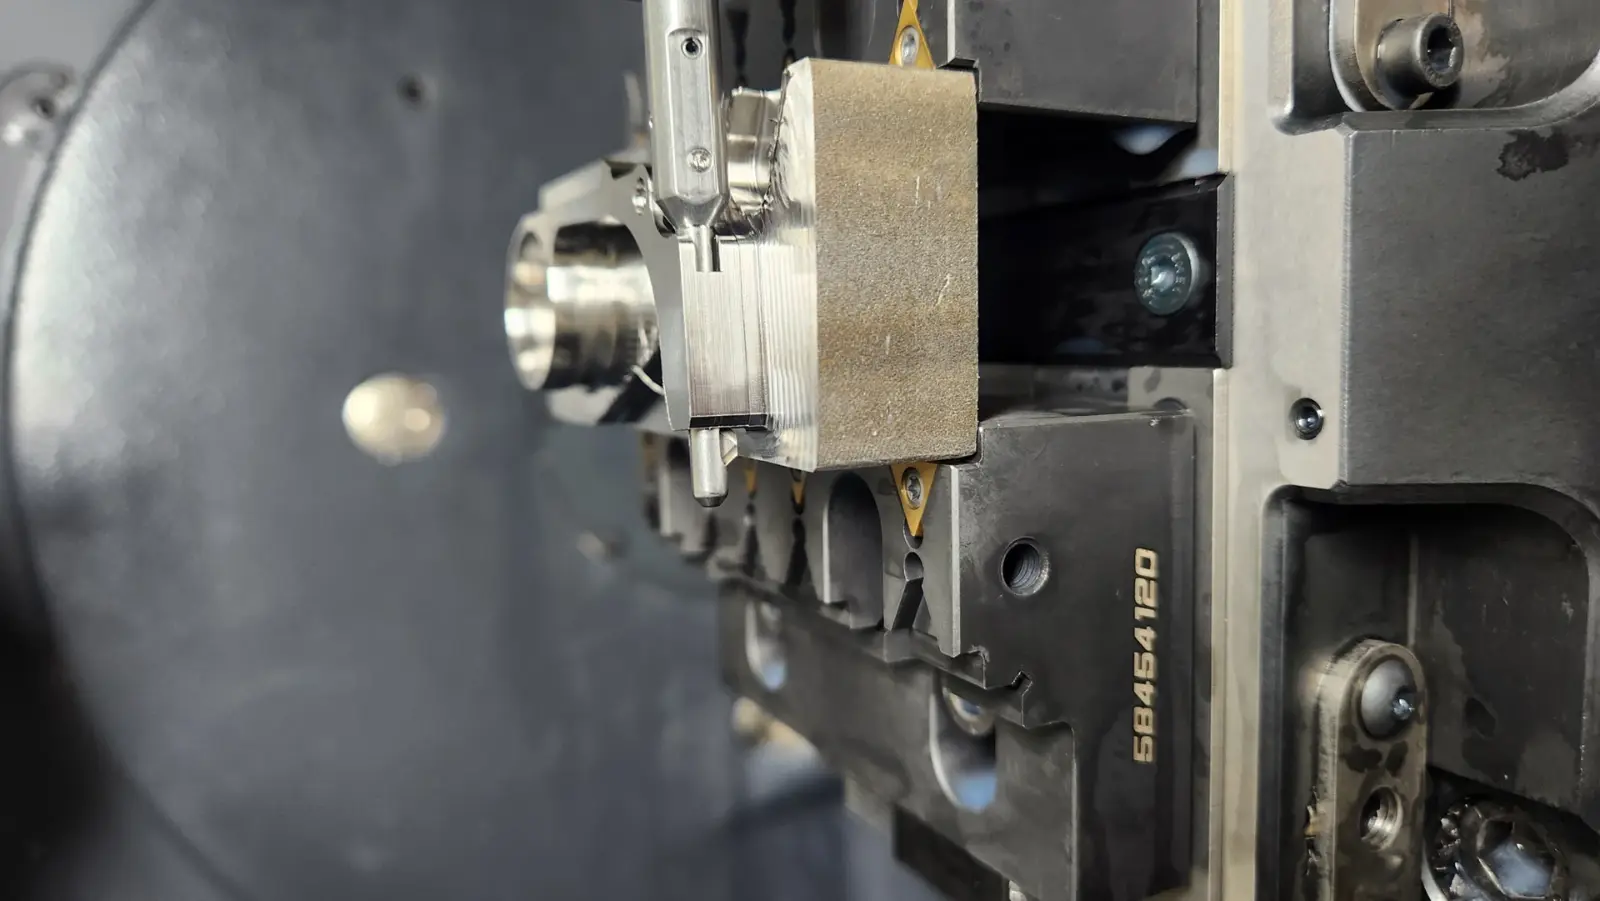 UB1085 · UB2060
- Tool-holder
- UB1085
- Spindle speed
- 800 RPM
- Table feed
- 200 mm/min
- Chamfer
- 0.2×45°
01 / The application
Burrs on both sides of a thread.
The task
Evaluate the UBURR tools on machined threads and eliminate burrs from both the front and rear of the drilled holes.
Application details
- Industry
- General
- Material
- AISI 4340 (W.Nr. 1.6928) tool steel, 38 HRC
- Pilot hole
- Ø8.5 mm (0.335")
- Pilot hole length
- H1 = 20 mm (0.787")
- Machine
- DMG Mori Seiki AKIRA Mi745
Part – top side
SUPPLIED PHOTO
02 / Tool & parameters
The tool behind
The tool behind
the result.
UBURR tool-holder
UB1085
UB-d085-C10-H53-L115
- Pilot hole
- Ø8.5 mm
- Blade
- UB2060
UBURR blade
UB2060
UB-TSB-5-PL
| Workpiece material | AISI 4340, 38 HRC |
|---|---|
| Pilot hole diameter | Ø8.5 mm (0.335") |
| Pilot hole length | 20 mm (0.787") |
| Machine | DMG Mori Seiki AKIRA Mi745 |
| Spindle speed | 800 RPM |
| Table feed | 200 mm/min (8 in/min) |
| Cutting speed | 22 m/min (72 sfm) |
| Feed per tooth | 0.25 mm (0.01") |
| Coolant | External air |
| Reported result | 0.2×45° chamfers, no significant wear after 50 holes |
These values describe this trial. Confirm the setup for your own application with NOGA MT.
03 / Before & after
No significant wear after 50 holes
Clean chamfers on both sides.
Top (front) side
Before UBURR
TOP SIDE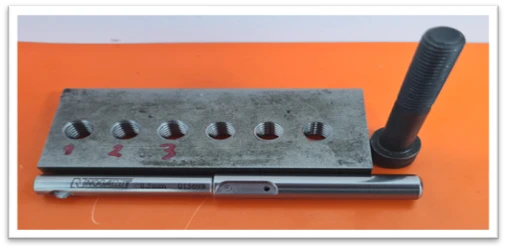
After UBURR
TOP SIDE
Bottom (rear) side
Before UBURR
BOTTOM SIDE
After UBURR
BOTTOM SIDE