UBURR · CNC Application Case Study
Back Deburring of Clamping Screw Bores in Cutting Tool Manufacturing.
Remove rear burrs from clamping screw bores automatically, inside the CNC cycle. For a cutting tool manufacturer, a UBURR™ UB1050 tool-holder with a UB2060 blade deburred the back of Ø5 mm bores in AISI 4340 hardened to 45 HRC, running on a Hermle C50 at 2,500 RPM and 250 mm/min.
See the application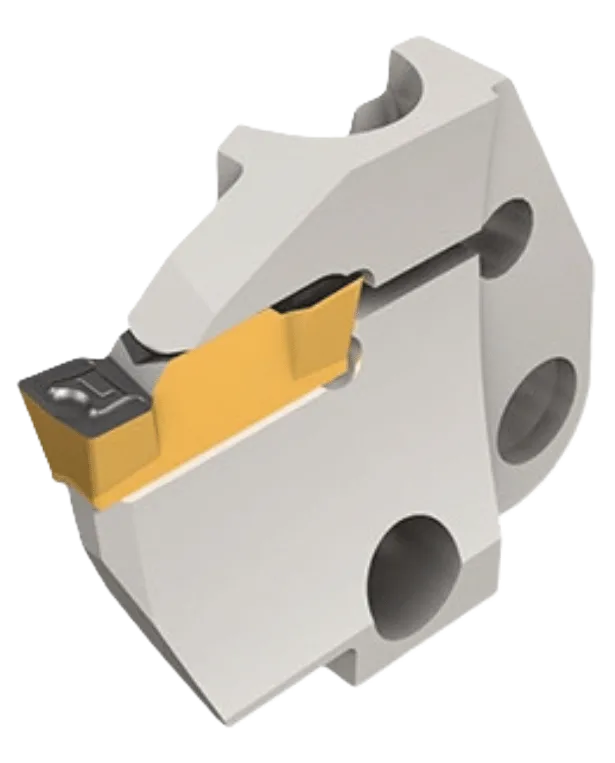 UB1050 · UB2060
- Tool-holder
- UB1050
- Spindle speed
- 2,500 RPM
- Table feed
- 250 mm/min
- Feed per tooth
- 0.10 mm
01 / The application
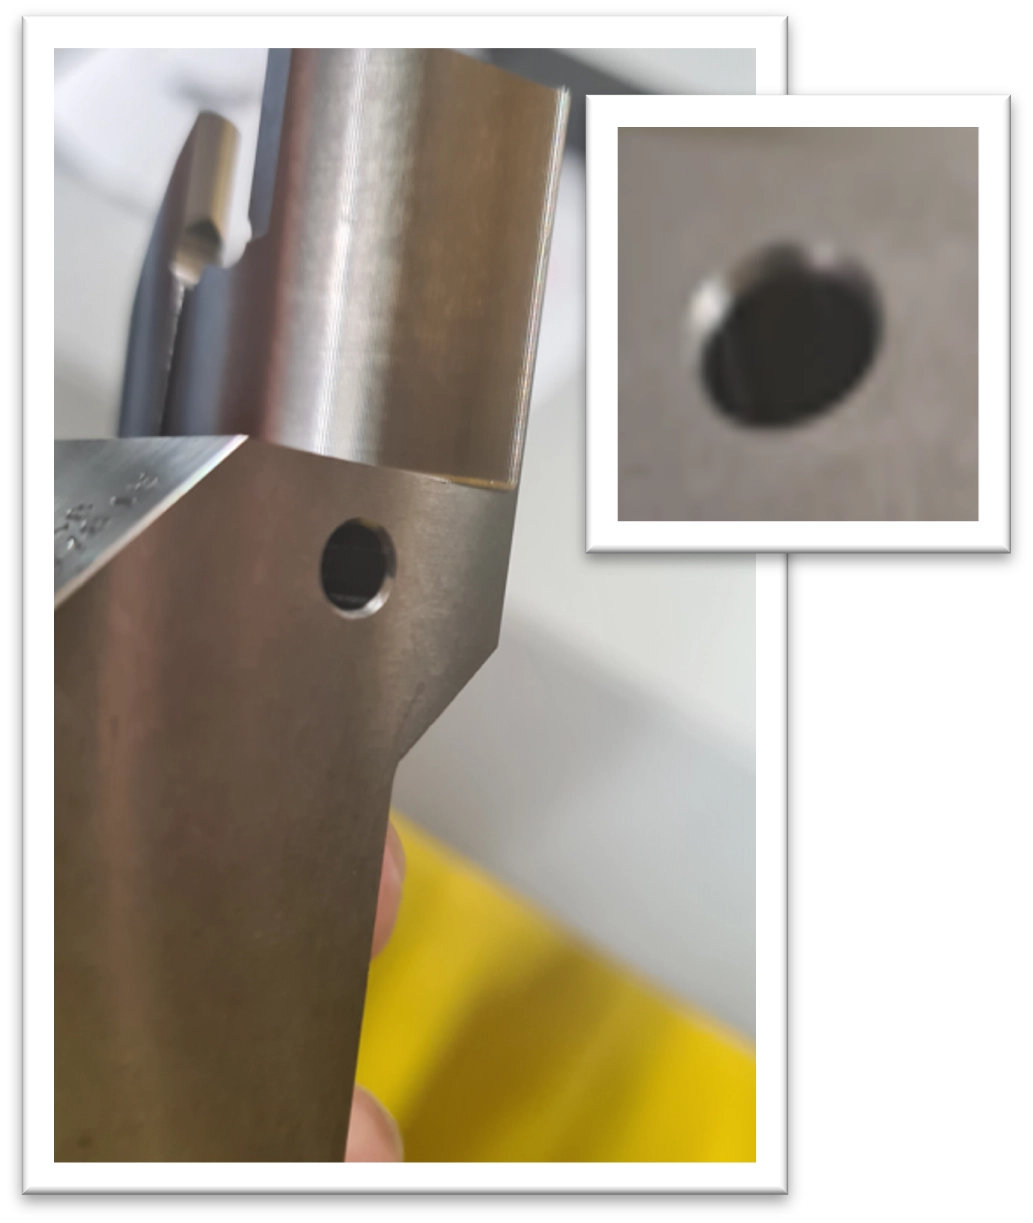
Burrs at the back of a 50 mm bore.
The task
Remove burrs from the rear of machined drill holes made for clamping screws, without manual deburring after machining.
Application details
- Industry
- Cutting tool manufacturing
- Material
- AISI 4340 (W.Nr. 1.6928), 45 HRC
- Pilot hole
- Ø5 mm (0.197")
- Pilot hole length
- H1 = 50 mm (1.97")
- Machine
- Hermle C50
- Production volume
- 5,000 bores/month for one tool family
02 / Tool & parameters
The tool behind
The tool behind
the result.
UBURR tool-holder
UB1050
UB-d050-C08-H53-L115
- Pilot hole
- Ø5 mm
- Blade
- UB2060
UBURR blade
UB2060
UB-TSB-5-PL
| Workpiece material | AISI 4340, 45 HRC |
|---|---|
| Pilot hole diameter | Ø5.0 mm (0.197") |
| Pilot hole length | 50 mm (1.97") |
| Machine | Hermle C50 |
| Spindle speed | 2,500 RPM |
| Table feed | 250 mm/min (10 in/min) |
| Cutting speed | 40 m/min (131 sfm) |
| Feed per tooth | 0.10 mm (0.004") |
| Coolant | External air |
These values describe this application. Confirm the setup for your own parts with NOGA MT.
03 / From the application
Back deburring, in the machine.
Bore exit on the part
MAGNIFIED INSET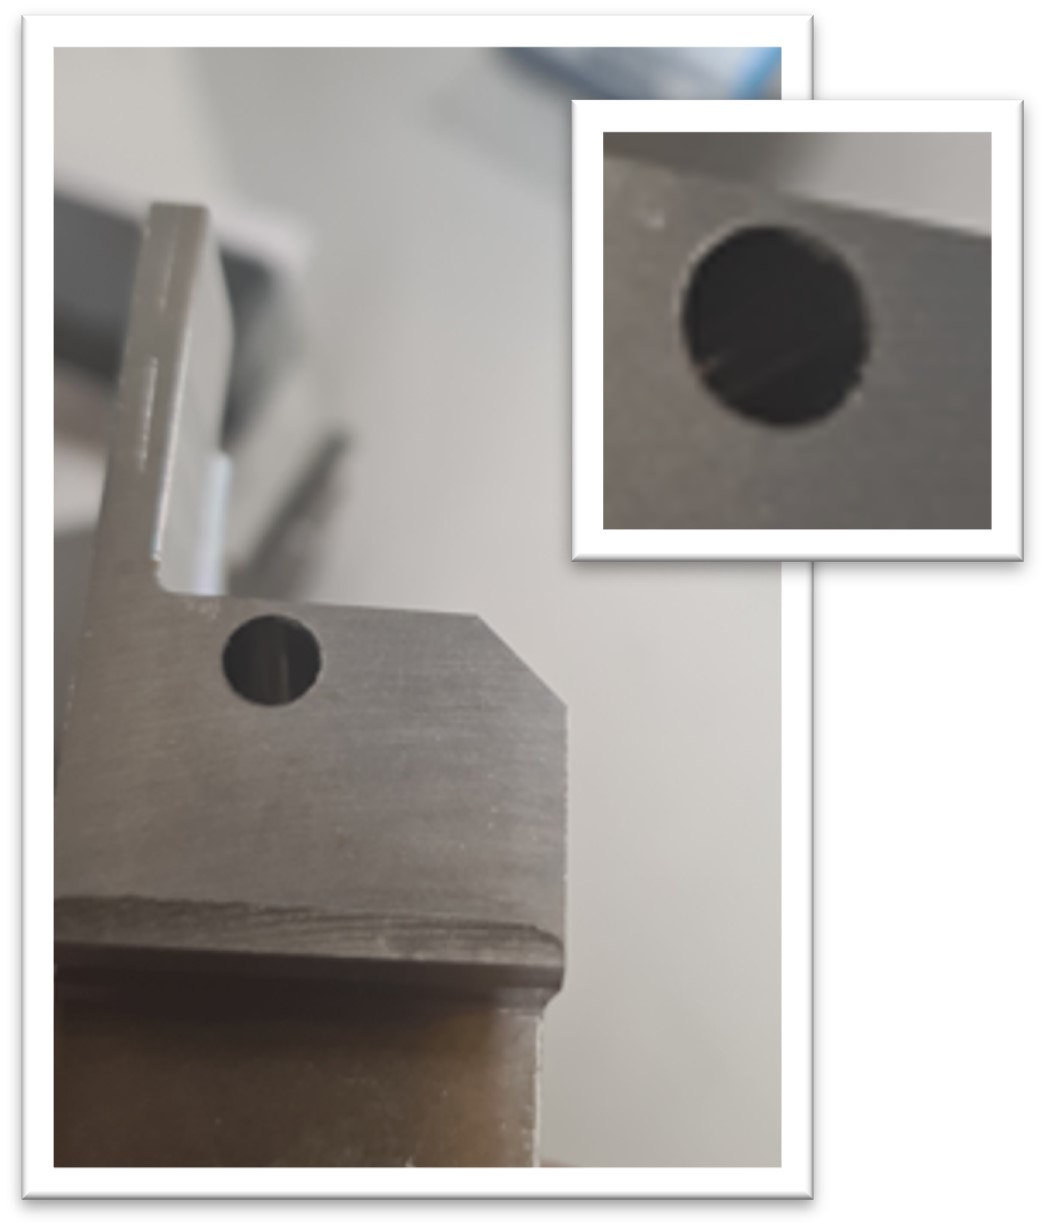
UBURR at the bore
MAGNIFIED INSET