UFIBER · CNC Application Case Study
Automated Cross-Hole Deburring of Aluminum Aerospace Components.
Eliminate manual deburring of cross-drilled manifold blocks. A UFIBER™ UF1715 Ø15 mm ceramic fiber brush, mounted on a tailor-made shank, reached cross-hole intersections 140 mm deep inside a Ø19.1 mm bore. Deburring time fell from 15 minutes to 60 seconds per part, a 93.33% reduction.
See the time savings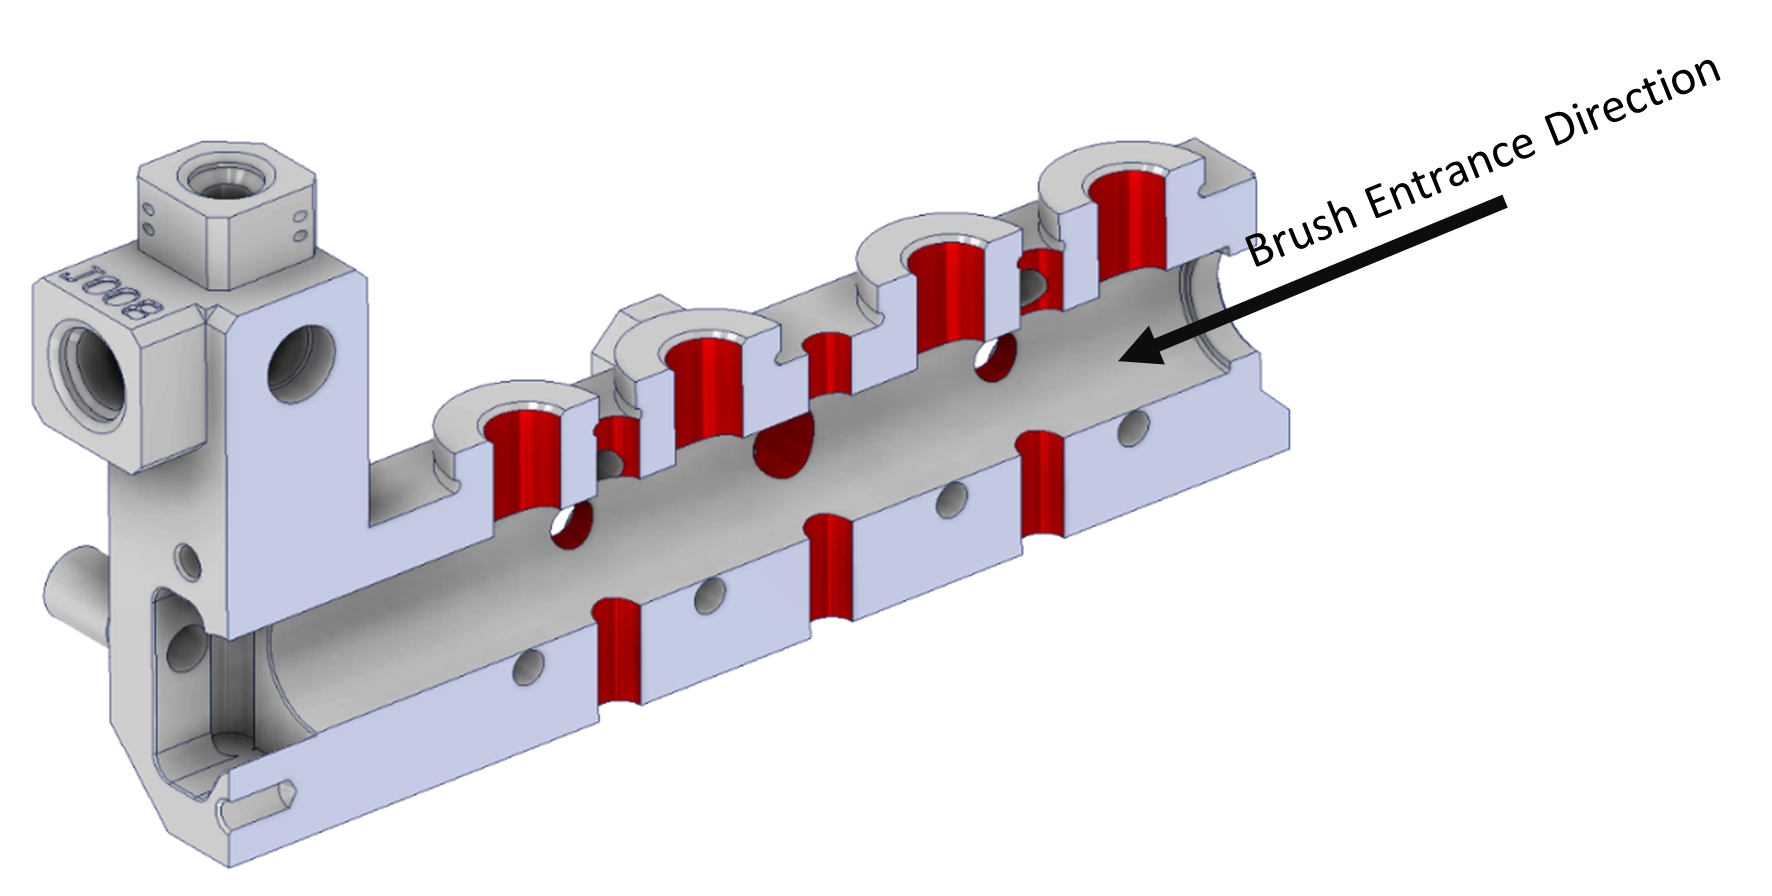 UF1715 · Ø15 mm · #1200
- Brush
- UF1715
- Spindle speed
- 7,000 RPM
- Table feed
- 500 mm/min
- Time reduction
- 93.33 %
01 / The application
Burrs deep inside a manifold.
The task
Eliminate burrs produced during cross-hole drilling on a CNC machine, removing the need for manual deburring. The solution used a UFIBER surface brush configured as a cross-hole brush on a tailor-made shank.
Application details
- Industry
- Aerospace
- Part
- Manifold block
- Material
- Aluminum 7075 (W.Nr. 3.4365)
- Pilot hole
- Ø19.1 mm (0.752")
- Pilot hole length
- 140 mm (5.512")
- Production volume
- 100 parts per batch
Application drawing
TECHNICAL DRAWING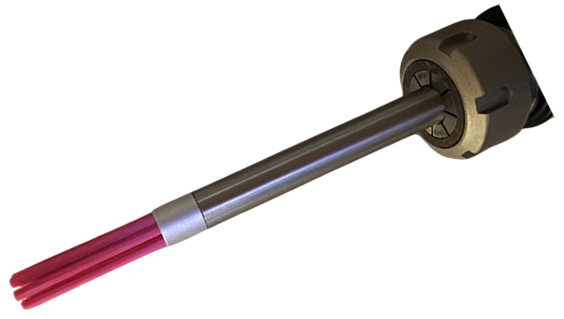
02 / Tool & parametersThe tool behind
The tool behind
the result.
UFIBER surface brush
UF1715
UF-FB-R-D015-L50
- Brush diameter
- Ø15 mm
- Grit
- #1200 Red
Tool-holder
Special
Designed and produced by the end-user
- Purpose
- Reach to 140 mm
- Mounting
- Tailor-made shank
| Workpiece material | Aluminum 7075 |
|---|---|
| Pilot hole diameter | Ø19.1 mm (0.752") |
| Machining depth | 140 mm (5.512") |
| Spindle speed | 7,000 RPM |
| Table feed | 500 mm/min (20 in/min) |
| Coolant | External emulsion |
| Reported result | 60 s per part, 93.33% time reduction |
These values describe this application. Confirm the setup for your own parts with NOGA MT.
Tool-holder
END-USER DESIGN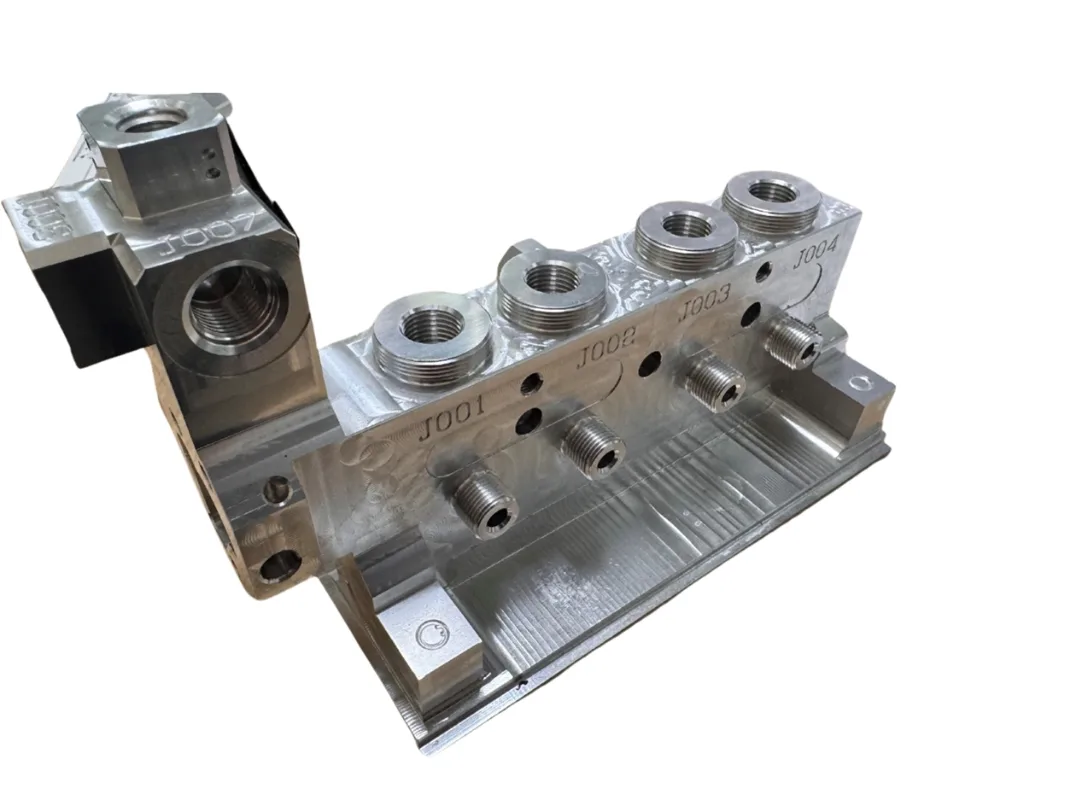
Tool-holder drawing
END-USER DESIGN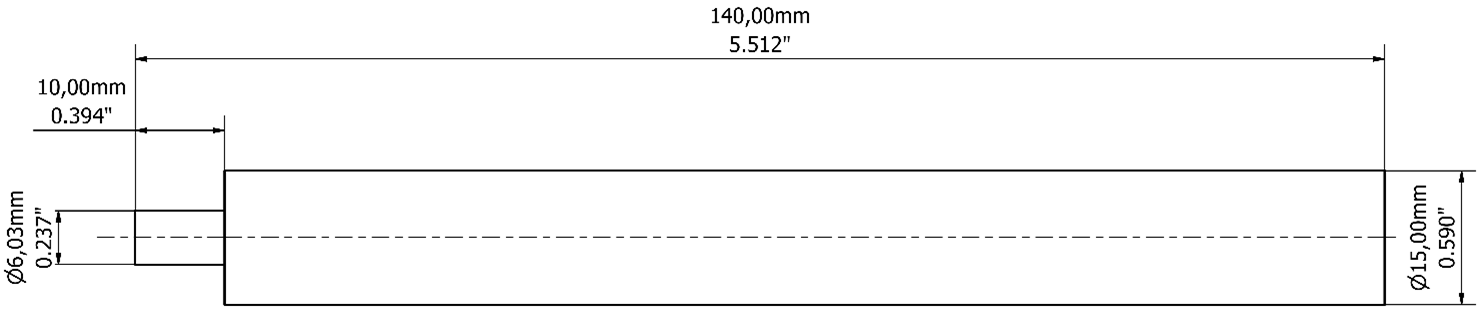
03 / Before & after
15× efficiency improvementFrom 15 minutes to 60 seconds.
900 → 60 sDeburring time per part
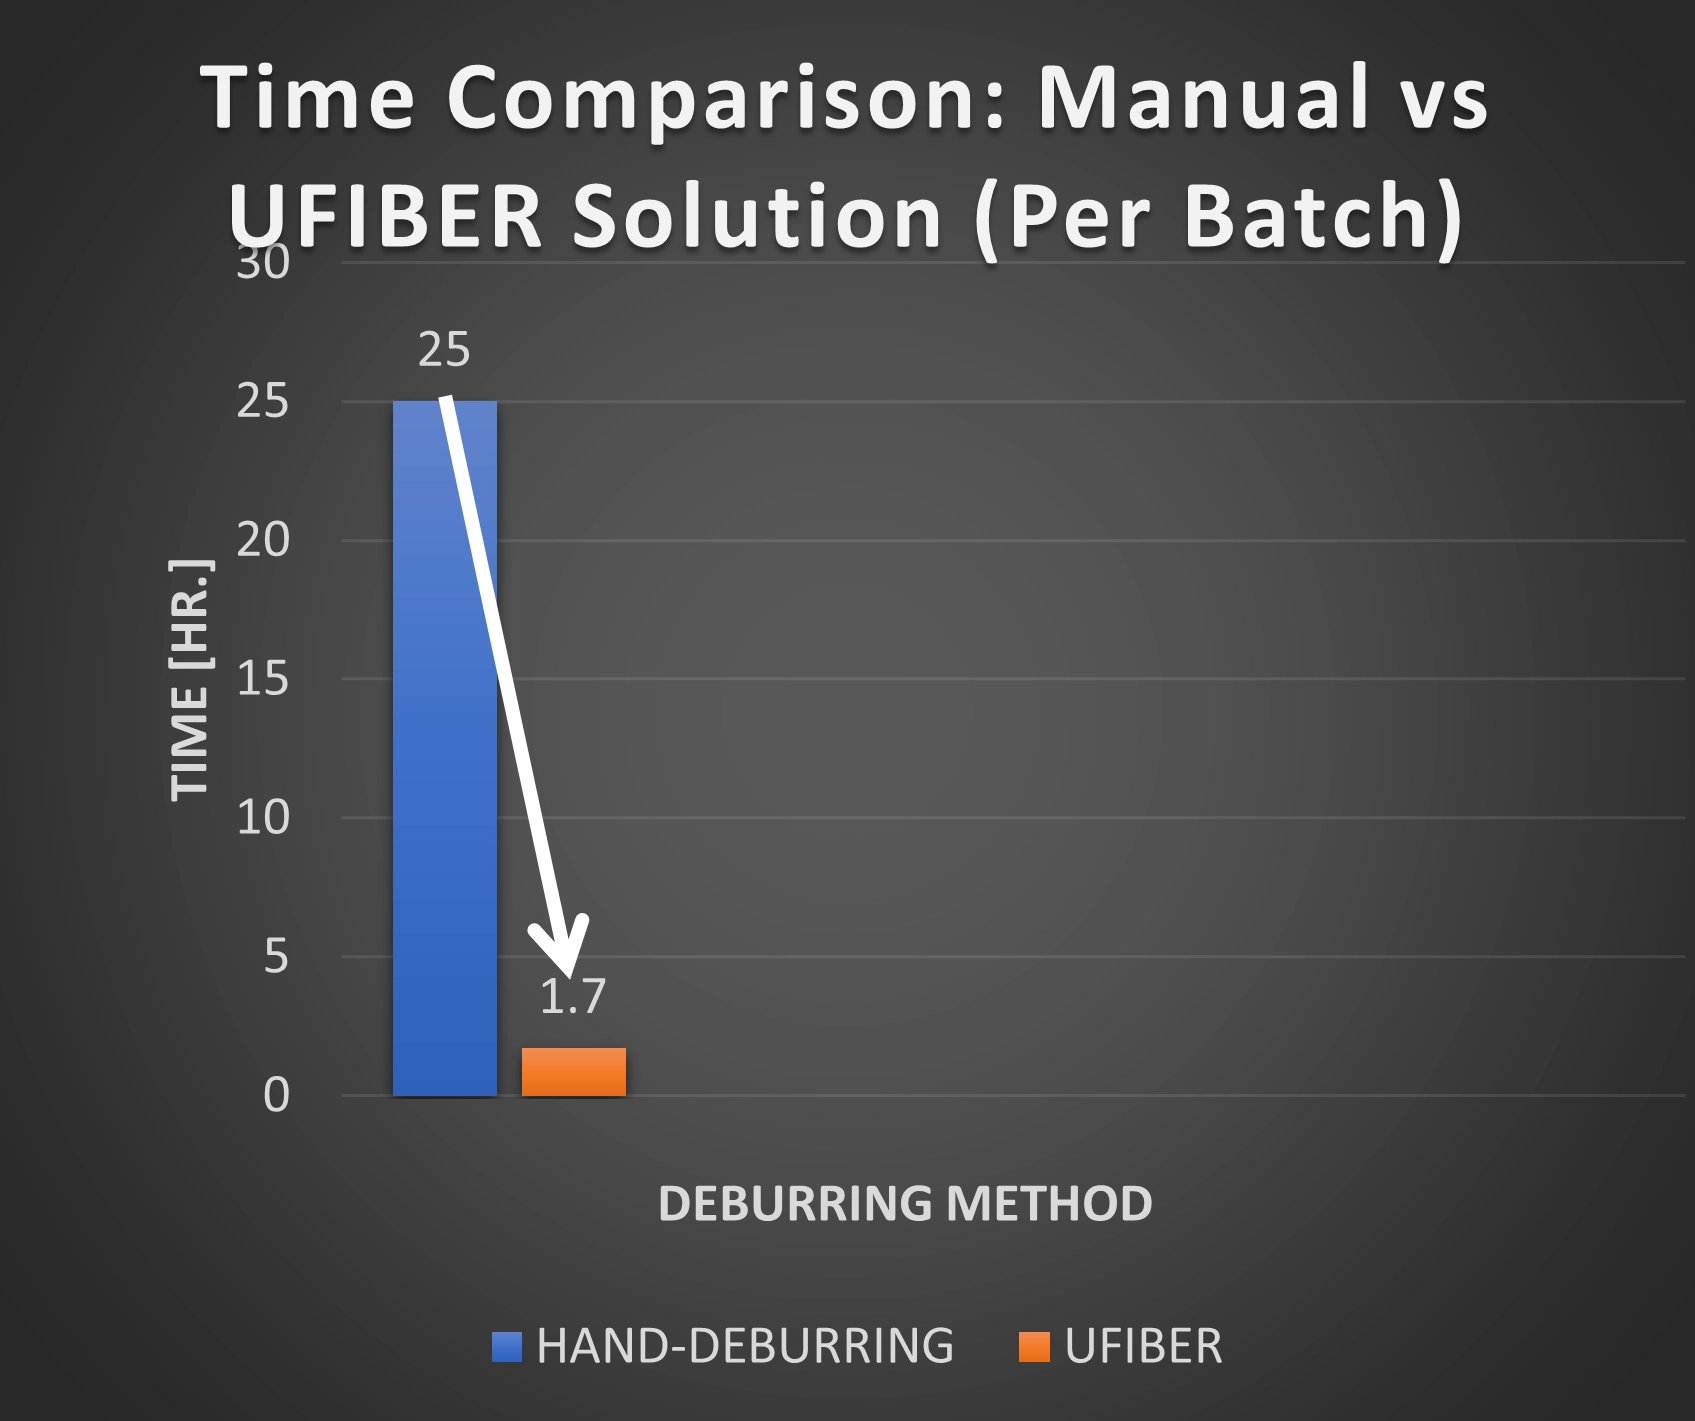
25 → 1.7 hPer 100-part batch
93.33%Time reduction
15×Efficiency improvement
Cross-hole intersection
Before UFIBER
CROSS-HOLE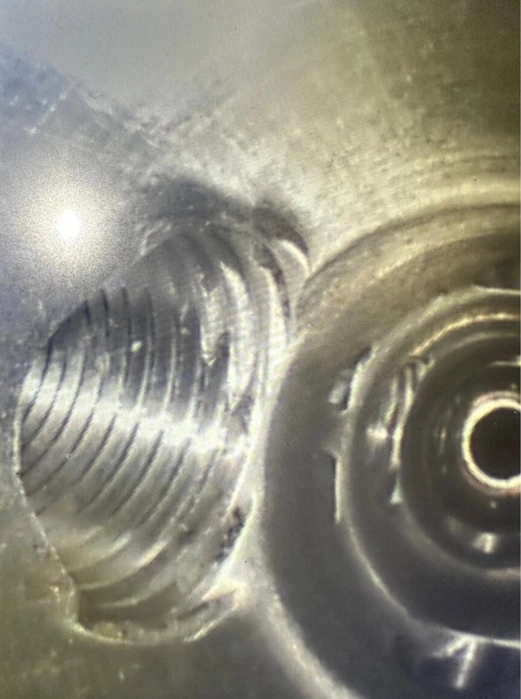
After UFIBER
CROSS-HOLE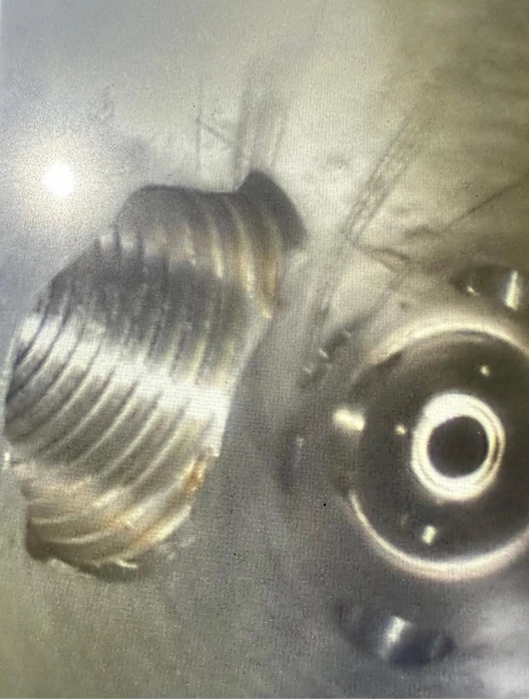
Close-up
Before UFIBER
MAGNIFIED VIEW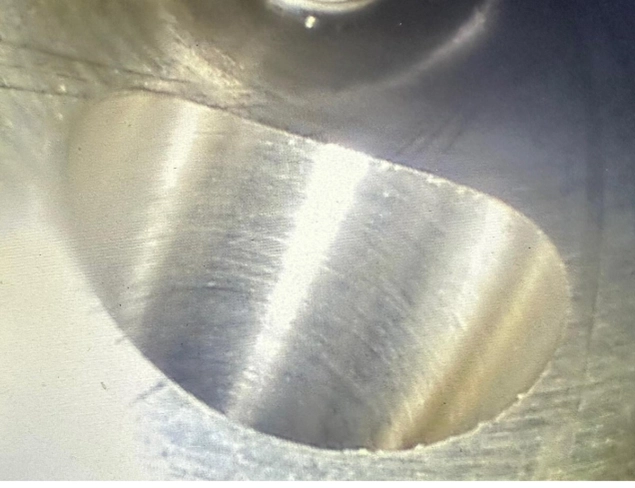
After UFIBER
MAGNIFIED VIEW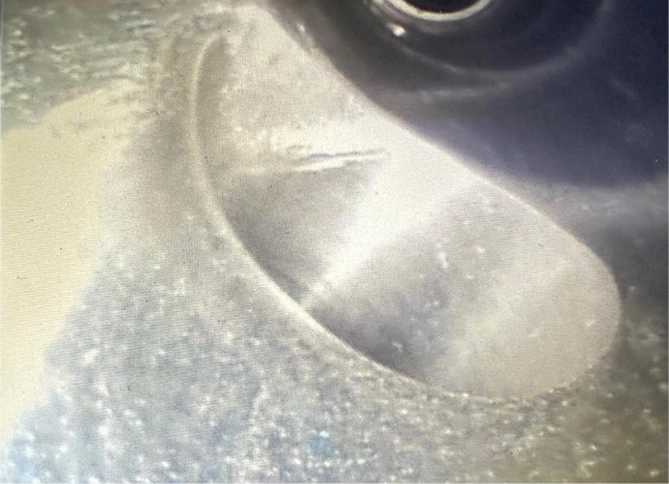
Time comparison
Time per part
CHART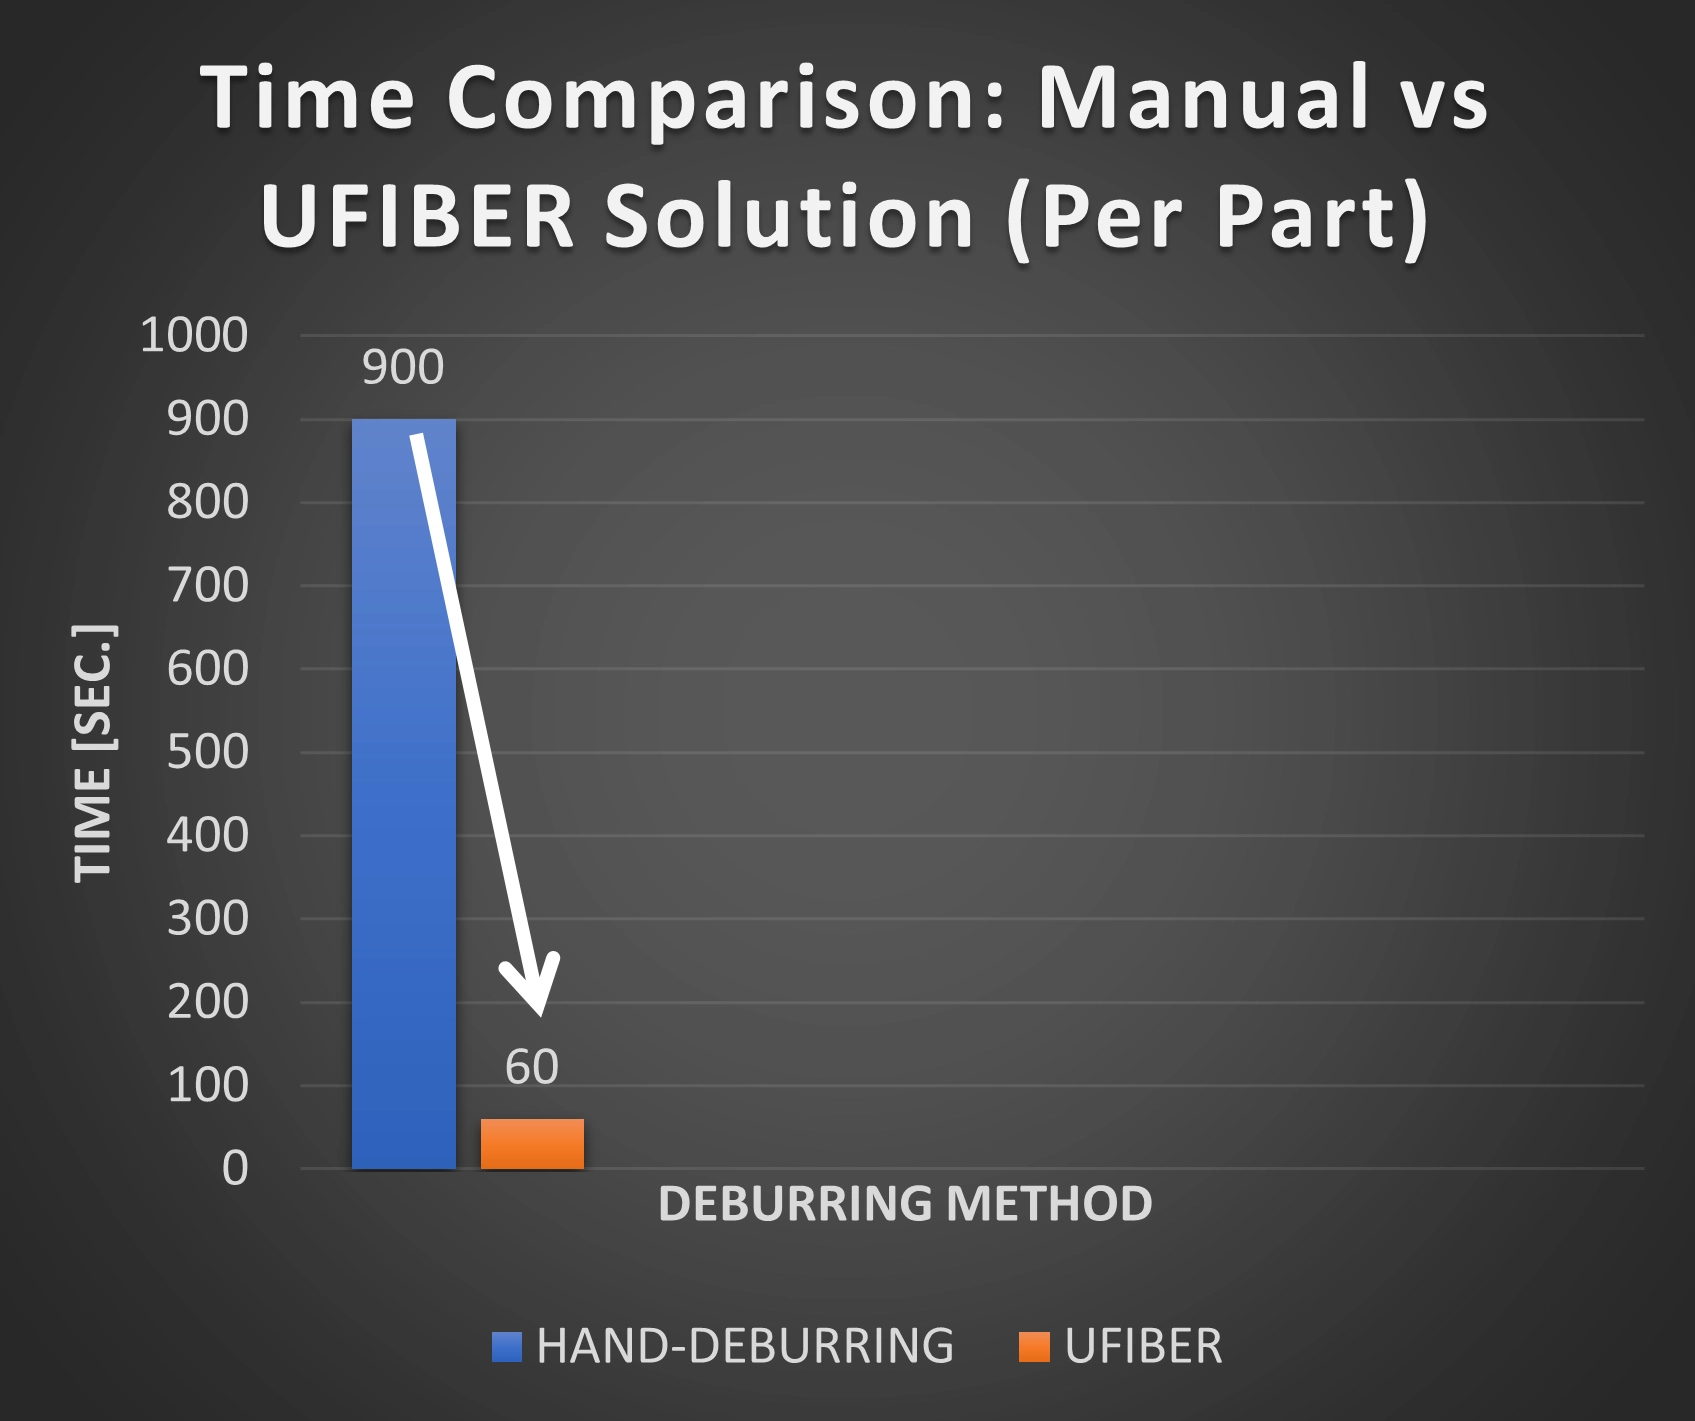
Time per batch
CHART