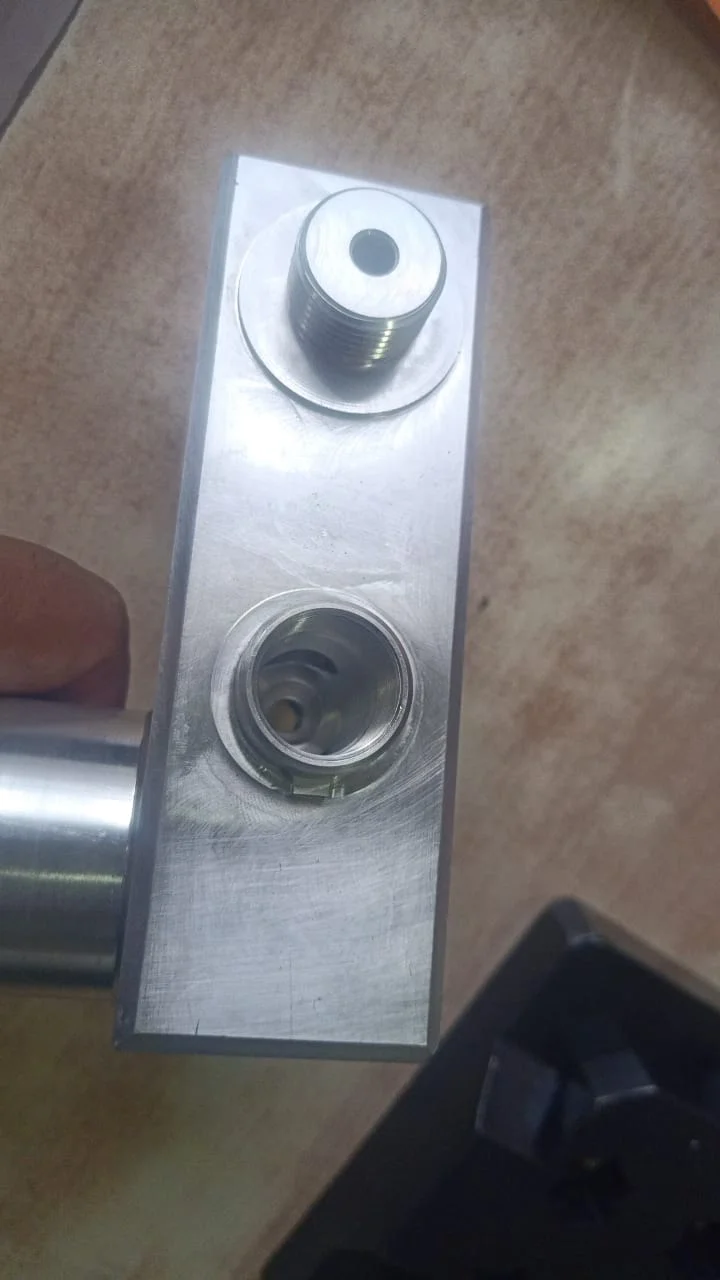
Automated Cross-Hole Deburring in Aluminum.
Achieve reliable internal burr removal with CNC-automated cross-hole deburring using UFIBER™ ceramic fiber brushes. In this successful application, a UF2670 Ø7 mm brush was used through a Ø12.4 mm entry bore to remove burrs at an internal cross-hole intersection. Running at 6,000 RPM and 480 mm/min, the process delivered consistent burr removal while reducing manual finishing and improving repeatability.
See the trial result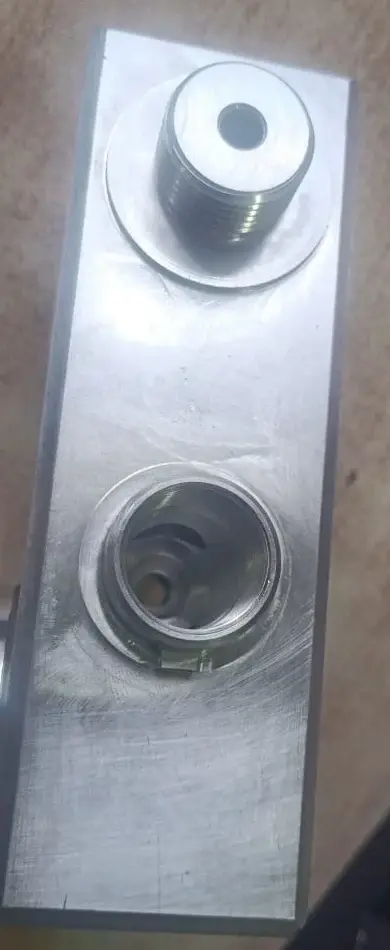 UF2670 · Ø7 mm · #1000
- Brush
- UF2670
- Spindle speed
- 6,000 RPM
- Feed rate
- 480 mm/min
- Feed per revolution
- 0.08 mm/rev
Reaching an internal intersection.
The task
Remove a burr at a cross-hole intersection in an aluminum component. The reported entry bore was Ø12.4 mm, with a machining depth of 68 mm.
The trial
The application was tested with a UFIBER UF2670 cross-hole brush at 6,000 RPM and 480 mm/min. The application report confirmed successful burr removal.
The tool behind
the result.
- Brush diameter
- Ø7 mm
- Grit
- #1000
| Workpiece material | Aluminum |
|---|---|
| Entry bore diameter | Ø12.4 mm |
| Machining depth | 68 mm |
| Spindle speed | 6,000 RPM |
| Feed rate | 480 mm/min |
| Feed per revolution | 0.08 mm/rev |
| Reported result | Successful burr removal |
These values describe this trial. Aluminum grade, cross-hole diameter, machine model and coolant were not specified in the report. Confirm the setup for your own application with NOGA MT.
Successful burr removal.
Before UFIBER
MAGNIFIED VIEW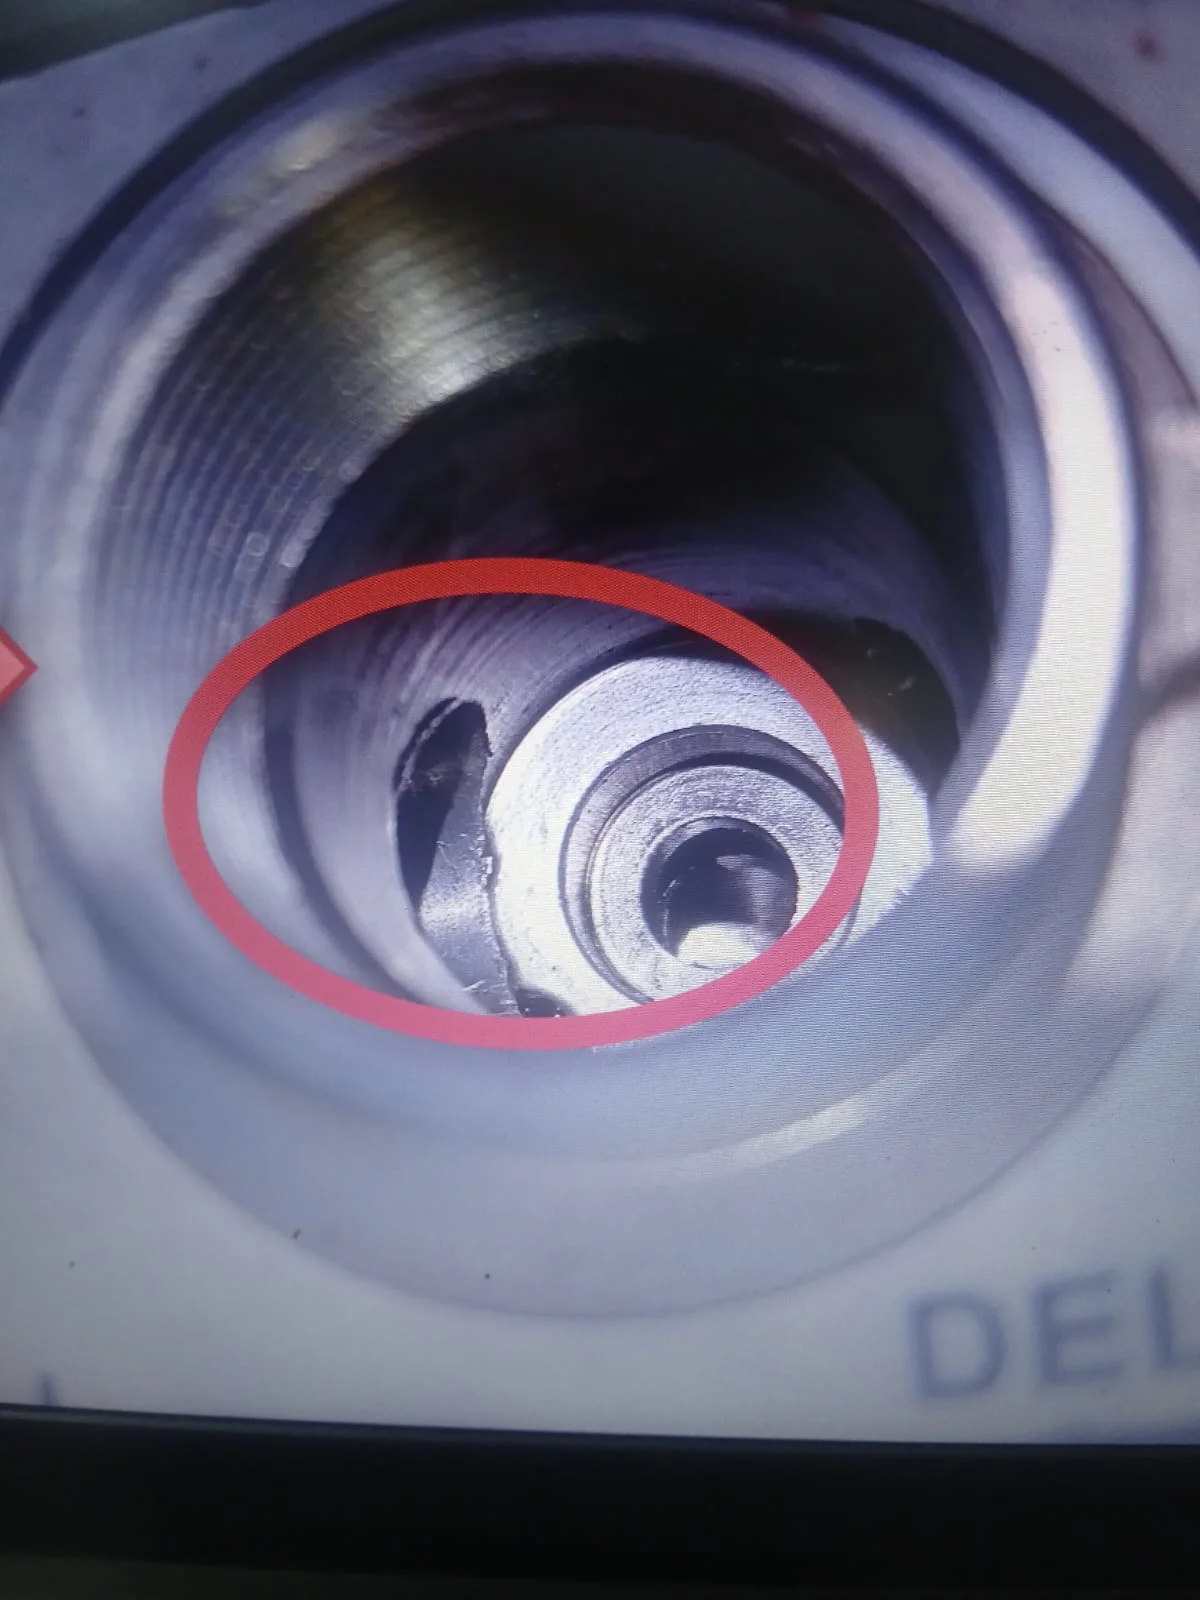
After UFIBER
DETAIL FROM AFTER PHOTO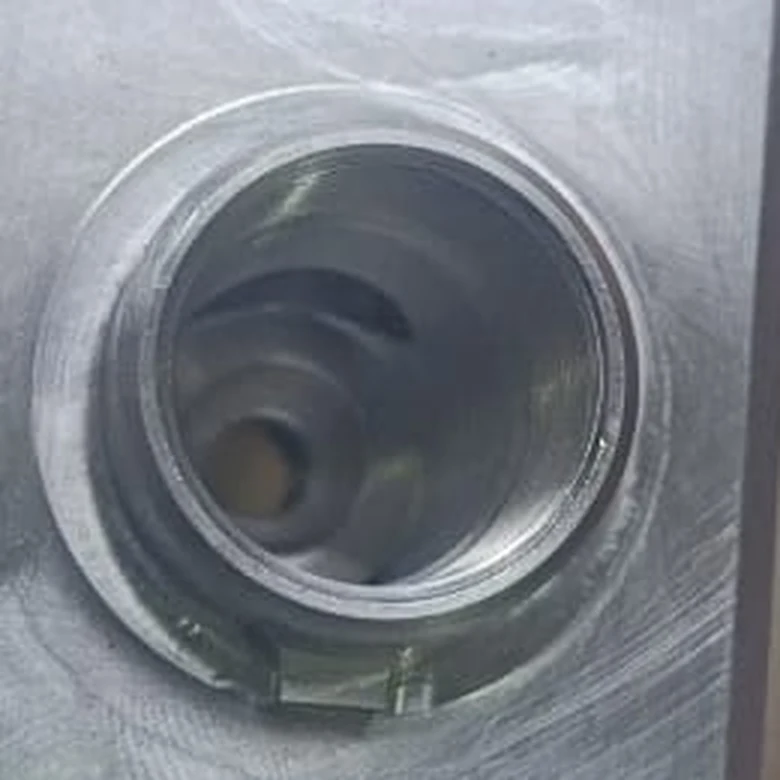
The after detail is rotated 90° counterclockwise to align the bore orientation with the before view. It is a crop of an overview photo; the photos use different viewing angles and magnification.
View the complete after photo