
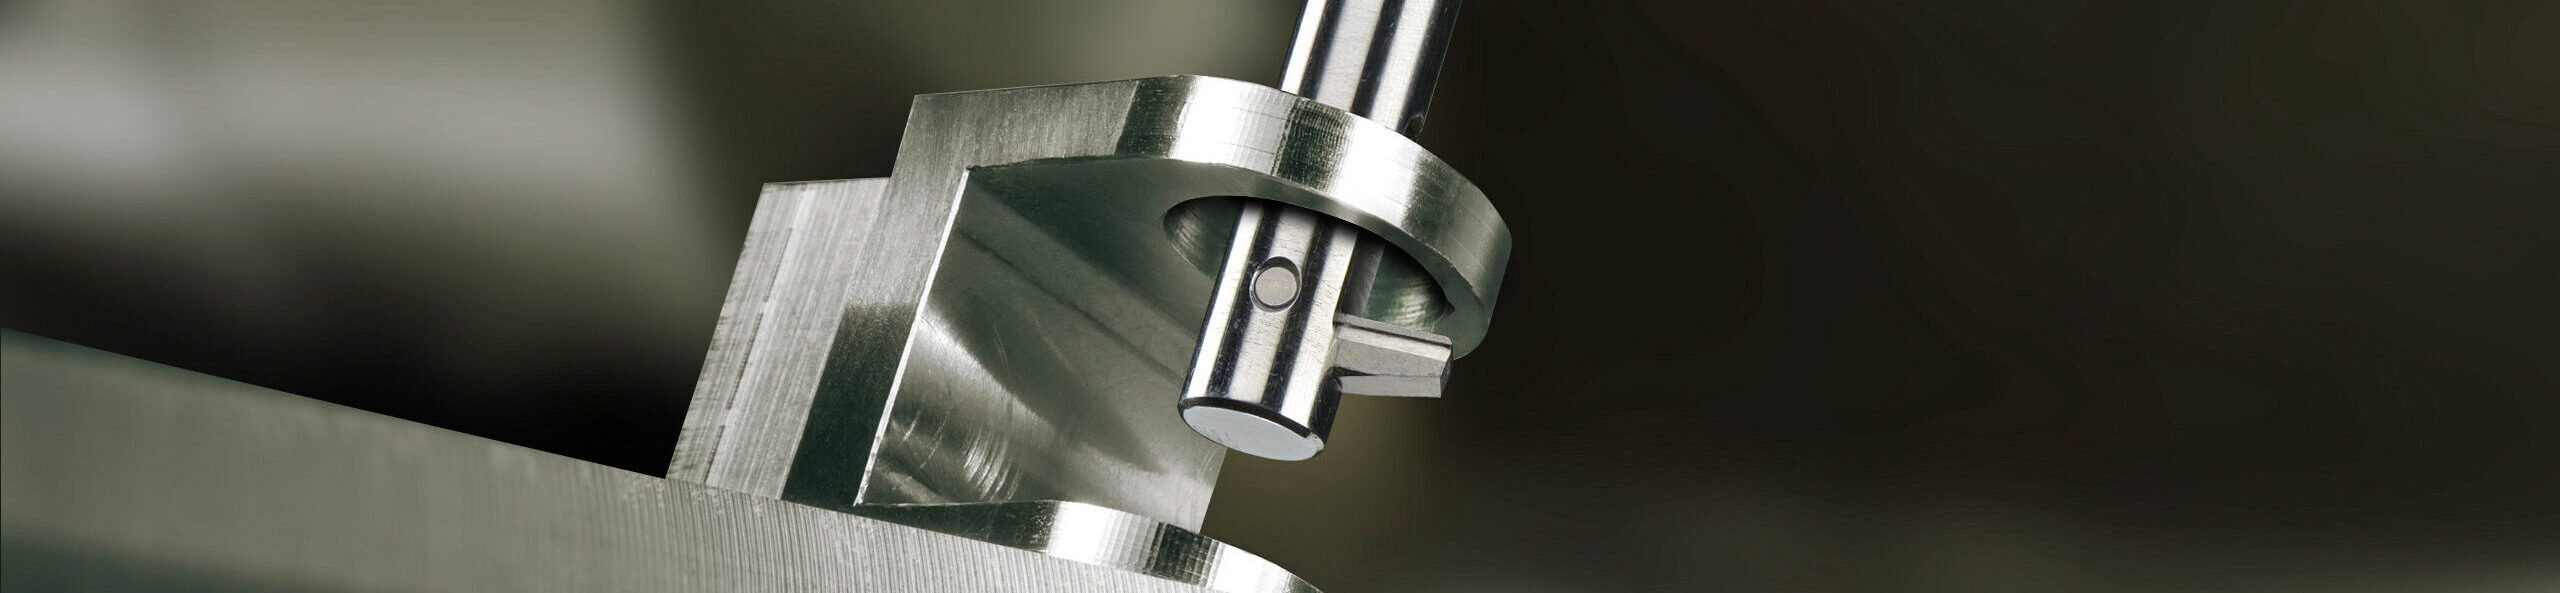
USPOT® Back Spotfacing & Counterboring Tool
Machine hidden rear faces through the existing pilot hole, without flipping the workpiece. A semi-standard insert, customized to your feature, on the coolant-actuated UBACK UX tool-holder.
USPOT / UX Series at a Glance
The range is organized into six series. Each series groups three nominal pilot-hole sizes and defines the matching holder family, RFC capacity and maximum supported USPOT counterbore diameter.
| Series | Pilot-Hole Rangemm / inch | USPOT ØDmax Range by Holdermm / inch | Standard UX Holders | RFCmm / inch |
|---|---|---|---|---|
| B | Ø8–10 mmØ0.3150–0.394″ | Ø18.5–23 mmØ0.728–0.906″ | UX2080 / UX2090 / UX2100 | 43 mm1.693″ |
| C | Ø11–13 mmØ0.433–0.512″ | Ø26–30 mmØ1.024–1.181″ | UX3110 / UX3120 / UX3130 | 52 mm2.047″ |
| D | Ø14–16 mmØ0.551–0.630″ | Ø32.5–37 mmØ1.280–1.457″ | UX4140 / UX4150 / UX4160 | 72.5 mm2.854″ |
| E | Ø17–19 mmØ0.669–0.748″ | Ø39.5–44 mmØ1.555–1.732″ | UX5170 / UX5180 / UX5190 | 76.5 mm3.012″ |
| F | Ø20–22 mmØ0.787–0.866″ | Ø46–50.5 mmØ1.811–1.988″ | UX6200 / UX6210 / UX6220 | 76.5 mm3.012″ |
| G | Ø23–25 mmØ0.906–0.984″ | Ø53–57.5 mmØ2.087–2.264″ | UX7230 / UX7240 / UX7250 | 72 mm2.835″ |
How to Select the Correct UX Holder and USPOT Insert
Keep the process simple: holder first, then the insert geometry, then compatibility checks.
Start with Pilot Ød
Select the UX holder whose nominal / supported pilot range fits your through hole.
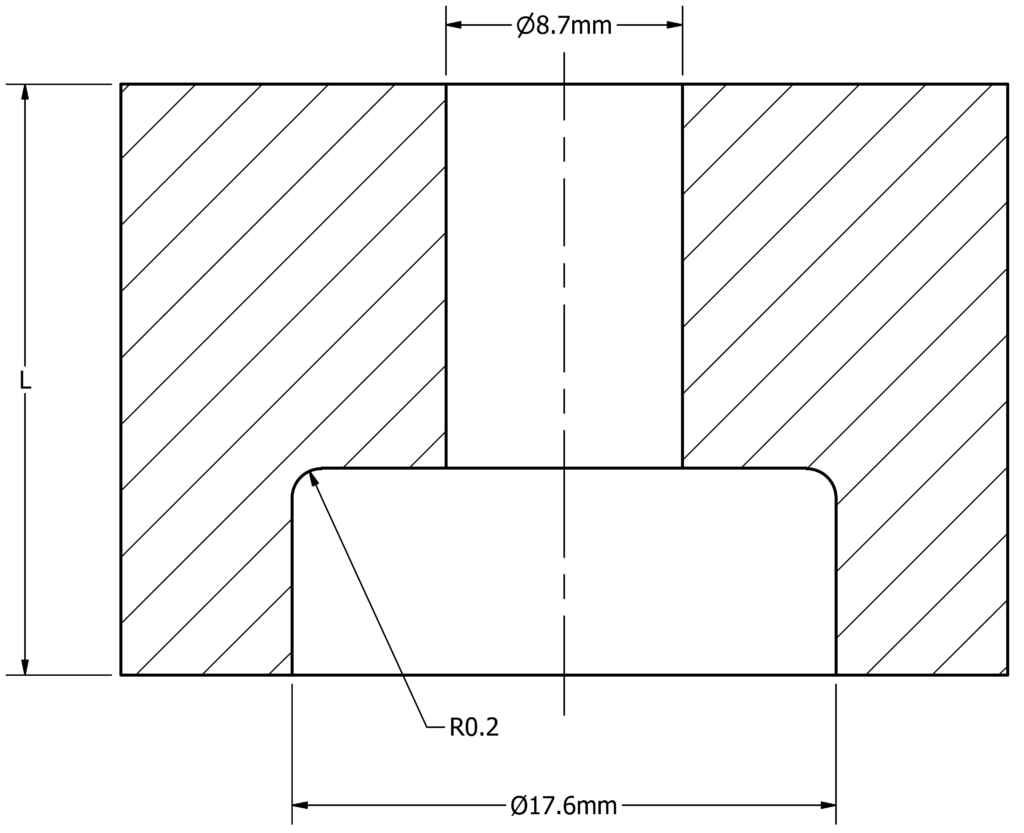
Example: Ød = 8.7 mm → Series B / UX2080 familyDefine the Back Feature
Enter the required spotface / counterbore ØD, pilot-hole length L and corner radius R.
Check L ≤ RFCSelect Cutting Geometry
Choose the chip-former and coating / surface treatment for the workpiece material. Use the Insert Technology guide below or the configurator recommendation.
PL / ML / HL + coatingVerify Series & Designation
Confirm the insert series matches the UX holder and use the generated US designation for quotation / ordering.
US-d087-D176-B-R02-ML-NCTChip-Formers, Coatings & Surface Treatments
The chip-former controls the cutting-edge geometry; the coating or surface treatment controls heat resistance, wear behavior, friction and material adhesion. Use this section to understand the codes used by the USPOT configurator and insert designation.
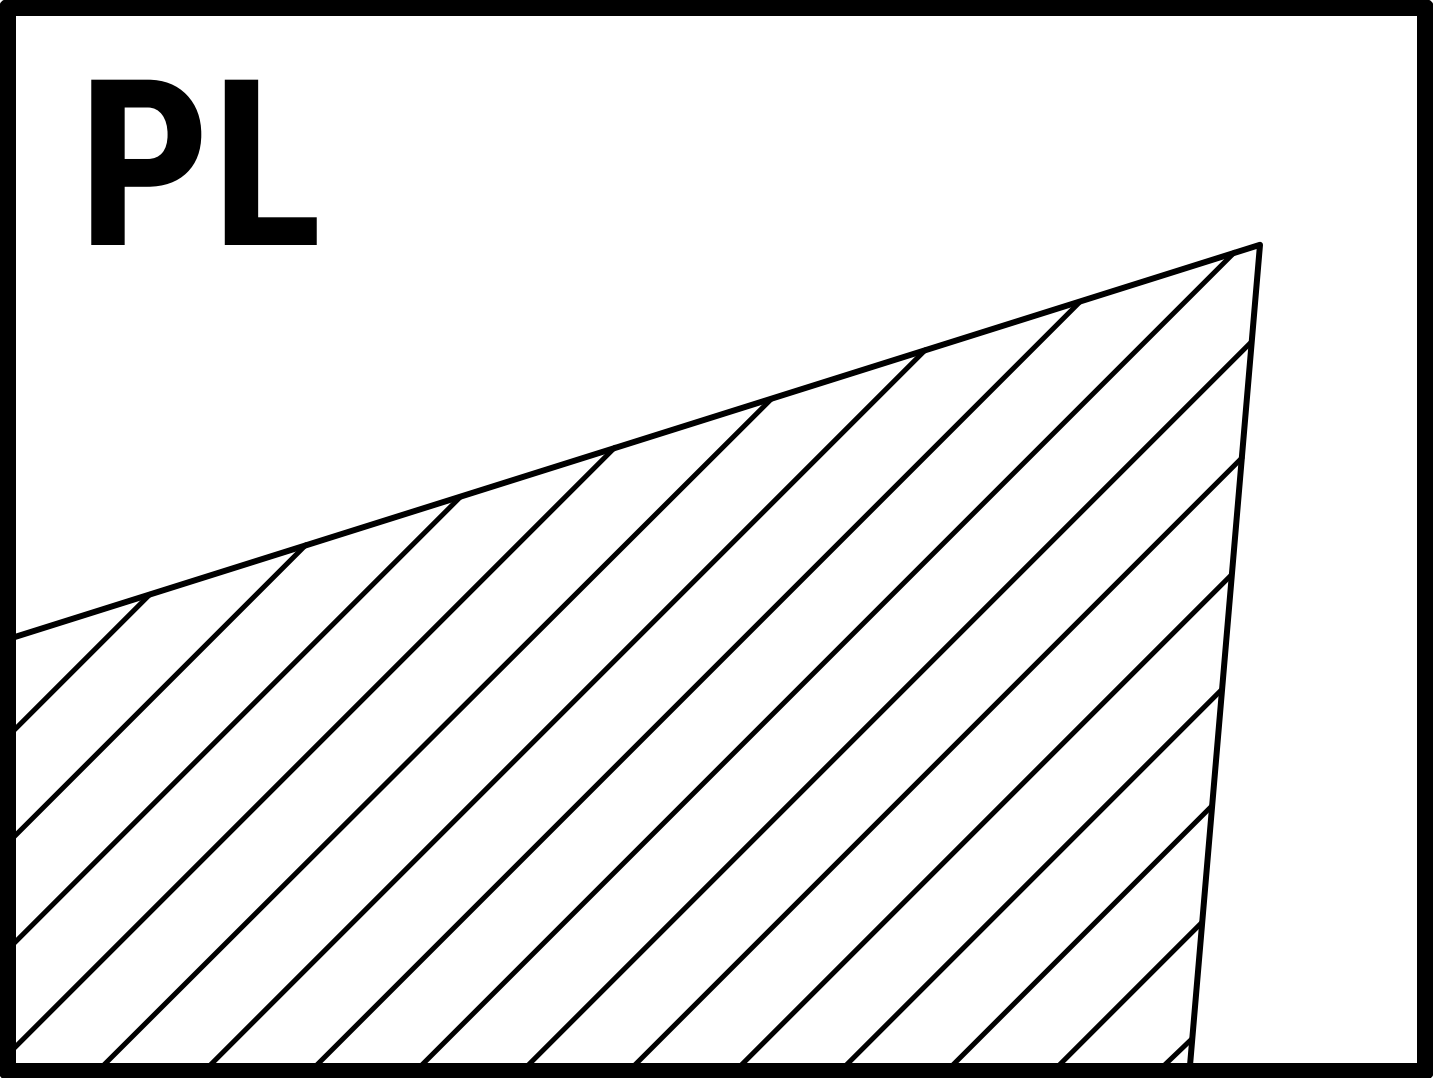
PL — Positive Cutting Land
Suitable for all-round purpose and ISO P, M, K, N and S materials, as well as composite materials.
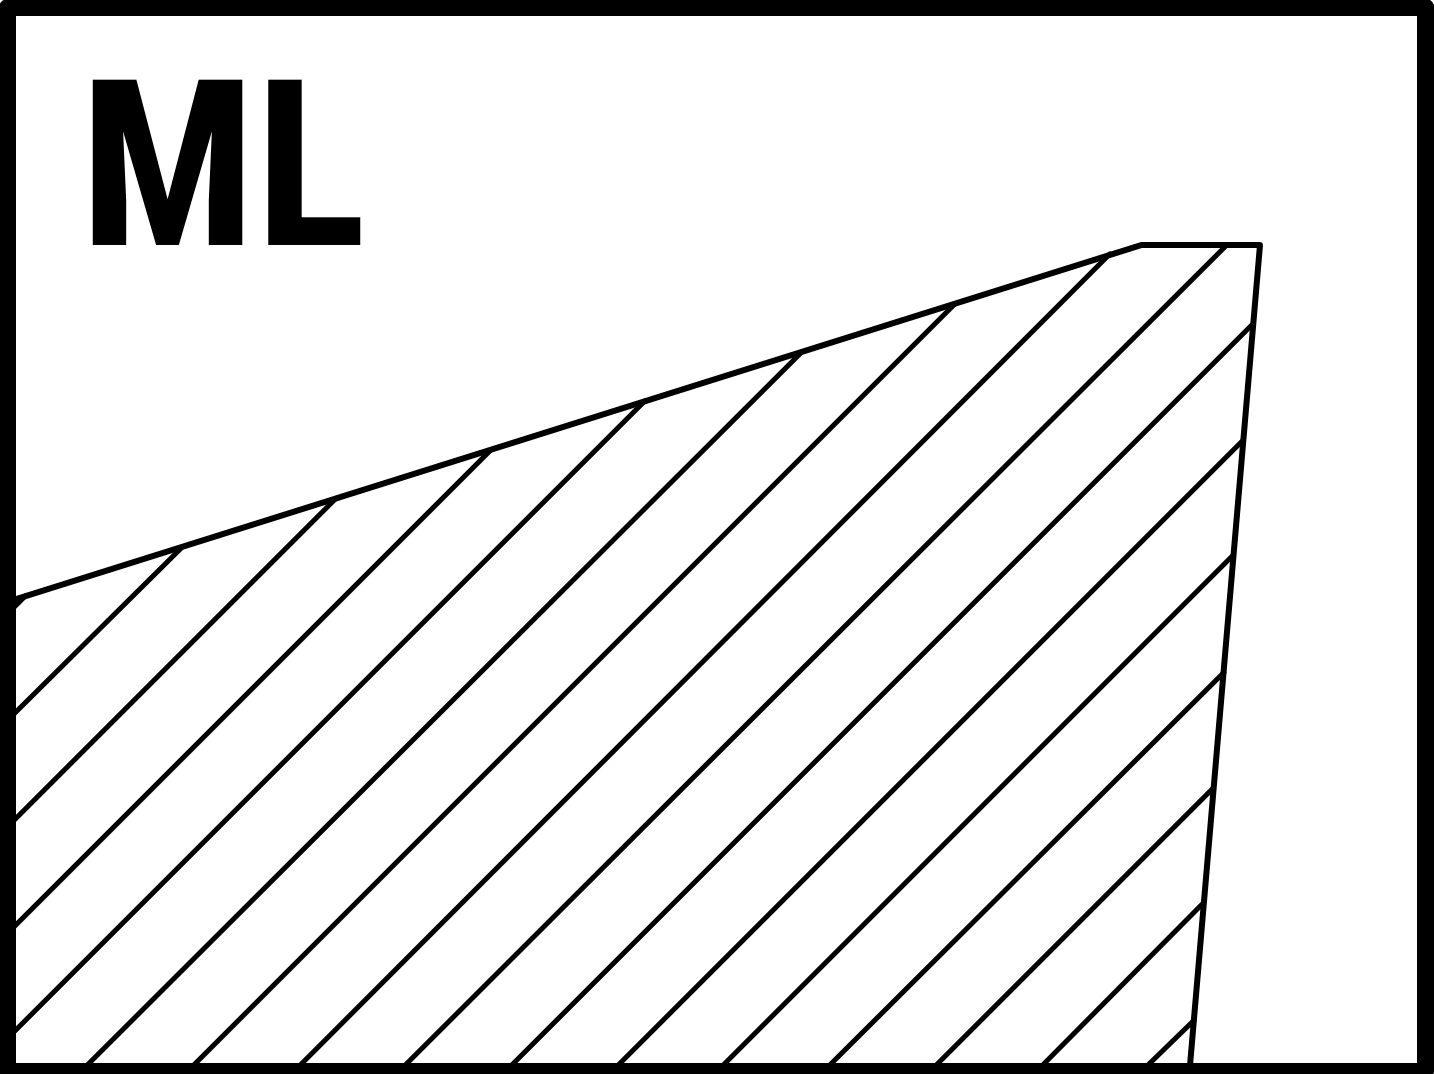
ML — Moderate Cutting Land
Suitable for ISO P, M, K, S and H materials.
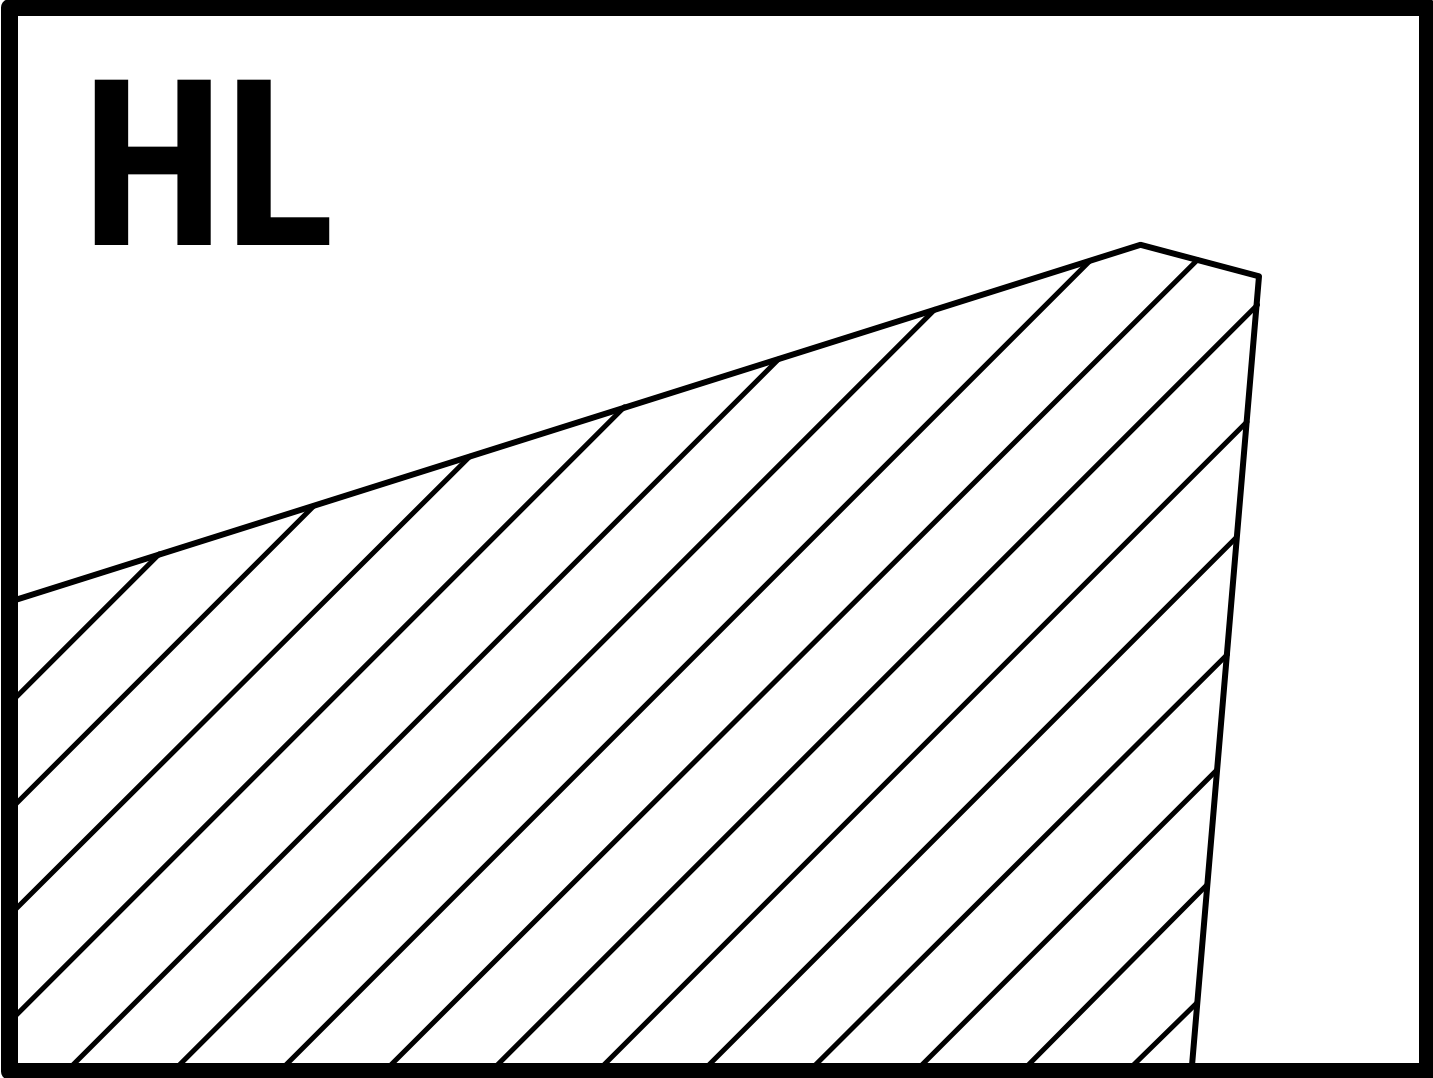
HL — Negative Cutting Land
Suitable for ISO P, M, K, S and H materials.
Coating Types & Surface Treatments
Comparison of NOGA coating / surface-treatment codes, key characteristics, typical applications and ISO material-group suitability.
| NOGA's Code | Coating | Key Features | Applications | Industries | Material Examples | ISO GROUP | |||||
|---|---|---|---|---|---|---|---|---|---|---|---|
| P | M | K | N | S | H | ||||||
| NCT | TiAlN | Excellent thermal stability, oxidation resistance, and wear resistance. | High-speed cutting and general-purpose machining. Works in wet & dry conditions. | Aerospace, Automotive, General Engineering | AISI 304, 42CrMo4, Grey Cast Iron (GG), Ti6Al4V | ✓ | ✓ | ✓ | × | ✓ | ✓ |
| NCD | TiAlSiN | Very high hardness, extreme oxidation resistance (>1200°C). Excels in dry machining at high speeds. Suitable for hardened steels >45 Rc. | High-performance machining in demanding environments. | Aerospace, Automotive, Die & Mold | Inconel 718, AISI 4140, Ti6Al4V, Hastelloy | ✓ | ✓ | × | × | ✓ | ✓ |
| NCA | AlTiSiN | High hardness, thermal stability, and wear resistance. Works well in dry, high-speed cutting. Suitable for hardened steels >45 Rc. | High-speed machining in extreme conditions. | Aerospace, Automotive, Precision Engineering | AISI 316, AISI H13, Hastelloy | ✓ | ✓ | × | × | ✓ | ✓ |
| NCN | AlCrN | High oxidation resistance (to 1100°C), toughness, abrasion resistance. | General machining in abrasive / wet conditions. | Automotive, Aerospace, Die & Mold | AISI 304, AISI 1045, Grey Cast Iron (GG), AL6061, Die Steels | ✓ | ✓ | ✓ | ✓ | × | × |
| NCW | AlTiN | High hardness, wear resistance, thermal stability up to 1100°C. | Heavy-duty machining and high-speed cutting. Dry & abrasive conditions. | Aerospace, Automotive, Heavy Engineering | AISI 4340, M2 HSS, Grey Cast Iron (GG) | ✓ | ✓ | ✓ | × | ✓ | × |
| NCB | TiB₂ | Excellent thermal stability, hardness, and very high conductivity. Prevents material adhesion and BUE. | High-speed machining of non-ferrous metals. | Aerospace, Automotive, Electronics | AL7075, 6061-T6, Copper, Magnesium Alloys (AZ31), SiC composites | × | × | × | ✓ | ✓ | × |
| POL | Polishing (Surface Treatment) | Removes scratches, burrs and micro-defects. Produces smooth finish and reduces friction. | High-speed finishing of non-ferrous materials. Improves MRR and surface aesthetics. | Aerospace, Automotive | AL7075, 6061-T6, Copper, Magnesium Alloys (AZ31) | × | × | × | ✓ | × | × |
USPOT Configurator & G-Code Generator
Enter the feature once: it checks the pilot range, ØD and L ≤ RFC, matches the UX holder, and outputs the USPOT designation and CNC program.
🔧 UBACK Configurator & G-Code Generator
USPOT / UCHAMF insert configurator · Tool-holder matching · CNC back counterboring & countersinking programs
Step 1: Select Insert Type
Choose the UBACK application you need. The configurator will build the exact insert designation and match the correct UX tool-holder.
Click an insert type to continue — the configurator opens automatically.
Step 2: Insert Configurator
Enter your application dimensions. All designation codes are generated in metric.
⚡ Quick Fill from Insert Designation (optional)
⚙ Configuration Parameters
📐 Technical Diagram
Step 3: Your Insert & Tool-Holder
Matched configuration based on your application. The insert series always matches the tool-holder series.
🔩 Insert
🛠 UX Tool-Holder
Step 4: Generate CNC Program
Build the back-machining cycle for your controller using the matched tool-holder and insert.
📊 Recommended Cutting Data
Generated G-Code Program
Disclaimer of Liability — CNC Programs
The CNC programs, cutting data, and 3D models generated by this tool are provided for reference and convenience only, as a starting point for process planning. They are generated automatically from the parameters entered and have not been verified for any specific machine, control, workpiece, fixture, or operating condition.
It is the sole responsibility of a qualified CNC programmer or operator to review, validate, and adapt every generated program before use — including verifying all coordinates, speeds, feeds, tool and coolant M-codes, clearances, and safety limits against the actual machine and setup. Every program must be run for the first time with appropriate caution, using reduced feed and rapid overrides, single-block execution, and a dry run without a workpiece.
To the fullest extent permitted by law, NOGA and its affiliates accept no responsibility or liability for any damage, injury, loss, or cost of any kind arising from the use of, or reliance on, the output of this tool, whether used as generated or after modification. Use of this tool constitutes acceptance of these terms.
Download 3D model
Choose what the STEP file should contain. Both options use the same datum: tool axis on Z, Z0 at the tool nose face.
Full USPOT Tool-Holder Reference
Use the configurator for selection; use this Metric / Inch table for dimensional verification, spare parts and setup references. LTB1 depends on the USPOT insert size and the listed value is the maximum permitted value.
USPOT / UX Dimensional Drawing
Reference drawing for the USPOT insert mounted in the UBACK UX tool-holder. Use it together with the table dimensions below.
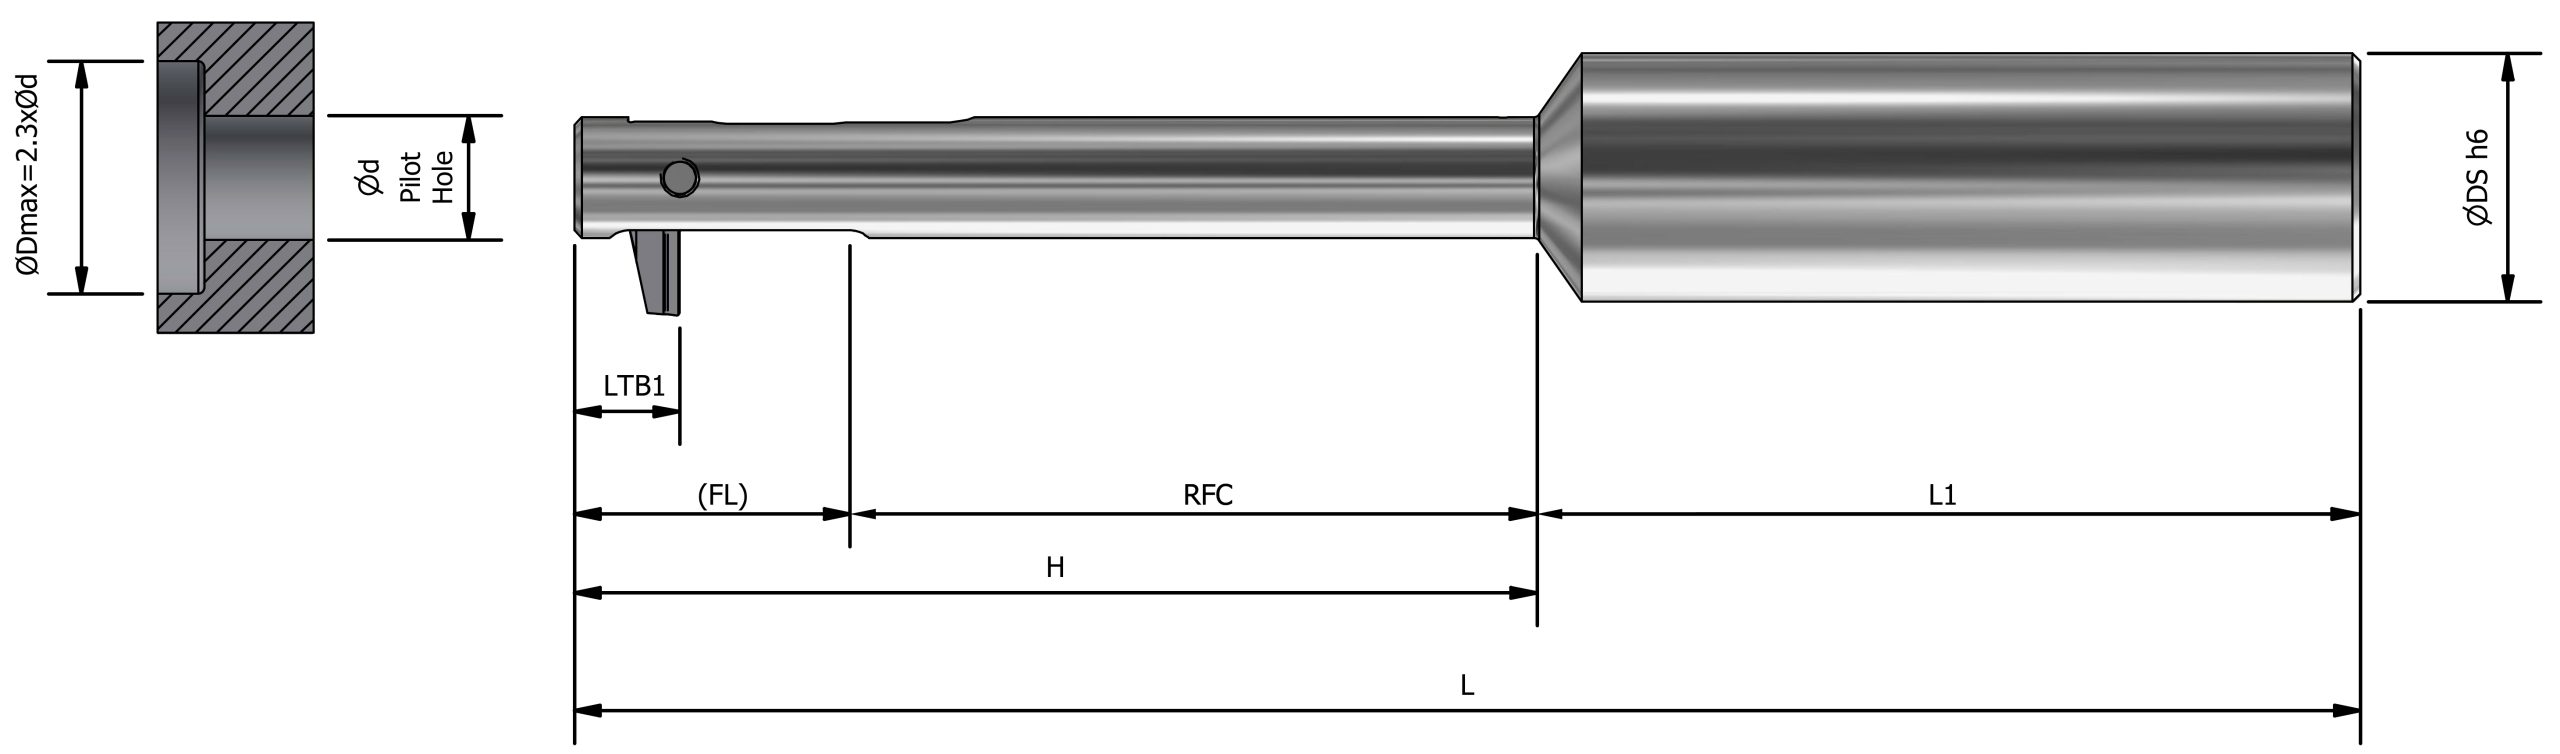
Show / hide complete Metric / Inch holder table
| Ød minmm / inch | SKU | Description | Series | ØDS h6mm / inch | FLmm / inch | RFCmm / inch | Hmm / inch | Lmm / inch | L1mm / inch | LTB1 maxmm / inch | USPOT ØDmaxmm / inch | Piston Plug | Insert Screw |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Ø8 mmØ0.315″ | UX2080 | UX-d080-B-C16-H62-L115 | B | Ø16 mmØ0.630″ | 17 mm0.669″ | 43 mm1.693″ | 62 mm2.441″ | 115 mm4.528″ | 53 mm2.087″ | 7.3 mm0.287″ | Ø18.5 mmØ0.728″ | UX0011 / M5×6 | UX0005 / M2.5×0.35×7B |
| Ø9 mmØ0.354″ | UX2090 | UX-d090-B-C16-H62-L115 | B | Ø16 mmØ0.630″ | 17.8 mm0.701″ | 43 mm1.693″ | 62 mm2.441″ | 115 mm4.528″ | 53 mm2.087″ | 7.3 mm0.287″ | Ø21 mmØ0.827″ | UX0011 / M5×6 | UX0005 / M2.5×0.35×7B |
| Ø10 mmØ0.394″ | UX2100 | UX-d100-B-C16-H62-L115 | B | Ø16 mmØ0.630″ | 18.8 mm0.740″ | 43 mm1.693″ | 62 mm2.441″ | 115 mm4.528″ | 53 mm2.087″ | 7.3 mm0.287″ | Ø23 mmØ0.906″ | UX0011 / M5×6 | UX0005 / M2.5×0.35×7B |
| Ø11 mmØ0.433″ | UX3110 | UX-d110-C-C16-H80-L133 | C | Ø16 mmØ0.630″ | 27 mm1.063″ | 52 mm2.047″ | 80 mm3.150″ | 133 mm5.236″ | 53 mm2.087″ | 12.4 mm0.488″ | Ø26 mmØ1.024″ | UX0011 / M5×6 | UX0006 / M3×0.35×10C |
| Ø12 mmØ0.472″ | UX3120 | UX-d120-C-C16-H80-L133 | C | Ø16 mmØ0.630″ | 27.3 mm1.075″ | 52 mm2.047″ | 80 mm3.150″ | 133 mm5.236″ | 53 mm2.087″ | 12.4 mm0.488″ | Ø28 mmØ1.102″ | UX0011 / M5×6 | UX0006 / M3×0.35×10C |
| Ø13 mmØ0.512″ | UX3130 | UX-d130-C-C16-H80-L133 | C | Ø16 mmØ0.630″ | 28 mm1.102″ | 52 mm2.047″ | 80 mm3.150″ | 133 mm5.236″ | 53 mm2.087″ | 12.4 mm0.488″ | Ø30 mmØ1.181″ | UX0011 / M5×6 | UX0006 / M3×0.35×10C |
| Ø14 mmØ0.551″ | UX4140 | UX-d140-D-C20-H105-L158 | D | Ø20 mmØ0.787″ | 32.5 mm1.280″ | 72.5 mm2.854″ | 105 mm4.134″ | 158 mm6.220″ | 53 mm2.087″ | 14 mm0.551″ | Ø32.5 mmØ1.280″ | UX0012 / M6×6 | UX0007 / M3×0.35×13D |
| Ø15 mmØ0.591″ | UX4150 | UX-d150-D-C20-H105-L158 | D | Ø20 mmØ0.787″ | 32.5 mm1.280″ | 72.5 mm2.854″ | 105 mm4.134″ | 158 mm6.220″ | 53 mm2.087″ | 14 mm0.551″ | Ø34.5 mmØ1.358″ | UX0012 / M6×6 | UX0007 / M3×0.35×13D |
| Ø16 mmØ0.630″ | UX4160 | UX-d160-D-C20-H105-L158 | D | Ø20 mmØ0.787″ | 32.5 mm1.280″ | 72.5 mm2.854″ | 105 mm4.134″ | 158 mm6.220″ | 53 mm2.087″ | 14 mm0.551″ | Ø37 mmØ1.457″ | UX0012 / M6×6 | UX0007 / M3×0.35×13D |
| Ø17 mmØ0.669″ | UX5170 | UX-d170-E-C20-H115-L170 | E | Ø20 mmØ0.787″ | 38.5 mm1.516″ | 76.5 mm3.012″ | 115 mm4.528″ | 170 mm6.693″ | 55 mm2.165″ | 16.5 mm0.650″ | Ø39.5 mmØ1.555″ | UX0012 / M6×6 | UX0008 / M3×0.35×16E |
| Ø18 mmØ0.709″ | UX5180 | UX-d180-E-C20-H115-L170 | E | Ø20 mmØ0.787″ | 38.5 mm1.516″ | 76.5 mm3.012″ | 115 mm4.528″ | 170 mm6.693″ | 55 mm2.165″ | 16.5 mm0.650″ | Ø41.5 mmØ1.634″ | UX0012 / M6×6 | UX0008 / M3×0.35×16E |
| Ø19 mmØ0.748″ | UX5190 | UX-d190-E-C20-H115-L170 | E | Ø20 mmØ0.787″ | 38.5 mm1.516″ | 76.5 mm3.012″ | 115 mm4.528″ | 170 mm6.693″ | 55 mm2.165″ | 16.5 mm0.650″ | Ø44 mmØ1.732″ | UX0012 / M6×6 | UX0008 / M3×0.35×16E |
| Ø20 mmØ0.787″ | UX6200 | UX-d200-F-C25-H120-L175 | F | Ø25 mmØ0.984″ | 43.5 mm1.713″ | 76.5 mm3.012″ | 120 mm4.724″ | 175 mm6.890″ | 55 mm2.165″ | 18.8 mm0.740″ | Ø46 mmØ1.811″ | UX0013 / M8×6 | UX0009 / M4×0.5×19F |
| Ø21 mmØ0.827″ | UX6210 | UX-d210-F-C25-H120-L175 | F | Ø25 mmØ0.984″ | 43.5 mm1.713″ | 76.5 mm3.012″ | 120 mm4.724″ | 175 mm6.890″ | 55 mm2.165″ | 18.8 mm0.740″ | Ø48.5 mmØ1.909″ | UX0013 / M8×6 | UX0009 / M4×0.5×19F |
| Ø22 mmØ0.866″ | UX6220 | UX-d220-F-C25-H120-L175 | F | Ø25 mmØ0.984″ | 43.5 mm1.713″ | 76.5 mm3.012″ | 120 mm4.724″ | 175 mm6.890″ | 55 mm2.165″ | 18.8 mm0.740″ | Ø50.5 mmØ1.988″ | UX0013 / M8×6 | UX0009 / M4×0.5×19F |
| Ø23 mmØ0.906″ | UX7230 | UX-d230-G-C25-H120-L175 | G | Ø25 mmØ0.984″ | 48 mm1.890″ | 72 mm2.835″ | 120 mm4.724″ | 175 mm6.890″ | 55 mm2.165″ | 21 mm0.827″ | Ø53 mmØ2.087″ | UX0013 / M8×6 | UX0010 / M4×0.5×21G |
| Ø24 mmØ0.945″ | UX7240 | UX-d240-G-C25-H120-L175 | G | Ø25 mmØ0.984″ | 48 mm1.890″ | 72 mm2.835″ | 120 mm4.724″ | 175 mm6.890″ | 55 mm2.165″ | 21 mm0.827″ | Ø55.5 mmØ2.185″ | UX0013 / M8×6 | UX0010 / M4×0.5×21G |
| Ø25 mmØ0.984″ | UX7250 | UX-d250-G-C25-H120-L175 | G | Ø25 mmØ0.984″ | 48 mm1.890″ | 72 mm2.835″ | 120 mm4.724″ | 175 mm6.890″ | 55 mm2.165″ | 21 mm0.827″ | Ø57.5 mmØ2.264″ | UX0013 / M8×6 | UX0010 / M4×0.5×21G |
USPOT at a glance
Screening values. The configurator confirms the exact holder and insert.
- Pilot-Hole Range
- Ø8–25 mm / 0.315–0.984″
- Counterbore / Spotface ØD Range
- Ø8.5–57.5 mm / 0.335–2.264″
- Pressure Actuation
- Internal coolant, emulsion or air
- Minimum Pressure
- 6 bar / 90 PSI
- ØD Counterbore / Spotface Tolerance
- ±0.1 mm / ±0.004″
- Tool-Holder Family
- UBACK UX / DURASHIELD
Selection and technical links
Start with the Application — Not the Catalog Table
Start with the application and configurator, then use the technical facts, range, holder data and coding references for verification.
Enter pilot diameter, ØD, pilot-hole length, radius and material. Match the UX holder and generate the insert designation.
Open configurator Check the RangeSee the B–G series, pilot-hole ranges, holder maximum ØD values and RFC capacity before configuring.
View range Selection LogicFollow the four checks that determine holder, insert geometry and compatibility.
How to select Technical CenterProgramming, insert replacement, cooling configurations, cutting data, chip-formers and coatings.
Open technical infoApplication examples
Typical rear faces USPOT reaches through the pilot hole, continuous and interrupted.
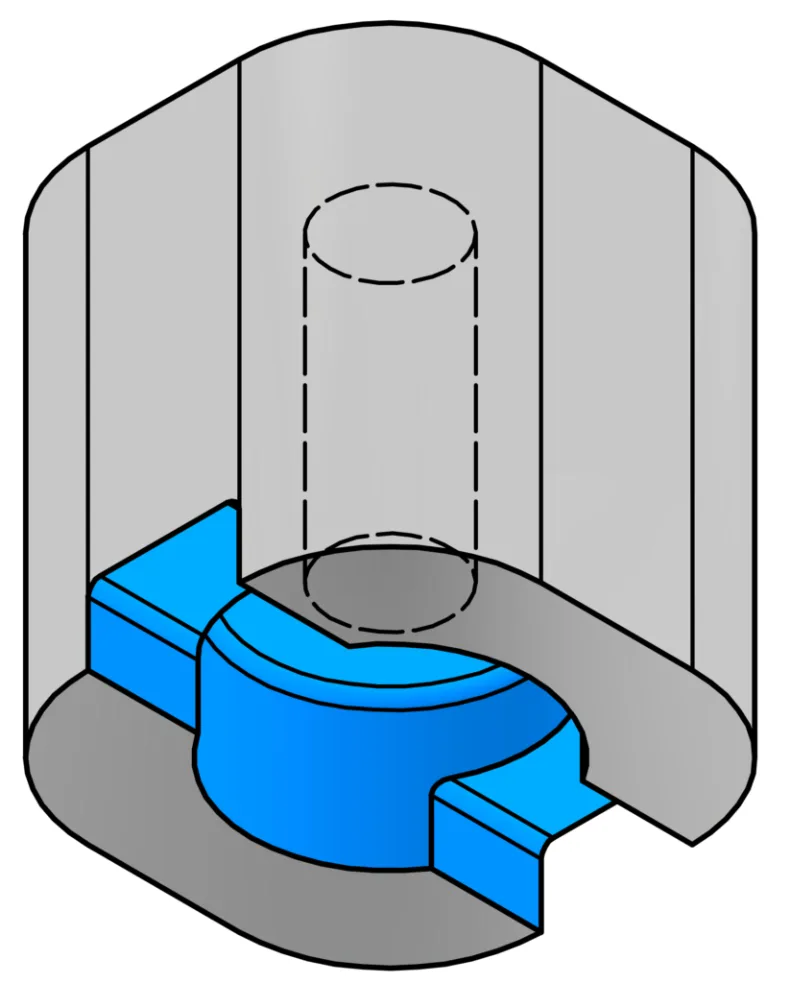
Internal Rear-Face Access
Reach a hidden rear surface through the pilot hole without turning or repositioning the workpiece.
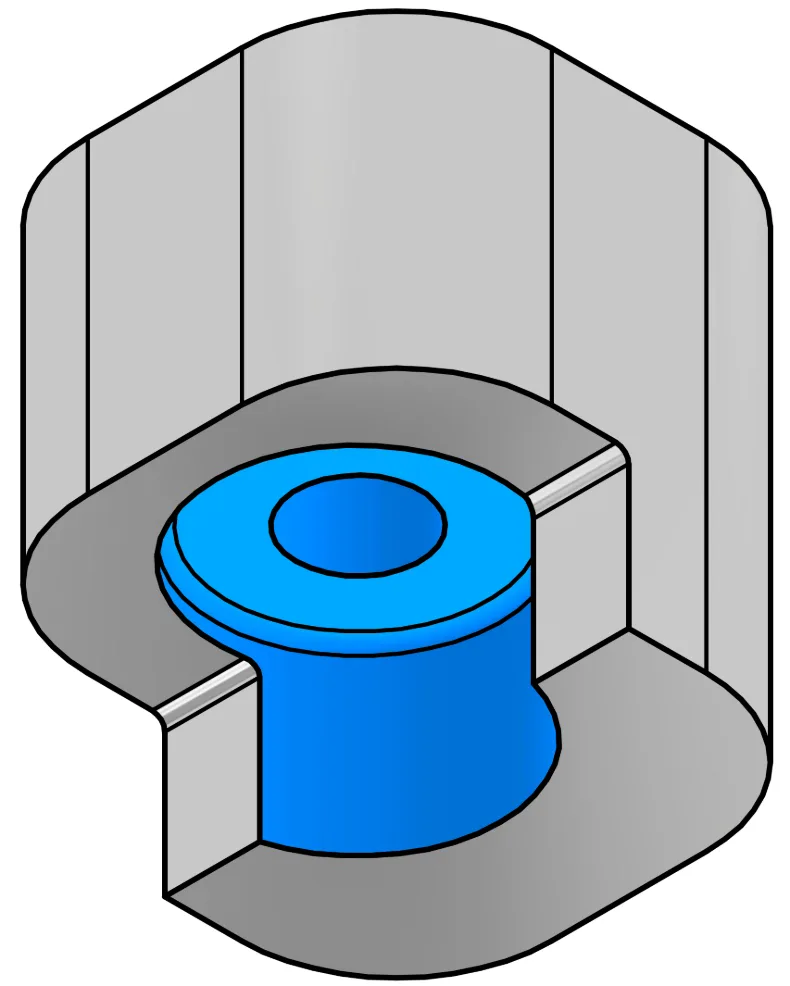
Restricted-Access Geometry
Use the foldable insert where conventional front-side tooling cannot physically reach the machining surface.
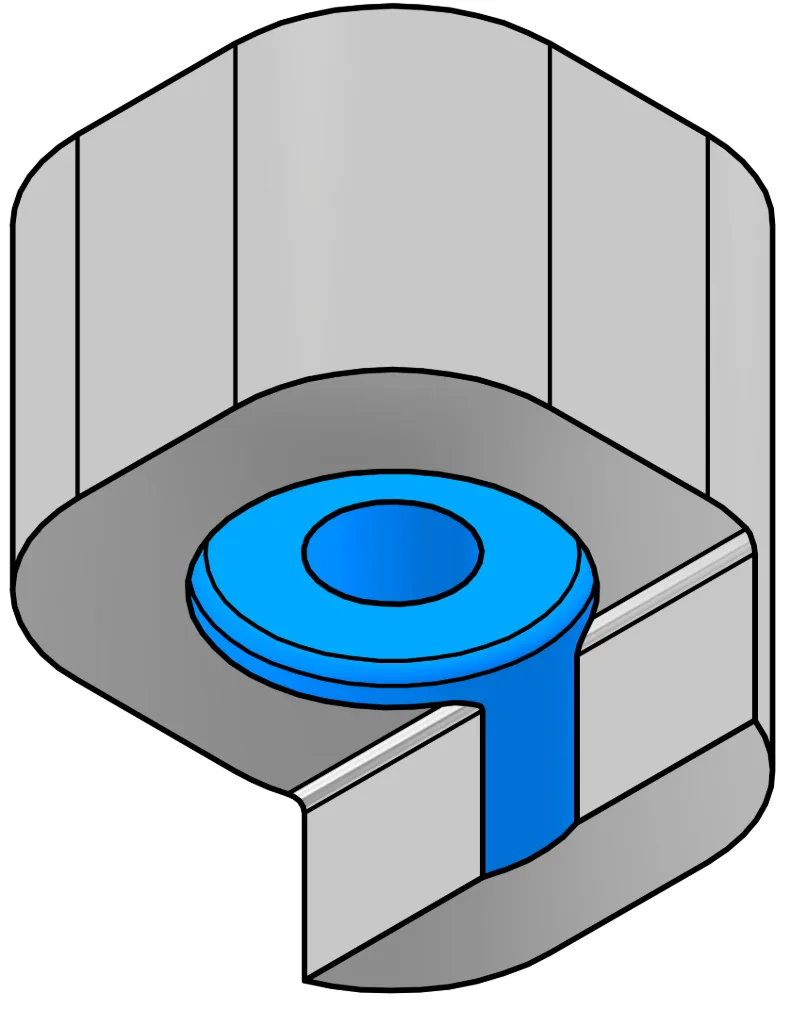
Deep / Recessed Back Surface
Match pilot-hole length to holder RFC and reach the required rear-side machining plane inside deeper components.
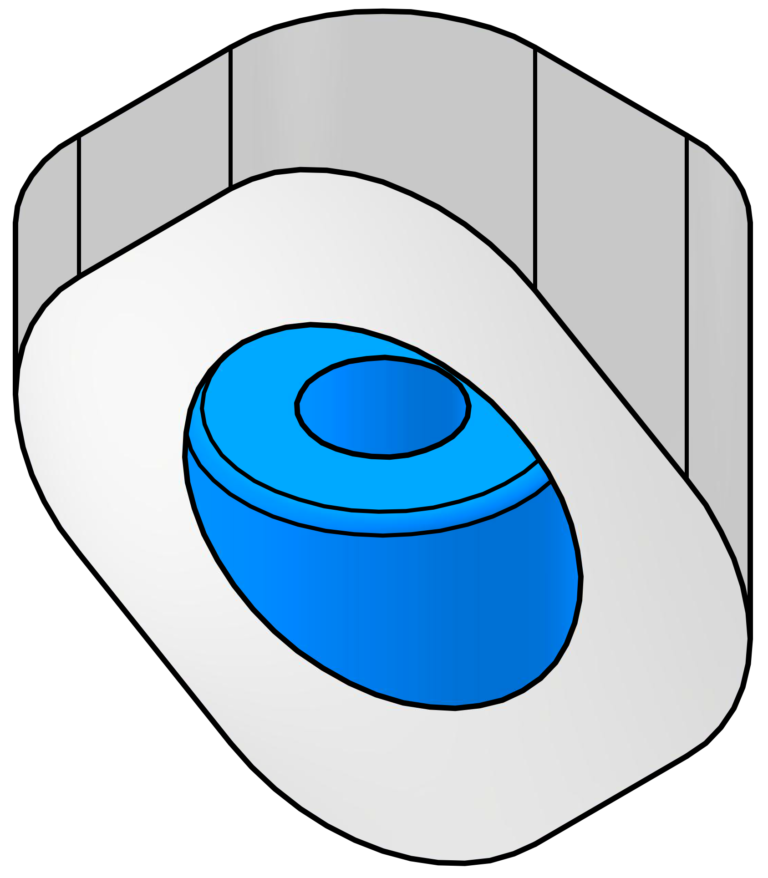
Complex Internal Access
Apply rear spotfacing or counterboring where part geometry makes a conventional straight tool approach impractical.
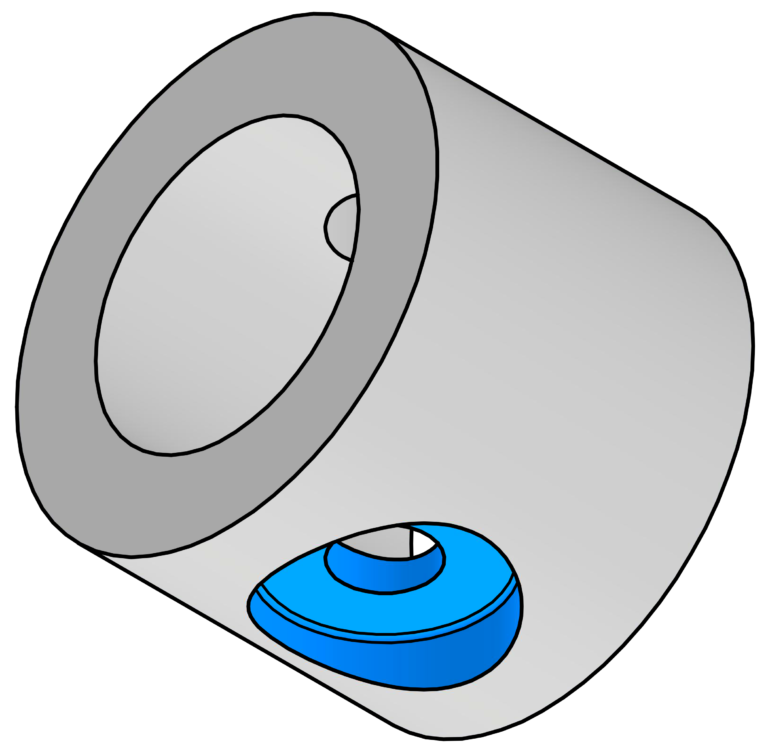
Interrupted Rear Surfaces
USPOT can be applied to selected interrupted rear surfaces when rigidity, insert engagement and cutting conditions are suitable.
How the UBACK mechanism works
Coolant, emulsion or air through the spindle (6 bar / 90 PSI minimum) opens the insert below the part and lets it fold back for a safe exit.
 Plays muted when in view
Enter with the Insert Folded
Position above the pilot hole and move through the bore with the insert retracted to protect the pilot-hole surface.
Move Below the Workpiece
Use the holder FL / RFC geometry to reach a safe position below the rear face before the cutting move.
Actuate & Machine
Internal coolant pressure actuates the insert. Approach the rear face and machine the required spotface / counterbore depth.
Close & Retract
Retract to the safe position, turn coolant pressure off as required by the cycle, fold the insert and exit through the pilot hole.
Understand the Holder and USPOT Insert Codes
The configurator creates the designation automatically. These diagrams remain useful as a visual reference for purchasing, engineering drawings and quotations.

UX Tool-Holder Coding
Holder designation communicates pilot diameter, series, shank size, working height and overall length.
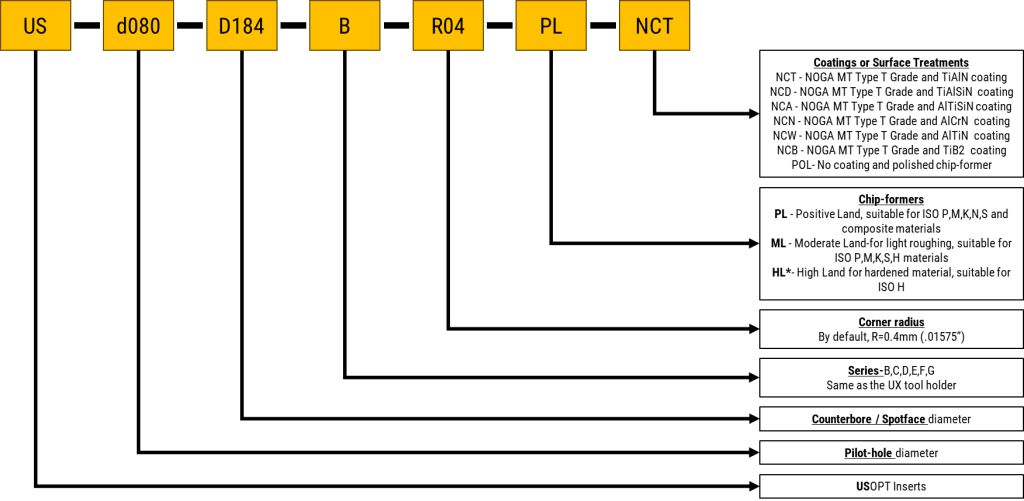
USPOT Insert Coding
Insert designation identifies pilot diameter, counterbore diameter, series, radius, chip-former and coating.
AISI 4340 · 42 HRC
Watch USPOT & UBACK in Action
Inline previews let visitors understand the machining concept without leaving the product page. The USPOT product demonstration is lazy-loaded so it does not delay the initial page render. The UBACK mechanism video is shown in the Operating Principle section above.
 AUTO-PLAYS WHEN VISIBLE
USPOT by NOGA MT | High-Accuracy Spot Facing with Hydraulic Control
Product demonstration focused on USPOT hydraulic operation and precision rear-side spotfacing.

DURASHIELD Tool-Holders
DURASHIELD identifies NOGA MT's premium holder platform. The UX holder family uses a passivated construction designed for corrosion resistance, structural integrity and demanding industrial service.
USPOT Selection Questions
Can USPOT machine a back counterbore without turning or flipping the workpiece?
Yes. USPOT reaches the hidden rear face through the existing pilot hole, allowing CNC back spotfacing or counterboring without turning or flipping the workpiece.
How do I select the correct USPOT insert diameter?
Start with the pilot-hole diameter and select the matching UX holder series. Then enter the required spotface diameter ØD, pilot-hole length L and corner radius R in the configurator. The required L must satisfy L ≤ RFC, ØD must remain within the selected holder / insert limit, and the insert series must match the UX holder series.
What is the maximum back spotface diameter for USPOT?
The maximum depends on the selected UX holder and series. Across the standard USPOT / UBACK range, spotface diameters extend up to Ø57.5 mm / 2.264″. Use the configurator or the Size Range table to verify the exact ØD limit for your pilot-hole diameter and holder.
What is USPOT used for?
USPOT is the UBACK flat-bottom insert solution for CNC back spotfacing and back counterboring through an existing pilot hole.
How is the insert opened and closed?
The UX tool-holder uses spindle coolant pressure to actuate the insert. The system supports coolant, emulsion or air with a minimum pressure of 6 bar / 90 PSI.
What is the most important geometry check?
Confirm that the pilot-hole length L is less than or equal to the selected holder RFC and that the requested ØD is within the holder / insert design limit.
Are USPOT inserts standard products?
USPOT is a semi-standard solution customized to the customer's specific feature. The configurator creates the application-specific designation and matches the corresponding UBACK UX holder series.
What is the ØD counterbore / spotface tolerance?
The product page specifies an achieved counterbore / spotface diameter tolerance of ±0.1 mm / 0.004″.
Where are programming and cutting recommendations?
Use the UBACK Technical Center ↗ for continuous / interrupted-cut programming, insert replacement, cooling configurations, coatings, chip-formers and detailed cutting recommendations.
Can USPOT perform interrupted cuts?
Yes. USPOT can perform interrupted back spotfacing and counterboring when the cutting path crosses gaps, openings, slots or other non-continuous rear surfaces. Final performance depends on the actual geometry, material, setup rigidity and cutting conditions, so the application should be validated before production.
Have the Drawing? Configure USPOT First.
Enter the application dimensions in the configurator to identify the correct UX tool-holder and build the USPOT designation. For special applications, attach the workpiece drawing and material details when requesting a quotation.